

Introduction to Equipment and Structural Principles of Powdered Mineral Pneumatic Conveying Systems
HeadPowder, a prominent name in the field of pneumatic conveying technology, specializes in providing advanced equipment for the efficient handling and transportation of powdered minerals. With a strong foundation in engineering excellence and a commitment to innovation, the company has established itself as a trusted partner for industries reliant on reliable material transport solutions.
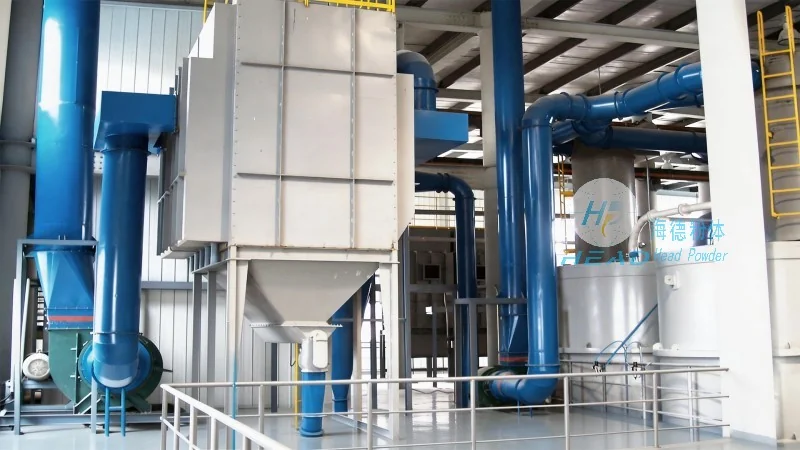
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company leverages decades of experience in the engineering and manufacturing of pneumatic conveying systems to deliver high-performance solutions tailored to the unique needs of various industrial applications. By combining robust design with cutting-edge technology, HeadPowder ensures that its equipment meets the stringent requirements of modern material handling processes.
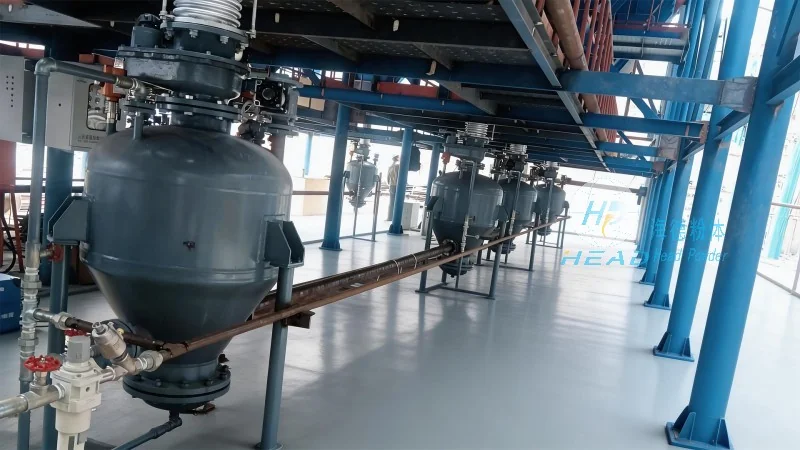
Pneumatic Conveying System Equipment Overview
The core of HeadPowder's offerings lies in its comprehensive range of pneumatic conveying system equipment. These systems are engineered to handle a wide variety of powdered minerals, including but not limited to coal, cement, flour, and other fine particulate materials. The equipment is designed to optimize material transport efficiency while minimizing operational costs and maintenance requirements. Key components typically include feeders, conveyors, and control systems, all integrated to form a seamless material handling solution.
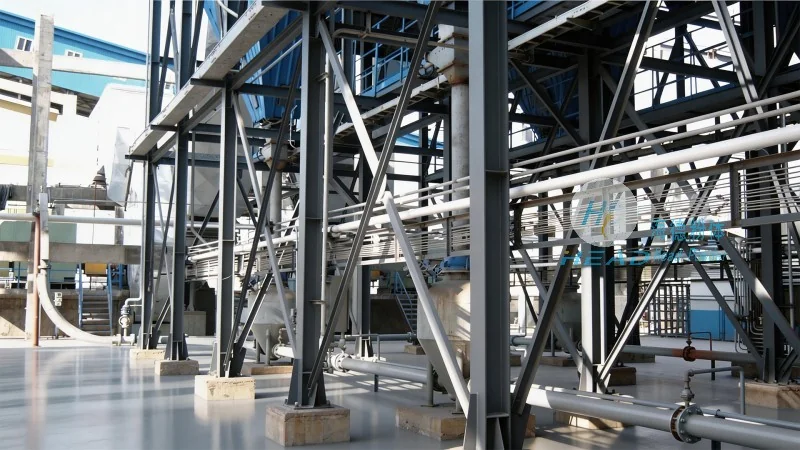
Structural Principles of Pneumatic Conveying Systems
The structural principles underlying HeadPowder's pneumatic conveying systems are centered on the use of air as the primary medium for transporting materials. The system operates by creating a pressure differential between the inlet and outlet of the conveying line, which draws the powdered material into the system. The design incorporates features such as positive displacement blowers or rotary lobe pumps to generate the necessary air pressure, ensuring consistent and reliable material flow. Additionally, the system's structure includes features like surge hoppers and dust collectors to enhance operational stability and safety, preventing material buildup and minimizing environmental impact.
Key Features and Advantages
HeadPowder's pneumatic conveying systems are distinguished by several key features that set them apart in the industry. These include high conveying capacity, which allows for the efficient transport of large volumes of material over long distances. The systems also offer flexibility in terms of layout and integration, enabling seamless incorporation into existing production lines. Furthermore, the equipment is designed for low maintenance, with durable components that resist wear and corrosion, thereby reducing downtime and operational expenses. The use of advanced control systems ensures precise regulation of material flow, enhancing process control and product quality.
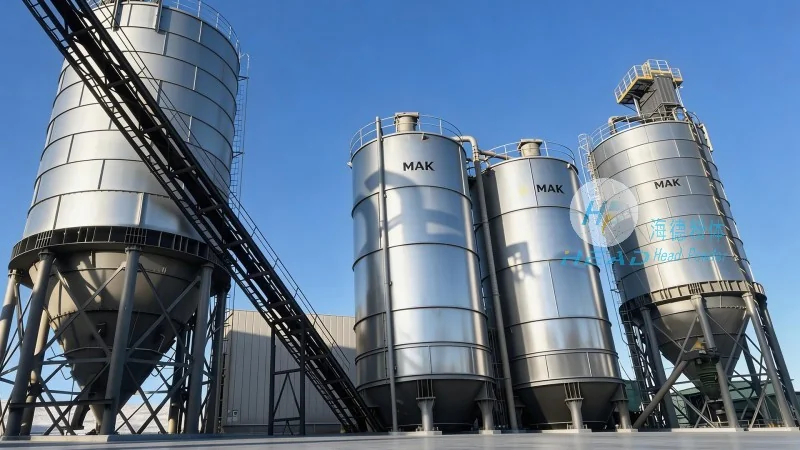
Application and Industry Impact
The applications of HeadPowder's pneumatic conveying systems span multiple industries, including mining, cement, food processing, and chemical manufacturing. In the mining sector, the systems are used to transport ore and other minerals from processing plants to storage facilities. In the cement industry, they facilitate the transport of raw materials and finished products, improving overall production efficiency. The food processing industry benefits from the hygienic design of the equipment, which ensures compliance with food safety regulations. By providing reliable and efficient material transport solutions, HeadPowder's systems contribute to increased productivity and reduced operational costs for its clients.