

Working Principle and Features of Ammonium Nitrate Material Pneumatic Conveying Line
Ammonium nitrate is a widely used chemical compound in various industrial applications, including agriculture, explosives, and chemical manufacturing. The efficient and safe transportation of this material is crucial for industrial operations. Pneumatic conveying systems have emerged as a reliable solution for handling ammonium nitrate, offering advantages over traditional methods like belt conveyors or bucket elevators. This article explores the working principle and key features of an ammonium nitrate material pneumatic conveying line, highlighting its benefits and operational aspects.
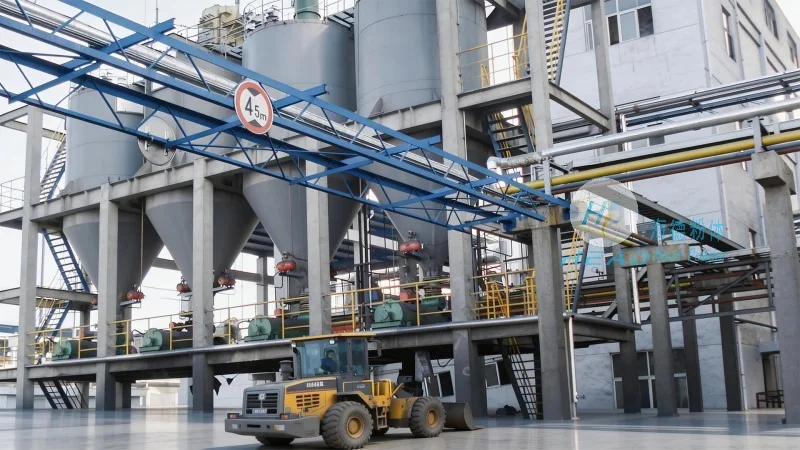
Working Principle of Ammonium Nitrate Pneumatic Conveying Line
The core of an ammonium nitrate pneumatic conveying system is the ability to transport bulk materials through a pipeline using a combination of air and pressure. The process typically involves several key components and steps. First, the ammonium nitrate material is fed into a hopper or feeder, where it is then introduced into the conveying line. A blower or compressor generates the necessary air pressure, which propels the material through the pipeline. The material is carried by the air stream, moving from the inlet to the outlet of the system. The design of the conveying line, including the type of air flow (positive or negative pressure) and the configuration of the pipeline, plays a critical role in ensuring efficient material transport. Positive pressure systems use compressed air to push the material forward, while negative pressure systems use suction to draw the material through the line. For ammonium nitrate, a positive pressure system is often preferred due to the material's properties and the need for controlled handling.
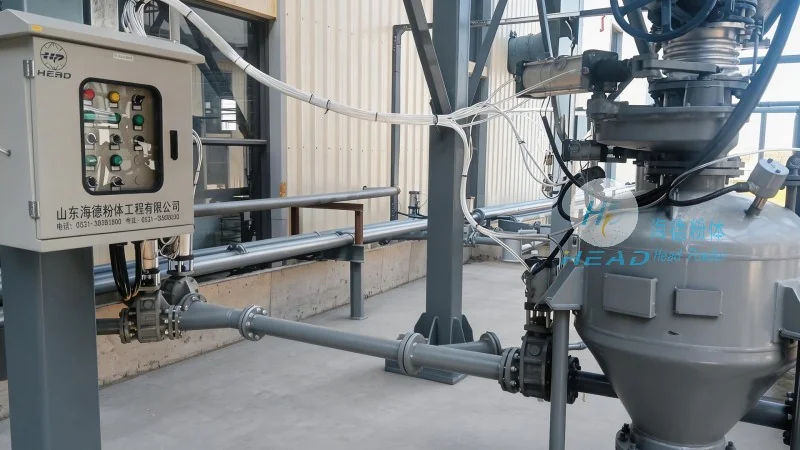
Key Features of Ammonium Nitrate Pneumatic Conveying Line
Several distinct features make the ammonium nitrate pneumatic conveying line an effective solution for material handling. First, it offers a dust-free and enclosed transport process, which is essential for handling ammonium nitrate to prevent dust dispersion and ensure safety. The system minimizes the risk of dust exposure, which is critical in industrial environments where dust can be hazardous. Second, the conveying line provides flexibility in terms of layout and installation. The pipeline can be arranged in various configurations, including vertical, horizontal, or a combination of both, to suit the specific needs of the industrial facility. This flexibility allows for integration with existing equipment and processes without major modifications. Third, the system is capable of handling a wide range of material flow rates, from low to high capacities, making it suitable for different production scales. The adjustable air pressure and flow rate controls enable precise control over the material transport, ensuring consistent performance. Fourth, the pneumatic conveying line is designed for low maintenance and durability. The components, such as the blower, pipeline, and feeder, are constructed from materials resistant to corrosion and wear, ensuring long-term operational reliability. Regular maintenance, including cleaning and inspection of the pipeline and components, is essential to maintain optimal performance.
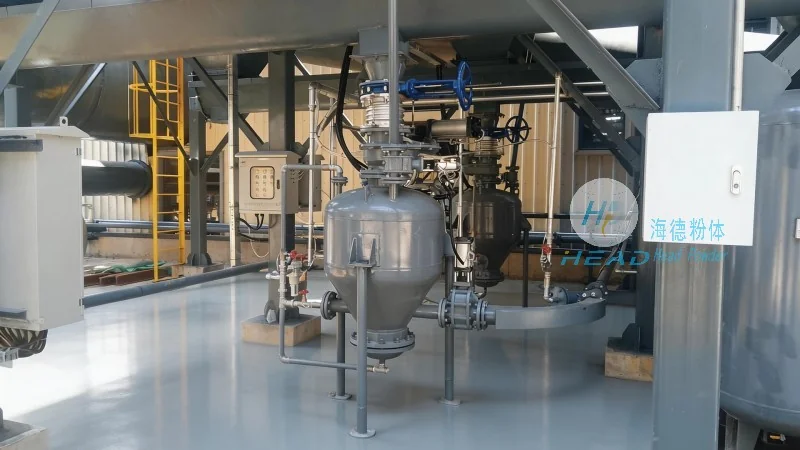
Benefits of Using Ammonium Nitrate Pneumatic Conveying Line
The adoption of an ammonium nitrate pneumatic conveying line brings numerous benefits to industrial operations. One of the primary advantages is improved safety. By enclosing the material transport process, the system reduces the risk of dust explosions and inhalation hazards associated with loose ammonium nitrate. This is particularly important in facilities where ammonium nitrate is used in large quantities. Second, the system enhances operational efficiency. The ability to transport material quickly and continuously without manual intervention reduces labor costs and increases production throughput. The consistent flow rate and minimal downtime contribute to higher overall productivity. Third, the system offers cost savings in the long run. Although the initial investment may be higher compared to traditional methods, the reduced maintenance requirements and lower material handling costs offset the initial expense over time. The enclosed design also minimizes material loss and waste, further improving cost-effectiveness. Fourth, the system provides environmental benefits. By preventing dust dispersion, the pneumatic conveying line reduces the environmental impact of material handling, complying with regulatory standards and promoting sustainable industrial practices.
Application Examples in Industrial Settings
The ammonium nitrate pneumatic conveying line is widely used in various industrial applications. In the agricultural sector, it is employed in fertilizer production facilities to transport ammonium nitrate from storage silos to processing units or packaging areas. The system ensures efficient and safe movement of the fertilizer material, supporting the production of high-quality agricultural products. In the chemical manufacturing industry, the conveying line is used in the production of explosives and other chemical compounds. The precise control over material transport is crucial for maintaining product quality and safety in these applications. Additionally, the system is utilized in the mining and mineral processing industries for handling ammonium nitrate used as a blasting agent. The ability to transport the material in a controlled manner minimizes the risk of accidents and ensures efficient blasting operations.
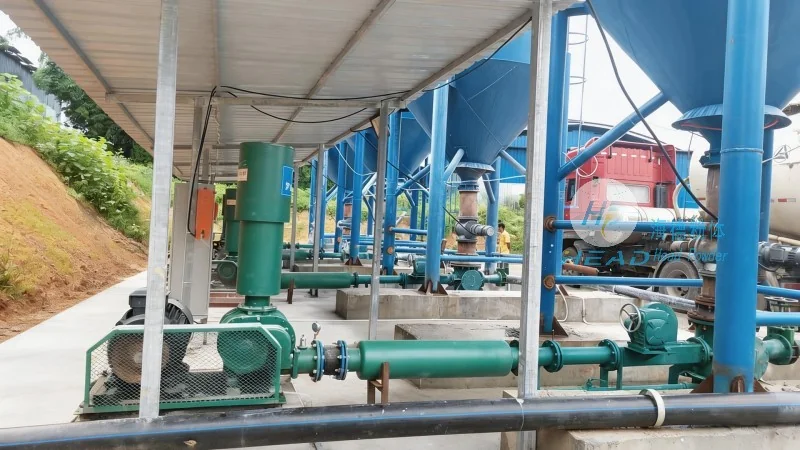
Conclusion and Company Information
Ammonium nitrate material pneumatic conveying lines are a sophisticated and efficient solution for handling this critical chemical compound. The working principle, which relies on air pressure to transport material through a pipeline, combined with key features such as dust-free operation, flexibility, and low maintenance, makes it an ideal choice for industrial applications. The benefits, including enhanced safety, operational efficiency, cost savings, and environmental compliance, further underscore the value of this technology. As industrial processes continue to evolve, the demand for reliable and safe material handling systems will remain high. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, specialize in designing and manufacturing such pneumatic conveying systems, providing tailored solutions to meet the specific needs of their clients. With a focus on quality and innovation, HeadPowder Engineering Co., Ltd. offers advanced solutions that enhance the safety and efficiency of ammonium nitrate handling in various industrial settings.