

Classification and Composition of Wheat Flour Pneumatic Conveying Systems
Wheat flour pneumatic conveying systems represent a critical technology in the food processing sector, designed to efficiently transport flour and other fine powders. These systems leverage air pressure to move materials, offering significant benefits including reduced risk of contamination, enhanced operational safety, and improved overall process efficiency. A thorough understanding of the classification and components of such systems is essential for selecting the appropriate equipment tailored to specific industrial needs.
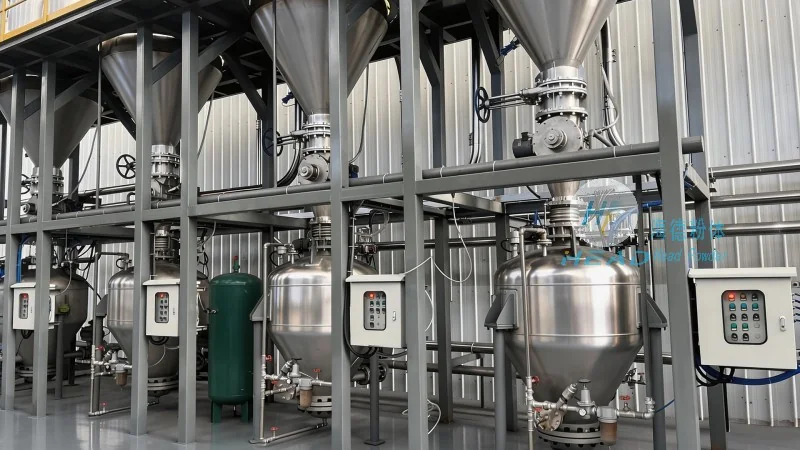
Classification of Wheat Flour Pneumatic Conveying Systems
Wheat flour pneumatic conveying systems can be broadly classified based on the direction of air flow and the method of material transport. The primary categories include:
- Absorption Type (Suction Conveying): This system operates by creating a negative pressure zone to draw materials from a source, such as a silo or storage bin, into the conveying line. It is ideal for applications requiring gentle handling of delicate powders, minimizing particle breakage and maintaining product quality.
- Compression Type (Pressure Conveying): In contrast, compression systems generate positive pressure to push materials through the pipeline. This method is suitable for longer conveying distances and higher material throughput, making it a preferred choice for large-scale flour processing facilities.
- Bidirectional Type: Some advanced systems combine both suction and pressure capabilities, allowing for flexible material handling in complex production lines. This versatility enables seamless integration with various processing stages, optimizing workflow and resource utilization.
Key Components of Wheat Flour Pneumatic Conveying Systems
Regardless of the classification, wheat flour pneumatic conveying systems typically consist of several core components that work in tandem to ensure reliable operation. These components include:
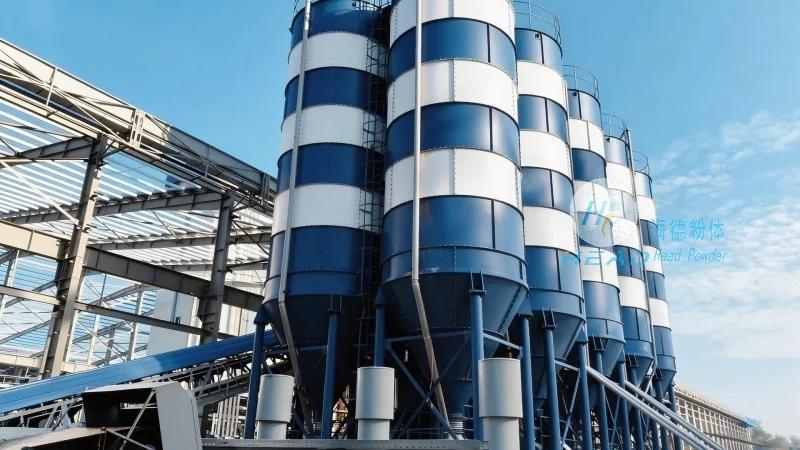
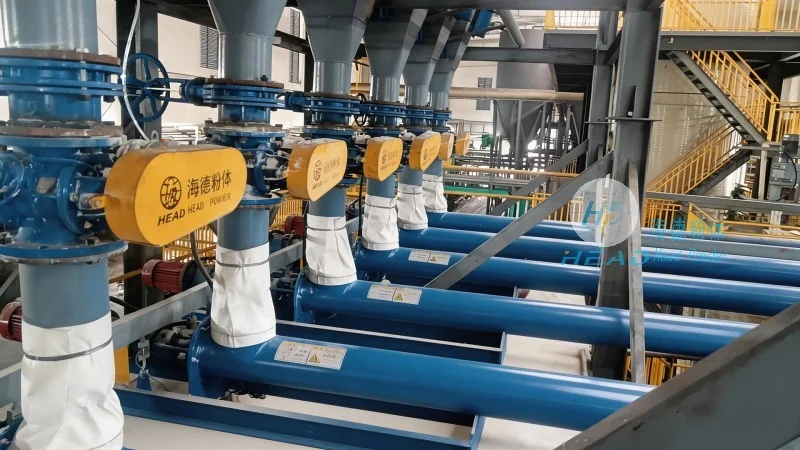
- Feeding Device: The feeding device is responsible for introducing the wheat flour or other powders into the conveying system. Common types include rotary valves, star feeders, and screw feeders, which ensure a consistent and controlled flow of material into the pipeline.
- Conveying Pipeline: The pipeline serves as the main pathway for transporting the material and air mixture. It is usually made of materials like stainless steel or food-grade plastic to prevent contamination and ensure durability. The design of the pipeline, including bends and elbows, is critical for maintaining system efficiency and minimizing pressure losses.
- Separation Device: The separation device, often a cyclone or a bag filter, is used to separate the material from the air stream at the end of the conveying process. This step is essential for recovering the flour and preventing dust emissions, ensuring compliance with environmental regulations and maintaining product purity.
- Air Source Equipment: The air source equipment, such as a blower or a compressor, provides the necessary air pressure to drive the conveying process. The choice of equipment depends on the system type (suction or pressure) and the required airflow rate, with considerations for energy efficiency and noise levels.
- Control System: Modern wheat flour pneumatic conveying systems are equipped with advanced control systems that monitor and regulate various parameters, including pressure, flow rate, and material level. These systems enhance operational stability, reduce downtime, and allow for remote monitoring and management.
HeadPowder Engineering Co., Ltd.: Your Trusted Partner in Pneumatic Conveying Solutions
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and installation of high-quality wheat flour pneumatic conveying systems. With years of experience in the industry, HeadPowder has developed a reputation for delivering customized solutions that meet the unique requirements of food processing facilities worldwide. The company’s commitment to quality, innovation, and customer satisfaction ensures that clients receive systems that are not only efficient but also reliable and cost-effective.
Customization and Application Flexibility
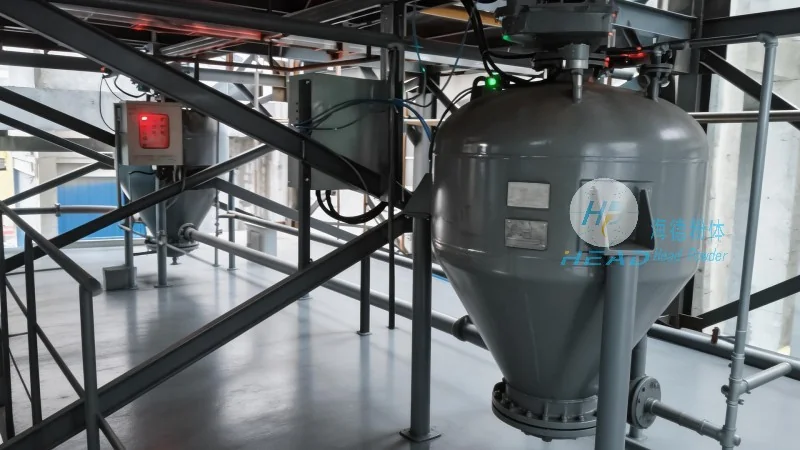
HeadPowder understands that each flour processing facility has distinct operational needs. Therefore, the company offers tailored pneumatic conveying systems that can be adapted to various production scales, material types, and environmental conditions. Whether for small-scale bakeries or large industrial mills, HeadPowder’s solutions are designed to optimize workflow, minimize waste, and enhance overall productivity. The company’s engineering team works closely with clients to assess their specific requirements, providing expert advice on system design, material selection, and installation procedures.
Benefits of Choosing HeadPowder Pneumatic Conveying Systems
Investing in a HeadPowder wheat flour pneumatic conveying system offers numerous advantages for food processing businesses. These include:
- Hygienic and Sanitary Design: All components are constructed from food-grade materials and designed to meet stringent hygiene standards, ensuring that the flour remains free from contaminants and maintains its quality throughout the conveying process.
- Energy Efficiency: Advanced air source equipment and optimized system design contribute to reduced energy consumption, leading to lower operational costs and a smaller environmental footprint.
- Reduced Downtime: Robust construction and reliable control systems minimize the risk of system failures, ensuring continuous production and maximizing operational uptime.
- Easy Maintenance: Modular design and accessible components simplify maintenance and repair procedures, reducing downtime and maintenance costs.
- Compliance with Regulations: HeadPowder systems are designed to comply with local and international regulations regarding food safety and environmental protection, providing peace of mind to clients.
Conclusion
Wheat flour pneumatic conveying systems are indispensable in modern food processing, offering efficient, hygienic, and safe material transport solutions. With its expertise and commitment to quality, HeadPowder Engineering Co., Ltd. stands as a trusted provider of these systems, delivering customized solutions that meet the evolving needs of the industry. By understanding the classification and components of these systems, and leveraging the expertise of companies like HeadPowder, food processing facilities can enhance their operational efficiency, maintain product quality, and achieve sustainable growth.