

Air Conveying Application in Bulk Transport of Diatomite Mineral Powder
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of air conveying systems tailored for the efficient bulk transport of diatomite mineral powders. This technology offers a reliable solution for industries requiring precise and low-maintenance material handling, particularly in applications where traditional mechanical conveying methods may present challenges. The air conveying system leverages compressed air to move diatomite powder through pipelines, ensuring a clean, dust-free, and controlled transport process that minimizes product contamination and operational downtime.
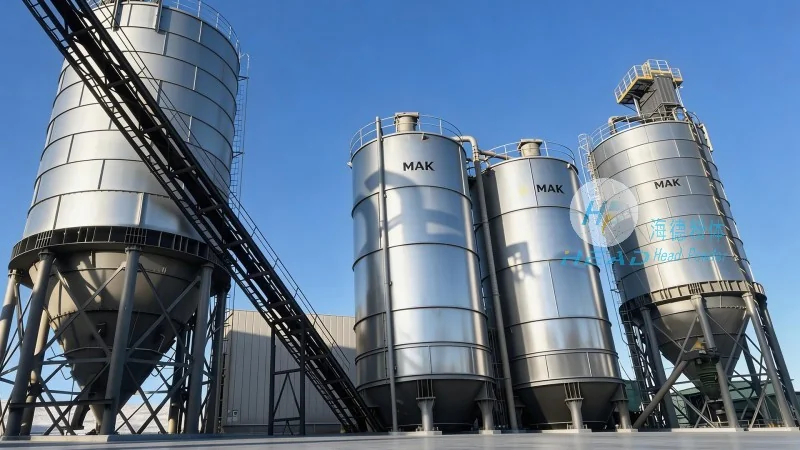
Key Advantages of Air Conveying for Diatomite Transport
When considering the bulk handling of diatomite mineral powders, air conveying systems provide several distinct advantages over conventional methods. Firstly, the system operates with minimal mechanical contact, reducing the risk of product degradation or contamination from metal parts. This is crucial for diatomite, which is often used in applications such as filtration, catalysts, and construction materials where purity is paramount. Secondly, air conveying enables a dust-free environment, enhancing workplace safety and compliance with environmental regulations. The enclosed pipeline system prevents dust emissions, making it suitable for indoor or environmentally sensitive operations. Additionally, the technology offers flexibility in pipeline layout, allowing for complex routing around obstacles and multiple delivery points without the need for extensive infrastructure modifications. The system’s self-cleaning capabilities also reduce maintenance requirements, as the air flow helps to prevent material buildup in the pipelines, extending the lifespan of the equipment.
Application Scenarios in Diatomite Processing
HeadPowder’s air conveying solutions are widely applied in various stages of diatomite processing, from raw material handling to final product distribution. In the mining and crushing phase, the system efficiently transports crushed diatomite from storage silos to grinding mills, ensuring a consistent feed rate for optimal grinding efficiency. During the drying process, air conveying can be integrated to move dried diatomite from drying chambers to storage or packaging areas, maintaining the material’s moisture content within specified limits. The technology is also utilized in the packaging stage, where it accurately delivers diatomite powder into bags or containers, minimizing spillage and improving packaging accuracy. Furthermore, the system supports continuous production lines, enabling seamless material flow between different processing units, which is essential for maintaining high throughput in diatomite processing facilities.
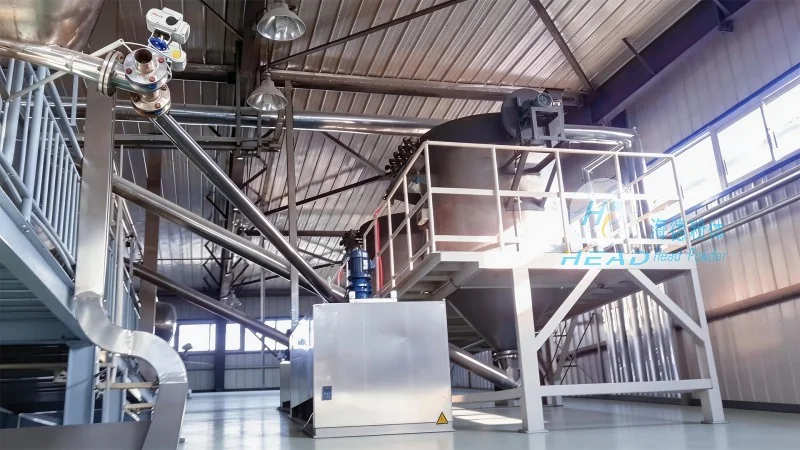
Technical Specifications and Customization Options
HeadPowder’s air conveying systems are designed with customizable specifications to meet the unique requirements of diatomite transport applications. The system includes components such as rotary air locks, which prevent backflow and maintain pressure differentials in the pipeline, and dust collectors that capture any airborne particles, ensuring compliance with air quality standards. The pipeline diameter and length can be tailored to the specific volume and distance of material transport, with options for both positive and negative pressure systems depending on the application. For diatomite, which has a relatively low bulk density, the system may incorporate larger diameter pipelines or higher air velocities to maintain flow rates. The control systems are equipped with sensors to monitor pressure, flow rate, and material level, providing real-time data for process optimization and troubleshooting. Additionally, the equipment is constructed from materials resistant to corrosion and abrasion, such as stainless steel or special alloys, to withstand the chemical and physical properties of diatomite over extended operational periods.
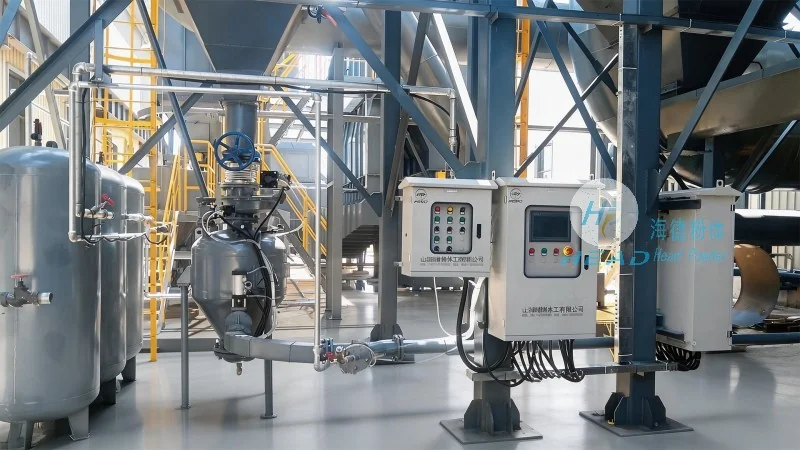
Operational Benefits and Cost Efficiency
The implementation of air conveying technology in diatomite mineral powder transport offers significant operational benefits and cost savings for processing facilities. By reducing the need for manual handling and mechanical conveyors, the system minimizes labor costs and the risk of workplace injuries. The enclosed pipeline design eliminates dust-related health hazards, improving employee safety and reducing the need for extensive cleaning and maintenance of the facility. From a financial perspective, the low maintenance requirements and long service life of the air conveying equipment result in lower operational costs compared to traditional methods. The system’s ability to handle large volumes of material efficiently reduces production time and increases overall throughput, contributing to higher productivity and revenue. Furthermore, the technology’s adaptability allows for easy integration with existing processing lines, minimizing downtime during installation and ensuring a smooth transition to the new system.
Conclusion and Future Outlook
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to advance air conveying technology for the bulk transport of diatomite mineral powders, providing industries with a reliable, efficient, and cost-effective solution. The company’s expertise in customizing air conveying systems ensures that each installation meets the specific needs of the diatomite processing facility, whether it involves small-scale operations or large industrial plants. As the demand for high-purity diatomite products grows, the importance of efficient and clean material handling becomes increasingly critical. HeadPowder’s air conveying solutions not only address these needs but also contribute to sustainable operations by reducing waste and improving environmental compliance. With ongoing technological advancements and customization options, the future of air conveying in diatomite transport looks promising, offering continued improvements in efficiency, safety, and cost-effectiveness for processing industries.