

Application of Pneumatic Conveying in the Bulk Transport of Food Additives
HeadPowder, a leading provider of bulk material handling solutions, specializes in pneumatic conveying systems tailored for the food additive industry. This article explores the application of pneumatic conveying in efficiently transporting food additives, highlighting the benefits and technical considerations for food processing facilities.
The Advantages of Pneumatic Conveying in Food Additive Handling
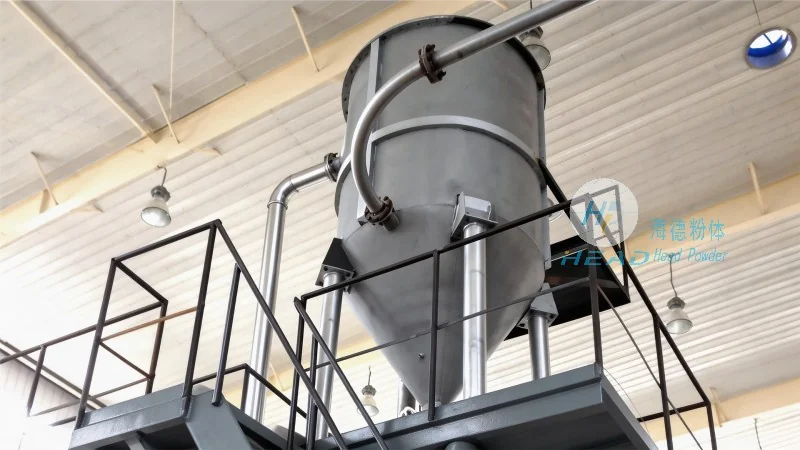
Pneumatic conveying offers several key benefits when handling food additives. First, it ensures a fully enclosed system, preventing cross-contamination and maintaining the purity of the additives. This is critical in the food industry where product safety and regulatory compliance are paramount. Additionally, the technology allows for gentle handling of sensitive materials, preserving the quality and integrity of the additives without causing degradation or agglomeration. The system also offers flexibility in transporting various forms of food additives, including powders, granules, and fine particles, adapting to different particle sizes and flow characteristics.
Key Features of Pneumatic Conveying Systems for Food Additives
HeadPowder’s pneumatic conveying systems are engineered with food safety in mind. The equipment is typically constructed from high-grade stainless steel, ensuring resistance to corrosion and easy cleaning. Many systems incorporate CIP (Clean-In-Place) designs, allowing for thorough sanitation without disassembling components. This is essential for maintaining hygiene standards and meeting regulatory requirements such as those from the FDA or EU food safety guidelines. The systems also feature advanced control mechanisms, enabling precise regulation of air flow, pressure, and material feed rates, which optimizes the conveying process and minimizes energy consumption.
Types of Pneumatic Conveying Systems Used in Food Additive Transport
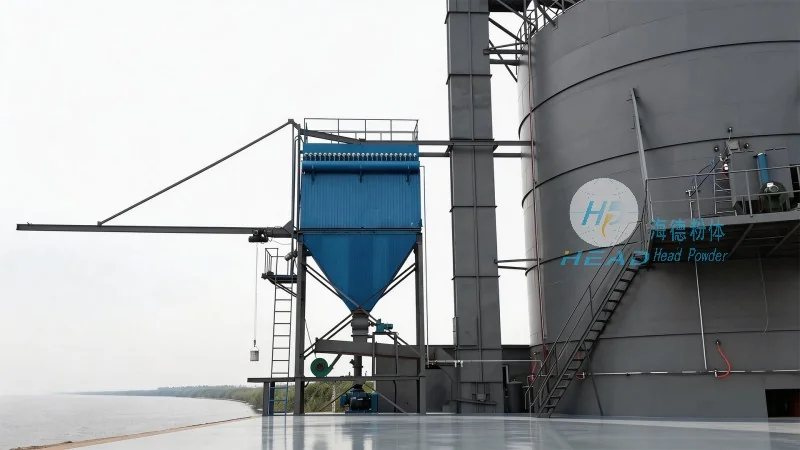
There are two primary types of pneumatic conveying systems commonly used for food additives: positive pressure and negative pressure systems. Positive pressure systems, often called pressure or blow-through systems, use a blower to force air and material through the pipeline. This method is effective for long-distance and high-capacity transport, making it suitable for large-scale food additive handling operations. Negative pressure systems, or vacuum systems, use a vacuum to draw material from a hopper into the pipeline. These are ideal for applications requiring gentle material handling or where the material needs to be transported from multiple sources to a central location. Both systems can be customized to meet specific operational needs, such as varying the air-to-material ratio to control conveying velocity and system efficiency.
Application Examples: Transporting Common Food Additives
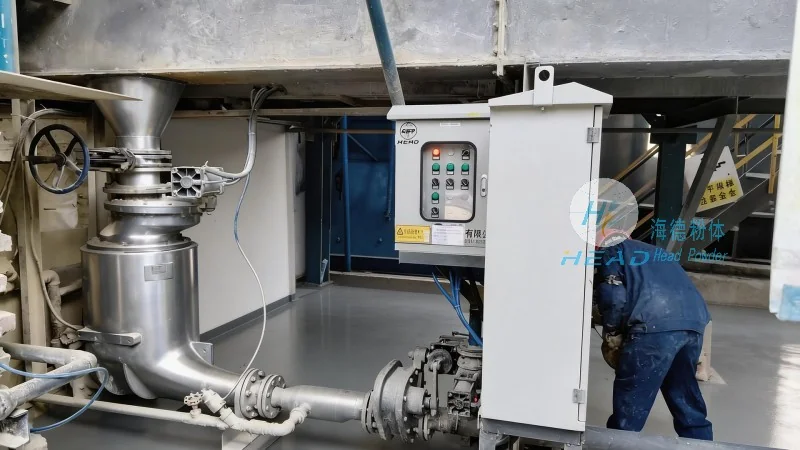
HeadPowder’s pneumatic conveying solutions are applied in the transport of a wide range of food additives. For instance, sweeteners like sucrose or high-fructose corn syrup powders are efficiently conveyed using positive pressure systems, ensuring consistent flow and minimal dust generation. Antioxidants and preservatives, which are often in fine powder form, benefit from the gentle handling provided by vacuum systems, preventing agglomeration and maintaining their effectiveness. Colorants and flavor enhancers, such as natural pigments or essential oils, are also handled with care, as the enclosed system prevents contamination and preserves their sensory properties. In each case, the system design considers the specific physical and chemical properties of the additive, ensuring optimal performance and product quality.
Customization and Integration: Tailoring Pneumatic Conveying Solutions
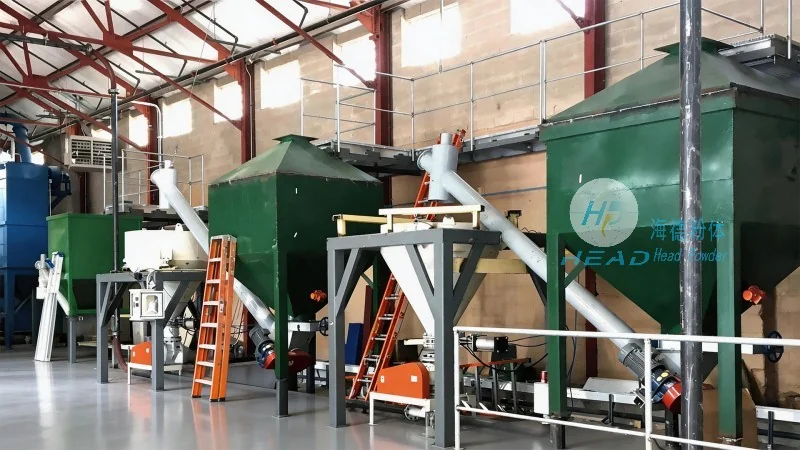
HeadPowder understands that each food processing facility has unique requirements. Therefore, the company offers customized pneumatic conveying solutions that integrate seamlessly with existing production lines. This includes designing systems that can handle varying batch sizes, accommodate different storage and processing equipment, and comply with specific industry standards. The company’s engineering team works closely with clients to assess their operational needs, material characteristics, and space constraints, developing a tailored solution that maximizes efficiency and minimizes downtime. Additionally, HeadPowder provides comprehensive support, including system installation, commissioning, and ongoing maintenance services, ensuring long-term reliability and performance.
Conclusion: The Role of Pneumatic Conveying in Food Additive Logistics
Pneumatic conveying is a critical technology in the efficient and safe transport of food additives. Its ability to provide enclosed, hygienic, and flexible handling makes it an indispensable part of modern food processing operations. HeadPowder, with its expertise in bulk material handling, continues to innovate and provide advanced pneumatic conveying systems that meet the evolving needs of the food additive industry. By leveraging these systems, food manufacturers can enhance operational efficiency, reduce costs, and ensure the highest standards of product safety and quality.