

Design of Cement Aggregate Pneumatic Conveying Systems
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for cement and aggregate materials. Our expertise lies in creating efficient, reliable, and cost-effective solutions that meet the stringent demands of modern industrial applications.
Key Features of Our Pneumatic Conveying Systems
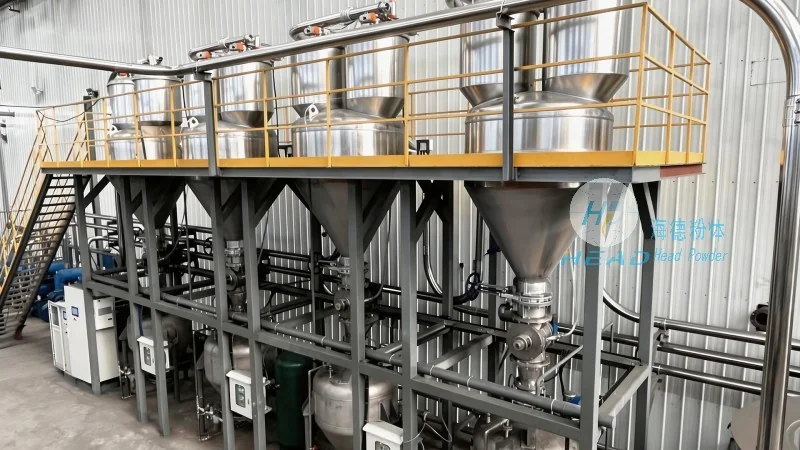
Our cement aggregate pneumatic conveying systems are engineered with precision to ensure optimal performance. The design incorporates high-quality components, including robust airlocks, efficient cyclones for separation, and durable pipelines that can withstand the abrasive nature of cement and aggregate particles. The systems are equipped with advanced control panels that allow for real-time monitoring and adjustment, ensuring consistent material flow and minimizing downtime.
System Components and Their Functions
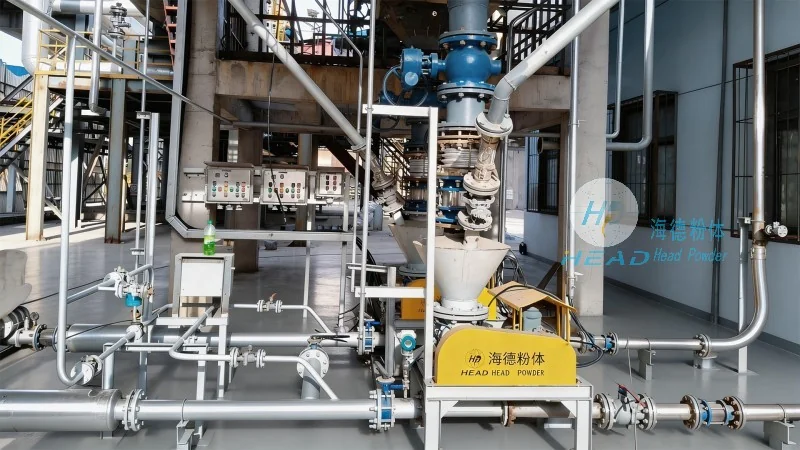
The core components of our pneumatic conveying system include the material hopper, which serves as the storage and feeding unit; the air compressor, responsible for generating the necessary air pressure to transport materials; and the conveying pipeline network that connects the feeding and discharge points. Additionally, we integrate specialized equipment such as rotary valves and check valves to regulate the flow and prevent backflow, enhancing the system's reliability and safety.
Advantages of Choosing HeadPowder's Systems
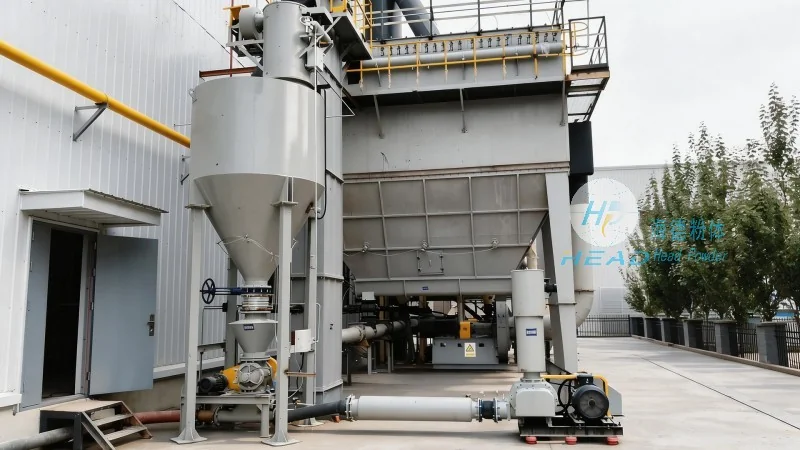
By selecting HeadPowder's pneumatic conveying systems, clients benefit from several key advantages. The systems offer a significant reduction in material handling costs compared to traditional methods like belt conveyors or bucket elevators. They also provide a more hygienic and dust-free environment, which is crucial for cement production facilities aiming to maintain high standards of cleanliness. Furthermore, the modular design allows for easy expansion or modification, adapting to evolving production needs without major overhauls.
Customization and Application Scope
HeadPowder understands that each industrial facility has unique requirements. Therefore, our pneumatic conveying systems are highly customizable to fit specific operational parameters, such as material type, flow rate, and distance. We have successfully implemented these systems in various applications, including cement plants, mining operations, and construction material processing facilities. Our solutions are designed to handle a wide range of materials, from fine powders to coarse aggregates, ensuring versatility and adaptability across different industries.
Quality Assurance and Technical Support
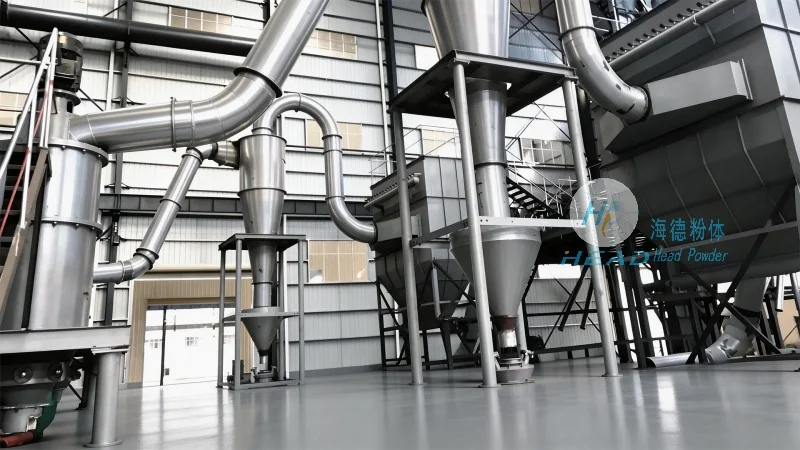
At HeadPowder, we adhere to stringent quality control measures throughout the design, manufacturing, and installation phases. Each system undergoes rigorous testing to ensure compliance with industry standards and client specifications. Moreover, our team provides comprehensive technical support, including on-site installation supervision, commissioning, and long-term maintenance services. This commitment to quality and service ensures that our clients receive not only a superior product but also a reliable partner for their material handling needs.