

Principle and Operational Scenario Features of Air-Driven Conveying Lines for Fine Coal Powder Mater
When it comes to transporting fine coal powder materials efficiently and reliably, air-driven conveying systems have emerged as a highly effective solution. These systems leverage the power of compressed air to move powders through pipelines, offering a range of advantages over traditional methods such as belt conveyors or bucket elevators. The principle behind these systems involves creating a pressure differential that propels the material along the pipeline, ensuring a smooth and continuous flow. This approach not only enhances operational efficiency but also minimizes material degradation and contamination risks, making it ideal for applications where product quality is paramount.
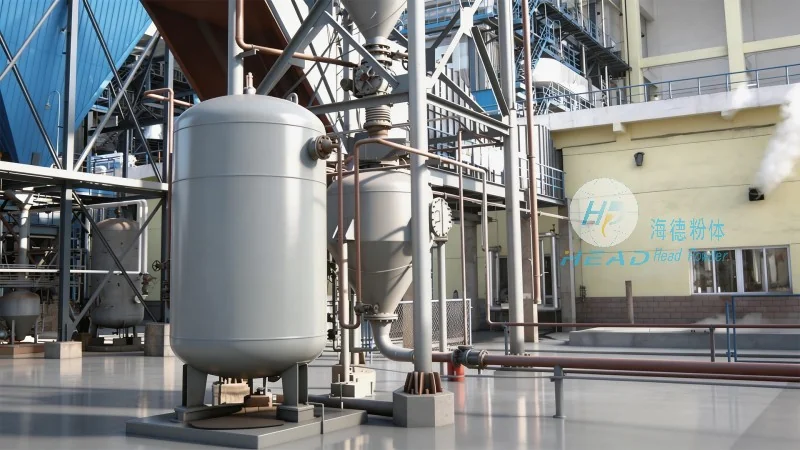
The Working Principle of Air-Driven Conveying Lines
At the core of an air-driven conveying system is the use of compressed air to generate the necessary force for material transport. The system typically consists of a series of components, including a blower or compressor, a hopper for material loading, a pipeline network, and a discharge point. The process begins with the material being fed into the hopper, where it is then drawn into the pipeline by the air flow. As the air moves through the system, it carries the fine coal powder along the path, maintaining a consistent velocity and pressure to prevent blockages or uneven distribution. The design of the pipeline, including the use of bends, valves, and filters, is critical to ensuring optimal performance and preventing material buildup or air leakage.
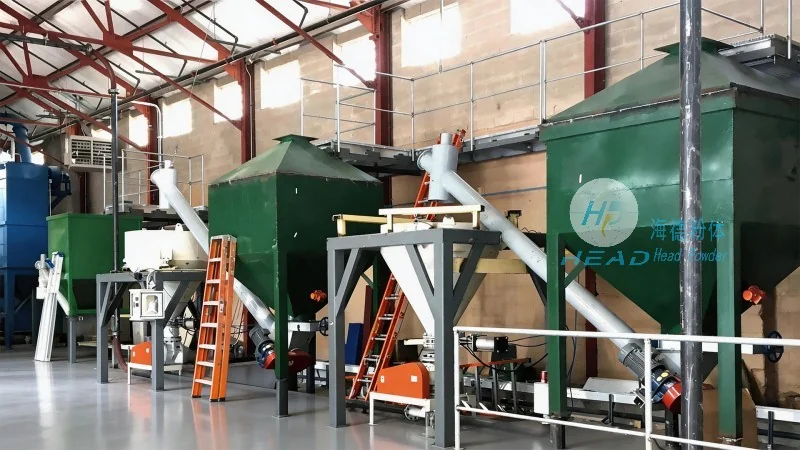
Key Features and Advantages of Air-Driven Conveying Systems
One of the primary advantages of air-driven conveying lines is their ability to handle fine and abrasive materials without causing excessive wear or degradation. Unlike mechanical systems that rely on moving parts in direct contact with the material, air-driven systems minimize friction and impact, preserving the integrity of the coal powder. Additionally, these systems are highly flexible, allowing for changes in the layout or direction of the pipeline without major modifications. This adaptability makes them suitable for various industrial settings, from mining and power generation to chemical processing and food production. Another key feature is the ability to transport materials over long distances with minimal energy consumption compared to other methods. The use of compressed air as the primary driving force is energy-efficient and can be integrated with existing air systems in many facilities, reducing overall operational costs.
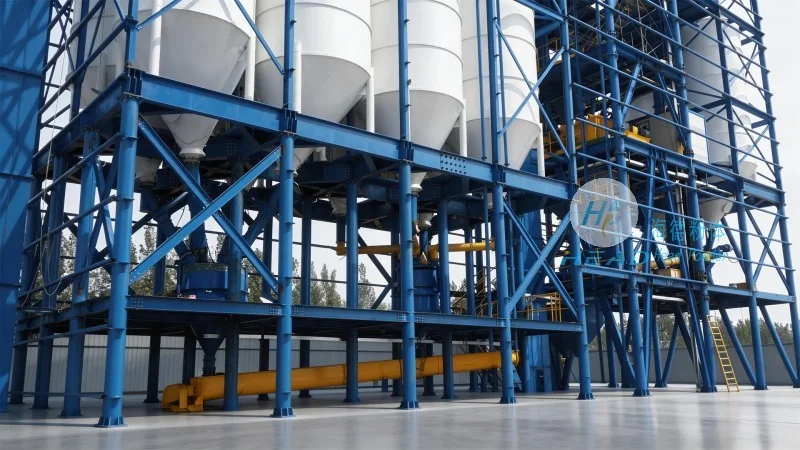
Working Scenario Characteristics of Air-Driven Conveying Lines
The application of air-driven conveying systems is characterized by specific operational scenarios that highlight their suitability for handling fine coal powder materials. These scenarios typically involve environments where dust control and material containment are critical. For instance, in power plants, these systems are used to transport coal from storage silos to boilers, ensuring a continuous and dust-free supply. In mining operations, they help move fine coal from processing facilities to storage or transport vehicles, maintaining a clean and efficient workflow. The systems are also commonly used in chemical plants where the handling of fine powders requires precise control over flow rates and particle size distribution. The ability to adjust air pressure and flow rates allows operators to optimize the conveying process for different material types and particle sizes, ensuring consistent performance under varying conditions.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of air-driven conveying solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing systems tailored to the unique needs of industrial applications. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's expertise lies in the integration of advanced technology with practical engineering, ensuring that their systems meet the highest standards of performance and durability. The company's commitment to customer satisfaction is reflected in its comprehensive support services, including system design, installation, and maintenance. Based in Shandong, China, HeadPowder leverages its local presence to provide timely and effective solutions for clients across various industries, contributing to the advancement of material handling technologies.