

What Is Powder Material Conveying Equipment? And What Are Its Design Principles?
When it comes to the efficient handling and transportation of bulk materials, especially in industries dealing with powders and granules, specialized equipment plays a crucial role. Powder material conveying equipment, also known as bulk material handling systems, are engineered to move materials like minerals, chemicals, and other fine particles from one location to another with precision and reliability. These systems are essential in various sectors, including mining, food processing, pharmaceuticals, and manufacturing, where the consistent and safe transfer of powders is critical for operational efficiency and product quality.
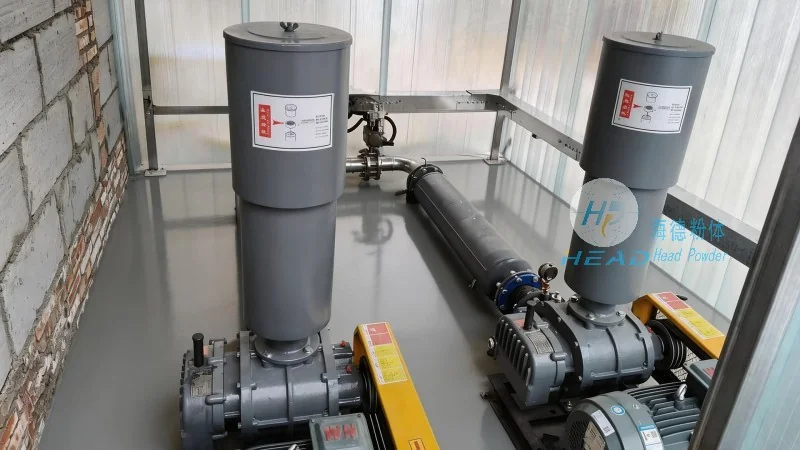
Understanding the Core Function of Powder Material Conveying Equipment
Powder material conveying equipment is designed to transport loose, dry materials in bulk. Unlike solid or liquid materials, powders present unique challenges due to their fine particle size, potential for dust generation, and susceptibility to caking or bridging. The primary goal of these systems is to ensure that powders are moved without degradation, contamination, or loss. This involves controlling factors such as flow rate, pressure, and material density to maintain a consistent and controlled transport process.
The Design Principles Behind Efficient Powder Conveying
The design of powder material conveying equipment is based on several key principles that address the specific characteristics of powders. One fundamental principle is the use of low-pressure, high-volume systems to minimize particle breakage and prevent dust accumulation. This is achieved through the application of positive displacement or pneumatic conveying methods, which use air or gas to move materials through pipelines. Another critical design principle is the incorporation of smooth, non-stick surfaces and proper sealing to prevent material buildup and ensure clean operation. Additionally, the equipment is often equipped with features like vibration or agitation mechanisms to prevent clogging and maintain consistent flow.
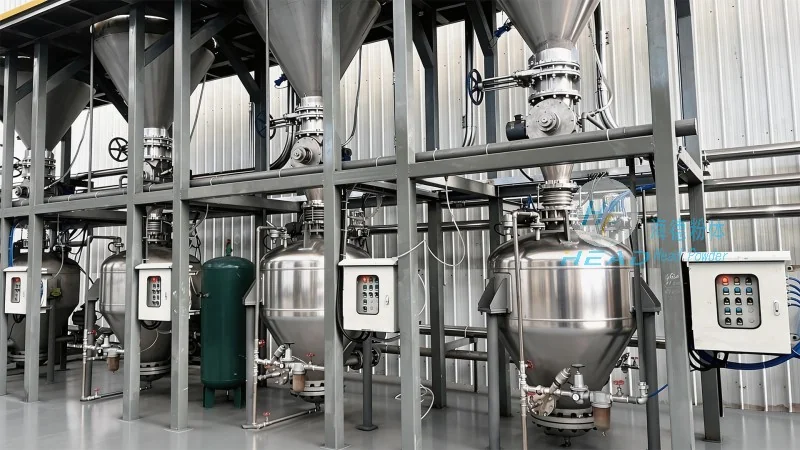
Key Components and Their Roles in the Conveying Process
Several key components work together to ensure the effective operation of powder material conveying equipment. The feed hopper is the initial component that collects and stores the powder material before it is introduced into the conveying system. It is designed to handle the bulk of the material and provide a controlled feed rate. The conveyor itself, which can be pneumatic or mechanical, is responsible for moving the material through the system. Pneumatic conveyors use air pressure to push or pull the material, while mechanical conveyors rely on belts, screws, or buckets to transport it. The discharge system then delivers the material to its final destination, ensuring a smooth and controlled release. Finally, control systems and monitoring devices are integrated to regulate the flow, pressure, and other parameters, ensuring optimal performance and safety.
Applications and Industries That Benefit from These Systems
Powder material conveying equipment is widely used across various industries due to its versatility and efficiency. In the mining industry, these systems are used to transport ore and other minerals from mines to processing facilities. In the chemical industry, they handle raw materials and finished products, ensuring safe and efficient transfer. The food and pharmaceutical industries also rely on these systems to maintain product purity and prevent contamination. Additionally, in manufacturing, they are used to move raw materials to production lines and finished products to storage areas. The adaptability of these systems makes them suitable for a wide range of applications, from small-scale operations to large industrial facilities.
Advantages of Using Professional Powder Conveying Solutions
Investing in high-quality powder material conveying equipment offers numerous advantages for businesses. One of the primary benefits is improved operational efficiency, as these systems can handle large volumes of material with minimal downtime. They also enhance safety by reducing the risk of dust explosions and material spills, which are common hazards in powder handling. Additionally, these systems help maintain product quality by preventing contamination and degradation during transport. The ability to customize the equipment to specific material characteristics and process requirements further enhances its effectiveness. Overall, the use of professional powder conveying solutions leads to cost savings, increased productivity, and better compliance with industry regulations.

Choosing the Right Equipment for Your Needs
When selecting powder material conveying equipment, it is essential to consider several factors to ensure the best fit for your specific application. The first consideration is the type of material being handled, as different materials have different properties that require specialized equipment. For example, abrasive or corrosive materials may require more durable components. The second factor is the required capacity and flow rate, as the system must be able to handle the volume of material needed for your operations. The third consideration is the distance and layout of the conveying path, as this will determine the type of conveyor system (e.g., pneumatic vs. mechanical) and the number of components needed. Additionally, the integration with existing systems and the availability of maintenance support are important factors to consider. Working with a reputable manufacturer, such as Shandong HeadPowder Engineering Co., Ltd., can help ensure that the chosen equipment meets all your requirements and provides long-term reliability.
Conclusion: The Importance of Reliable Powder Conveying Equipment
In conclusion, powder material conveying equipment is a vital component in industries that rely on the efficient handling of bulk materials. The design principles behind these systems are carefully engineered to address the unique challenges of powder transport, ensuring consistent, safe, and efficient operation. By understanding the key components and advantages of these systems, businesses can make informed decisions when selecting equipment that meets their specific needs. Whether in mining, chemicals, food, or manufacturing, investing in high-quality powder conveying solutions from a trusted provider like Shandong HeadPowder Engineering Co., Ltd. can lead to improved productivity, safety, and overall operational success. HeadPowder, based in Shandong, China, specializes in providing tailored bulk material handling solutions that meet the diverse needs of various industries.