

Phosphates Pneumatic Conveying: A Solution for Material Transport Beyond Distance Limits
Phosphates are essential raw materials in various industrial applications, including agriculture, food processing, and chemical manufacturing. The efficient and reliable transport of these materials is crucial for maintaining production efficiency and ensuring product quality. Traditional methods like belt conveyors or bucket elevators often face limitations when dealing with long-distance or complex layouts. This is where phosphates pneumatic conveying systems offer a superior alternative, enabling seamless material transport over extended distances with minimal operational constraints.
HeadPowder Engineering: Your Trusted Partner in Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder) is a leading provider of advanced material handling solutions, specializing in the design, manufacturing, and installation of phosphates pneumatic conveying systems. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for industries relying on phosphates processing. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality engineering services tailored to global market needs.
Key Features of Phosphates Pneumatic Conveying Systems
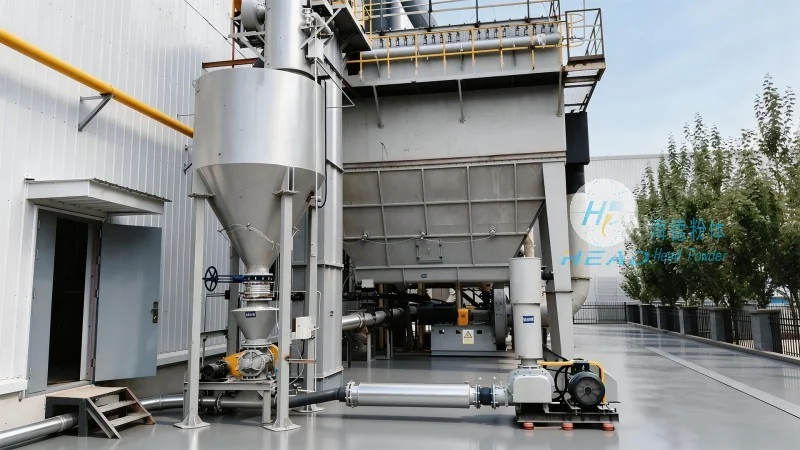
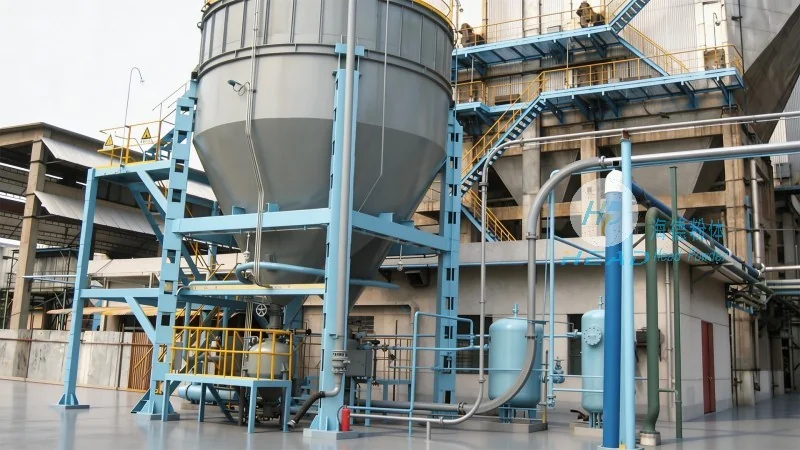
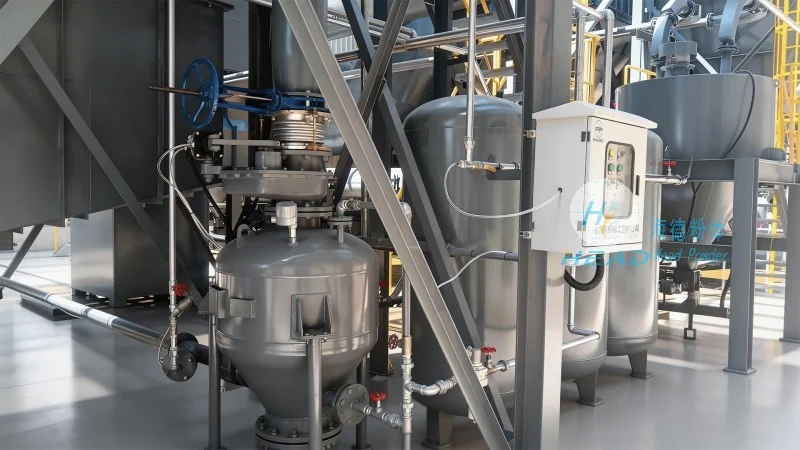
Phosphates pneumatic conveying systems utilize air as the primary medium to transport bulk materials. This technology offers several advantages over conventional methods, including: extended transport distances, flexible system layouts, and minimal material degradation. The system typically consists of a hopper, a conveyor line, and a receiver, with air being introduced to create a flow of material through the pipeline. For phosphates, which are often fine powders or granules, the design of the conveying system is critical to prevent clogging and ensure consistent flow rates. HeadPowder's engineers employ advanced computational fluid dynamics (CFD) and material testing to optimize system performance, ensuring reliable operation even with challenging material properties.

Applications in Phosphates Processing
Phosphates pneumatic conveying systems are widely used in the processing of various phosphate-based products. In agricultural applications, these systems facilitate the transport of phosphate fertilizers from storage silos to blending and packaging lines, enabling efficient distribution to farms. In the chemical industry, they are used to move raw phosphate materials to reaction vessels, ensuring a steady supply for production processes. The ability to transport materials over long distances without the need for multiple transfer points makes the system ideal for large-scale industrial facilities. HeadPowder's solutions have been successfully implemented in plants handling both wet and dry phosphate materials, demonstrating adaptability to diverse operational conditions.
Advantages of Choosing HeadPowder for Pneumatic Conveying
When selecting a pneumatic conveying system for phosphates, several factors come into play. HeadPowder stands out due to its comprehensive approach to system design and implementation. The company's engineers work closely with clients to understand their specific material characteristics, production volumes, and operational requirements. This collaborative process ensures that the final system is optimized for performance, reliability, and cost-effectiveness. Additionally, HeadPowder provides comprehensive after-sales support, including system maintenance, troubleshooting, and upgrades, ensuring long-term operational efficiency. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, providing clients with peace of mind regarding the performance and safety of their conveying systems.
Conclusion: Enhancing Efficiency with Phosphates Pneumatic Conveying
Phosphates pneumatic conveying systems represent a significant advancement in material handling technology, offering industries a reliable solution to overcome distance and layout challenges. By leveraging advanced engineering and customer-centric design, HeadPowder Engineering provides tailored solutions that meet the unique needs of phosphate processing facilities. With its expertise and commitment to excellence, HeadPowder continues to be a leader in delivering efficient and sustainable material transport solutions for the global phosphates industry. Whether for new plant installations or system upgrades, choosing HeadPowder ensures that industries can achieve optimal performance and maintain a competitive edge in their operations.