

Principle and Working Scene Characteristics of Coal Ash Particle Material Pneumatic Conveying System
Coal ash, a byproduct of coal combustion, presents unique challenges in material handling due to its granular nature and varying particle sizes. Pneumatic conveying systems offer an efficient and reliable solution for transporting coal ash particles from production sites to processing or disposal locations. This article explores the fundamental principles of such systems and highlights key working scene characteristics that make them suitable for coal ash handling applications.
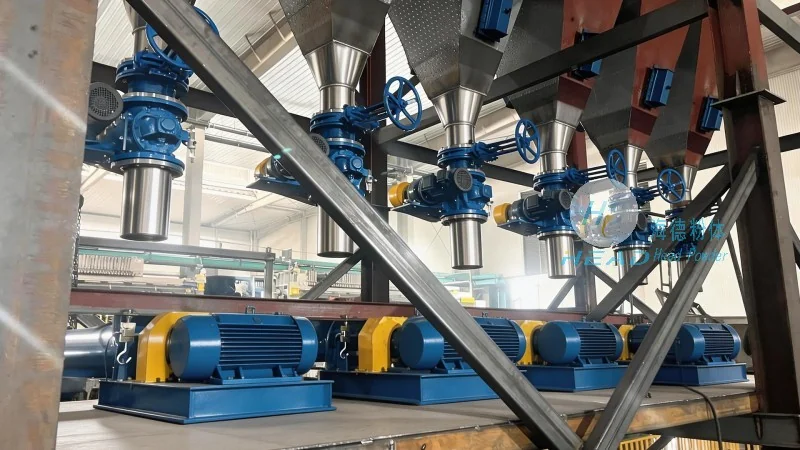
Principle of Pneumatic Conveying for Coal Ash Particles
The core principle of pneumatic conveying involves the use of air or gas to transport solid particles through a pipeline. In the case of coal ash, the system typically operates under positive pressure (pressure pneumatic conveying) or negative pressure (vacuum pneumatic conveying). Positive pressure systems use a blower to force air and particles through the pipeline, while negative pressure systems use a vacuum pump to draw particles into the system. The choice between these methods depends on factors such as the distance of transport, the volume of material, and the need to minimize dust emissions. For coal ash, which is often fine and prone to dusting, positive pressure systems are commonly preferred as they provide better control over particle flow and reduce the risk of clogging in the pipeline.
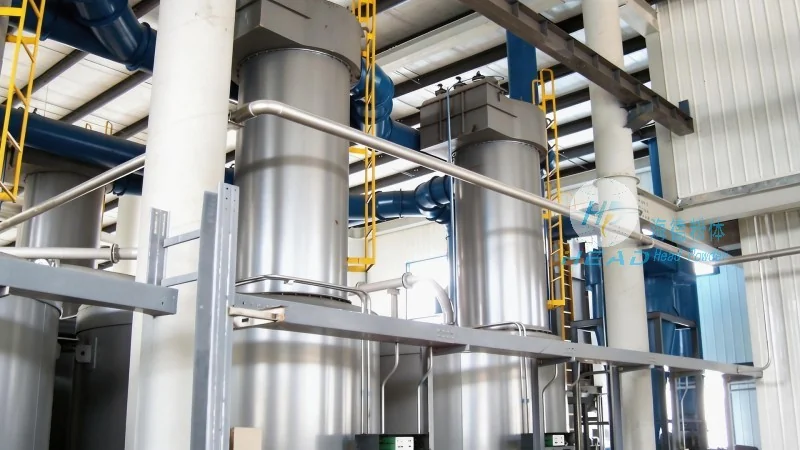
Working Scene Characteristics of Coal Ash Pneumatic Conveying Systems
The effectiveness of a coal ash pneumatic conveying system is heavily influenced by the specific working environment. Several key characteristics define these systems in practical applications:
- High Efficiency and Capacity: Pneumatic conveying systems can handle large volumes of coal ash particles at high speeds, making them ideal for industrial-scale operations where continuous material flow is required. The ability to transport material over long distances without the need for intermediate storage or manual handling significantly improves operational efficiency.
- Reduced Dust and Environmental Impact: Unlike traditional belt or bucket elevators, pneumatic systems minimize dust generation and dispersion. This is crucial for coal ash, which can be hazardous if inhaled. The enclosed pipeline design and controlled air flow help maintain a clean working environment and comply with environmental regulations.
- Flexibility in Layout: Pneumatic conveying systems can be easily integrated into existing industrial layouts. They can be configured to transport material in multiple directions, including vertical and horizontal combinations, allowing for complex system designs that adapt to the spatial constraints of the facility. This flexibility is particularly valuable in coal ash processing plants where space is often limited.
- Low Maintenance and Durability: Modern pneumatic conveying systems are designed with durable materials that can withstand the abrasive nature of coal ash particles. The absence of moving parts in the pipeline (except for the air supply equipment) reduces wear and tear, leading to lower maintenance costs and longer system lifespans. This makes them a cost-effective solution for long-term coal ash handling operations.
Application Scenarios and Practical Implementation
Coal ash pneumatic conveying systems are widely used in various industrial settings, including power plants, cement factories, and waste management facilities. In power plants, for example, these systems are employed to transport coal ash from the boiler to storage silos or to other processing units for further utilization. The ability to handle large volumes of ash quickly and efficiently supports the continuous operation of the power generation process. In cement factories, coal ash is often used as a supplementary cementitious material, and pneumatic conveying systems ensure a steady supply of ash to the production line, enhancing the overall productivity of the facility.
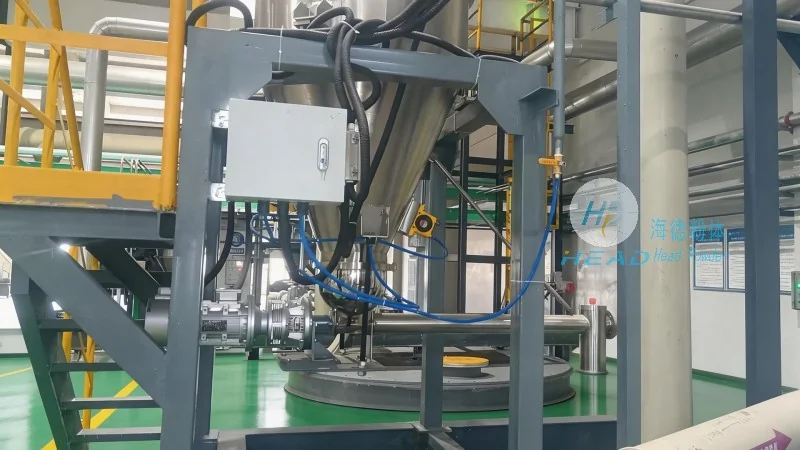
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for material handling and processing. With a focus on innovative and efficient systems, HeadPowder has developed advanced pneumatic conveying technologies tailored to the unique requirements of coal ash and other granular materials. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality products and services to clients worldwide. HeadPowder’s commitment to quality, reliability, and customer satisfaction has established it as a trusted partner in the industrial material handling sector.