

Principles and Application Scenarios of Pneumatic Conveying for Rare Earth Crystal Powder Materials
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for handling rare earth crystal powders. This article delves into the fundamental principles of such systems and highlights the distinct characteristics of their operational environments.
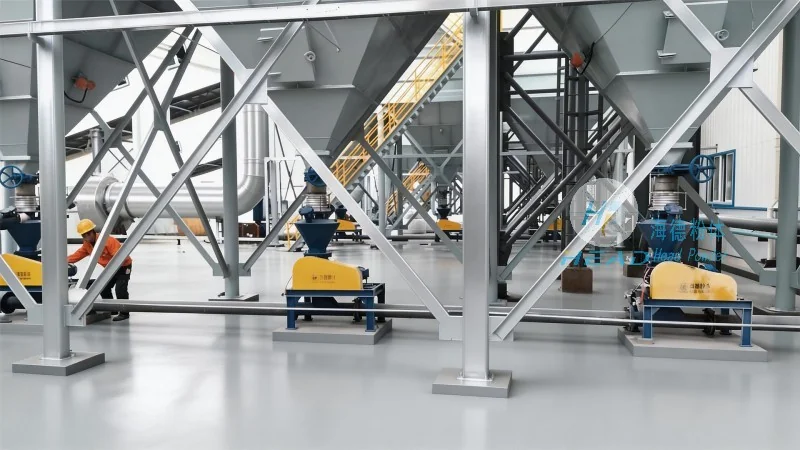
Company Overview
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to providing comprehensive solutions for material handling in industrial settings. With a strong focus on precision and efficiency, the company has established itself as a trusted partner for clients requiring specialized equipment for transporting rare earth materials. HeadPowder's expertise lies in optimizing pneumatic conveying processes to meet the unique demands of the rare earth industry, ensuring safe, reliable, and cost-effective material transport.
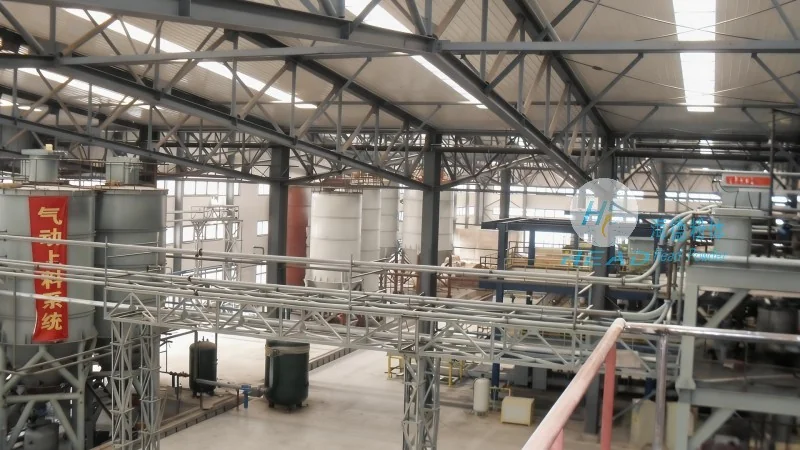
The Principle of Pneumatic Conveying
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials, including rare earth crystal powders, through a pipeline using a flow of gas, typically air. The core principle involves creating a pressure differential within the system, which propels the material forward. In the case of rare earth crystal powders, the system is engineered to handle fine, abrasive, and potentially hazardous materials, requiring precise control over air flow, pressure, and material velocity to prevent degradation or blockages.
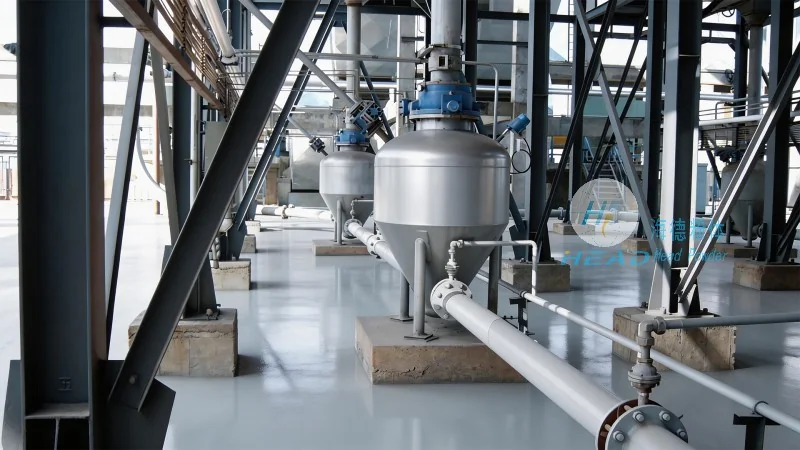
Key Working Scenarios and Characteristics
The application of pneumatic conveying for rare earth crystal powders is characterized by several distinct operational scenarios. These include short-distance and long-distance transport within industrial facilities, as well as integration with downstream processing equipment such as reactors, furnaces, and storage silos. The systems are designed to operate under varying conditions, from low to high pressure, and can be configured for both positive and negative pressure modes depending on the specific material handling requirements. A key characteristic is the ability to maintain material integrity, preventing agglomeration or contamination during transport, which is critical for maintaining the quality of rare earth products.
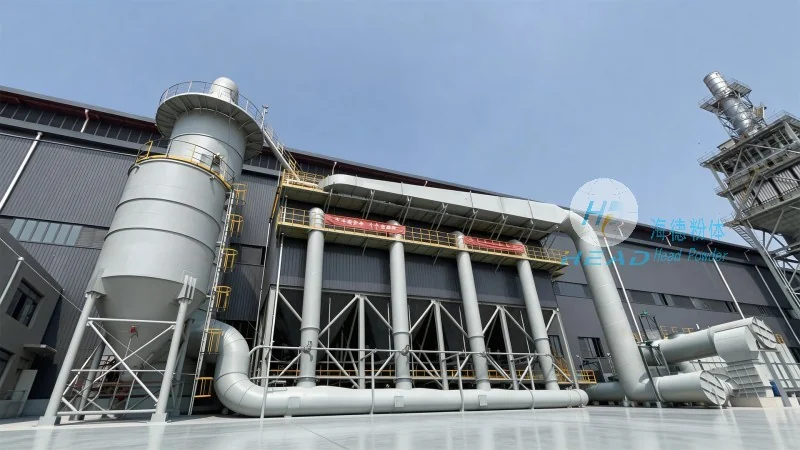
Technical Advantages and Practical Applications
The pneumatic conveying systems developed by HeadPowder offer several technical advantages that make them ideal for rare earth crystal powder handling. These include high efficiency in material transport, reduced labor costs due to automated processes, and enhanced safety by minimizing direct human contact with hazardous materials. Practical applications range from the initial extraction and processing stages to the final packaging and distribution of rare earth products. The systems are also adaptable to different production scales, from small-scale laboratory operations to large-scale industrial plants, ensuring versatility and scalability. By leveraging advanced engineering and material science, HeadPowder's solutions ensure that rare earth crystal powders are conveyed with minimal loss, maximum purity, and optimal operational performance.