

What is a Dust Collector Gas-Pneumatic Conveying Line? And What Are Its Design Principles?
For industrial applications that require efficient handling of collected dust, a gas-pneumatic conveying line is a critical system. This equipment is designed to transport dust and other particulate materials from a dust collector to a storage or processing location. Understanding the components and design principles of such a line is essential for optimizing performance and ensuring reliable operation in various industrial settings.
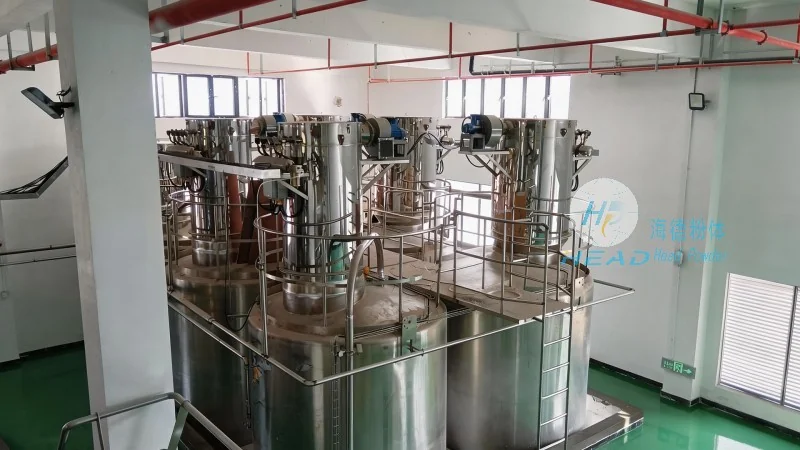
Key Components of a Dust Collector Gas-Pneumatic Conveying System
The core of a dust collector gas-pneumatic conveying line consists of several key components that work in tandem to achieve effective material transport. These include the dust collector itself, which captures airborne particles, and the conveying line, which transports the collected material. The system typically incorporates a blower or air compressor to generate the necessary airflow, a hopper or collection bin to hold the dust, and a pipeline network that connects these components. Additionally, control valves and check valves may be included to regulate airflow and prevent backflow, ensuring smooth and controlled material movement.
Design Principles for Efficient Dust Transport
The design of a dust collector gas-pneumatic conveying line is guided by several fundamental principles aimed at maximizing efficiency and minimizing operational issues. One of the primary principles is maintaining consistent airflow velocity throughout the system. This ensures that the particulate material remains suspended in the air stream, preventing clogging and ensuring reliable transport. The pipeline diameter and length are carefully selected to balance the required airflow with the material's properties, such as particle size and moisture content. Additionally, the system is designed to minimize pressure drop, which is crucial for maintaining the necessary airflow without excessive energy consumption. Proper sealing of connections and use of appropriate materials for the pipeline and components are also critical to prevent leaks and maintain system integrity.
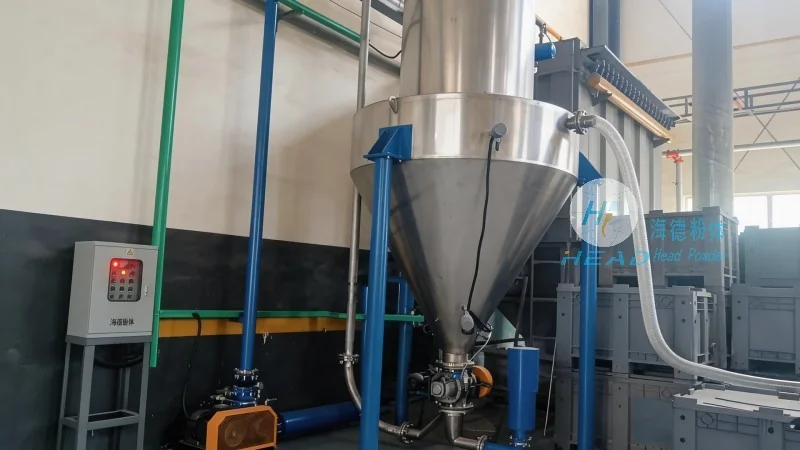
Application in Industrial Environments
Dust collector gas-pneumatic conveying lines are widely used in industries such as manufacturing, mining, and food processing, where dust and particulate matter are generated during production processes. In these applications, the system plays a vital role in maintaining air quality and ensuring compliance with environmental regulations. By efficiently transporting collected dust to a designated storage area, the system helps prevent dust accumulation and potential health hazards. The design of the conveying line is tailored to the specific characteristics of the material being handled, such as its density, abrasiveness, and moisture content, to ensure optimal performance and longevity of the equipment.
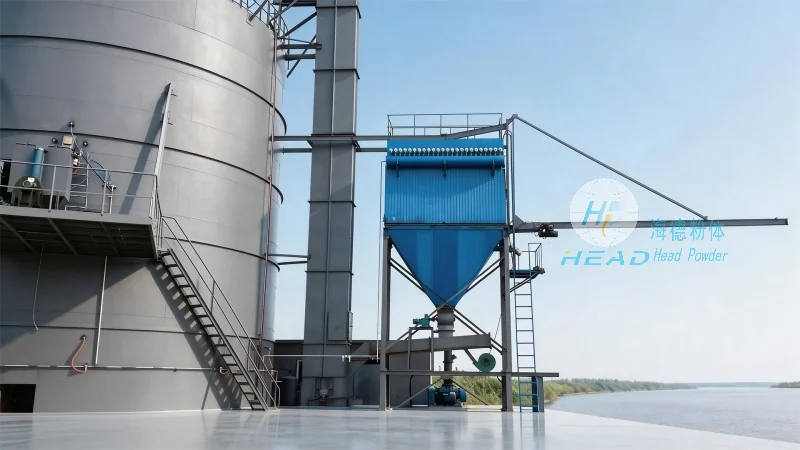
Benefits of Using a Gas-Pneumatic Conveying Line
Implementing a dust collector gas-pneumatic conveying line offers several significant benefits for industrial operations. One of the key advantages is the ability to handle a wide range of materials, from fine powders to larger particulates, with minimal maintenance. The system is also highly flexible, allowing for easy integration with existing dust collection systems and adaptation to changing production needs. Additionally, the use of compressed air as the conveying medium eliminates the need for mechanical components like belts or screws, reducing the risk of wear and tear and lowering maintenance costs. The system's ability to operate continuously and reliably contributes to improved overall productivity and reduced downtime in industrial facilities.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of dust collection and material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing gas-pneumatic conveying systems tailored to the needs of various industrial sectors. HeadPowder's expertise lies in understanding the unique challenges of different applications and developing customized solutions that enhance operational efficiency and environmental compliance. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry, offering comprehensive support from system design to installation and maintenance.