

What is a Brewery Sludge Pneumatic Conveying System? And What Are Its Design Principles?
Brewery sludge, a byproduct of the brewing process, requires efficient and hygienic handling to maintain operational efficiency and compliance with environmental regulations. A pneumatic conveying system is a specialized solution designed to transport this material through a network of pipes using air pressure or vacuum. This technology offers advantages such as reduced labor costs, minimized contamination risks, and the ability to handle materials in a closed system, which is crucial for maintaining product quality and hygiene standards in breweries.
Understanding the Core Components of a Pneumatic Conveying System
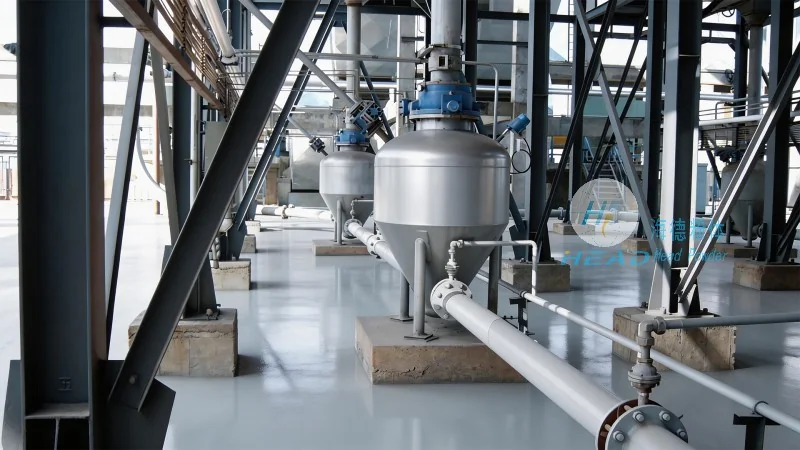
The design of a brewery sludge pneumatic conveying system involves several key components that work in concert to ensure reliable operation. The primary components include the material feed hopper, which stores and feeds the sludge into the system; the conveying line, typically made of stainless steel to resist corrosion and maintain hygiene; the air supply system, which generates the necessary pressure or vacuum to move the material; and the control valves and sensors that regulate the flow and ensure system safety. Each component is engineered to withstand the specific challenges of handling brewery sludge, such as its high moisture content and potential for clogging.
Design Principles for Efficient Material Transport
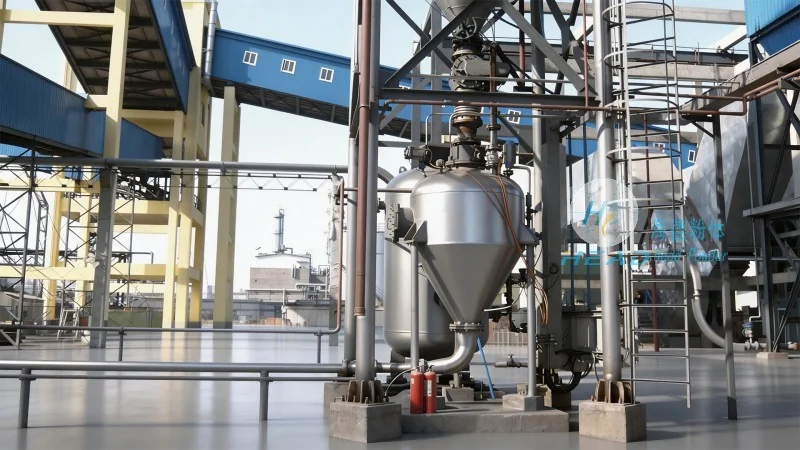
The design principles of a pneumatic conveying system for brewery sludge focus on optimizing the flow of material and air to achieve maximum efficiency and minimal energy consumption. One key principle is the selection of the appropriate conveying velocity, which must be high enough to prevent material settling but low enough to avoid excessive wear on the system components. The system design also considers the sludge's properties, including its moisture content, particle size, and density, as these factors directly impact the required air pressure and flow rate. Additionally, the system incorporates features like in-line mixers and cyclone separators to maintain consistent material flow and prevent blockages, ensuring smooth operation over extended periods.
Advantages of Using a Pneumatic Conveying System for Brewery Sludge
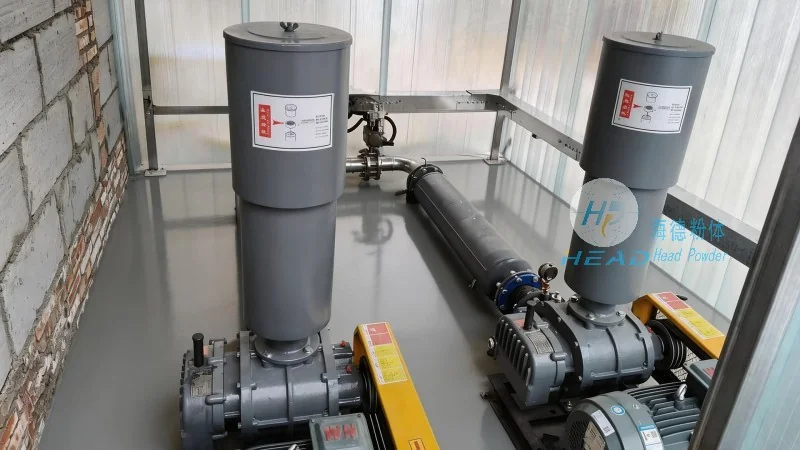
Implementing a pneumatic conveying system for brewery sludge offers several significant advantages over traditional methods like manual handling or mechanical conveyors. Firstly, it provides a completely enclosed system, which eliminates the risk of cross-contamination and odor spread, maintaining a clean and hygienic environment in the brewery. Secondly, it reduces labor costs by automating the material transport process, minimizing the need for manual labor and associated risks. Thirdly, the system is highly flexible, allowing for easy integration with existing brewery infrastructure and the ability to adjust the conveying capacity as production needs change. Finally, the use of stainless steel construction ensures durability and ease of cleaning, which is essential for maintaining compliance with food safety regulations.
Customization and Scalability of Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the industry, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of breweries. The company's expertise lies in understanding the unique challenges of handling brewery sludge and developing solutions that address these challenges effectively. Their systems are scalable, ranging from small-scale installations for smaller breweries to large-scale systems for industrial-scale operations. The company's team of engineers works closely with clients to assess their specific requirements, including the volume of sludge to be handled, the distance of transport, and the desired level of automation, to design a system that meets all operational and regulatory requirements. This customized approach ensures that the system is not only efficient but also cost-effective and sustainable in the long term.
Ensuring Compliance and Reliability in Brewery Operations
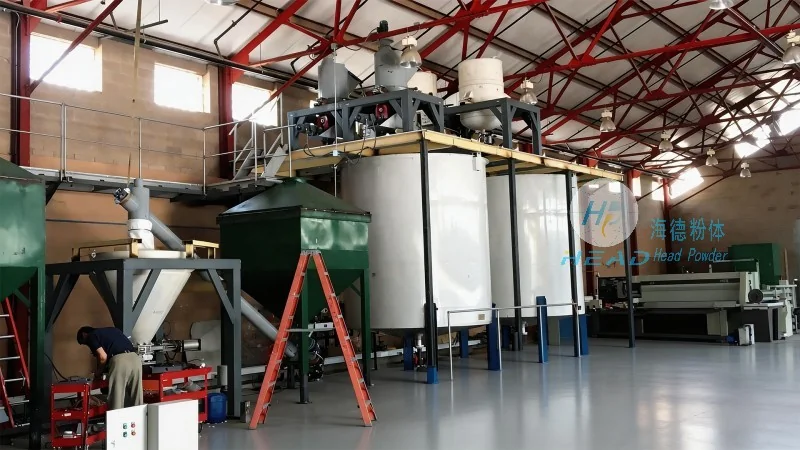
For breweries, maintaining compliance with environmental and food safety regulations is paramount. A well-designed pneumatic conveying system for brewery sludge helps achieve this by providing a closed system that prevents the release of odors and contaminants into the environment. The use of stainless steel and other hygienic materials ensures that the system meets the stringent standards set by regulatory bodies. Additionally, the system's reliability is critical for maintaining uninterrupted production. Shandong HeadPowder Engineering Co., Ltd. ensures that their systems are built with high-quality components and undergo rigorous testing to guarantee long-term reliability. This reliability is further enhanced by the company's commitment to providing comprehensive after-sales support, including maintenance services and technical assistance, to ensure that the system operates at peak performance throughout its lifespan.