

Introduction to Calcite Powder Conveying System: Overview of Structure and Working Principle
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and integration of advanced conveying systems tailored for industrial applications. Our company, Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China, and has established a strong reputation for delivering reliable and efficient solutions for the transportation of various powders, including calcite.
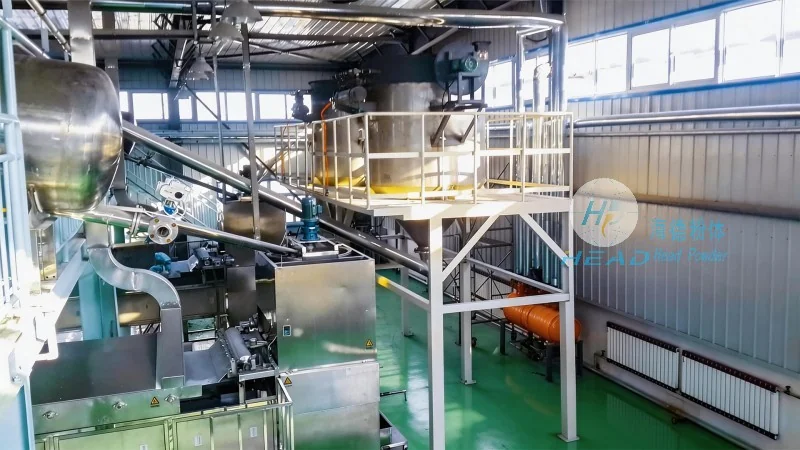
The Calcite Powder Conveying System: A Comprehensive Overview
The calcite powder conveying system is a sophisticated piece of equipment engineered to handle the unique challenges associated with calcite powder, a widely used mineral in industries such as construction, paper, and chemical manufacturing. This system is designed to ensure safe, efficient, and consistent transportation of calcite powder from storage to processing units, minimizing material loss and operational downtime.
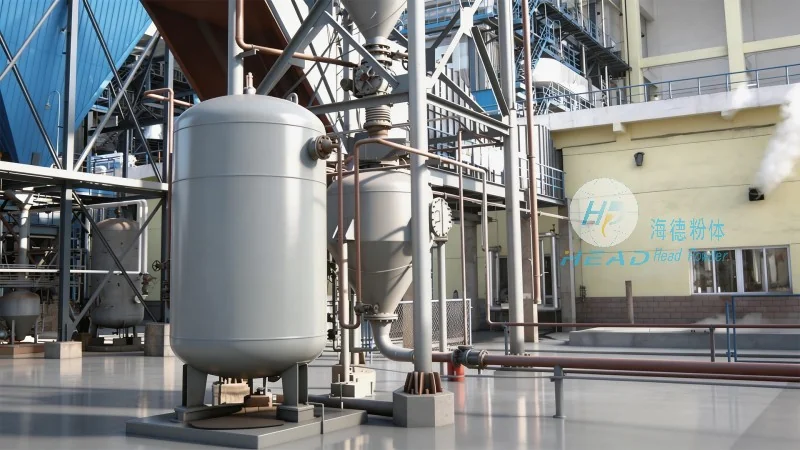
Key Components and Structural Design
The system's structure comprises several critical components that work in tandem to achieve optimal performance. The primary components include a hopper for material storage, a conveyor mechanism (such as a screw or pneumatic conveyor) for material transport, and a control panel for monitoring and adjusting operational parameters. The hopper is typically made of durable materials like stainless steel or corrosion-resistant alloys to withstand the abrasive nature of calcite powder. The conveyor system is engineered to handle the specific flow characteristics of calcite, ensuring smooth and continuous movement without clogging or blockages.
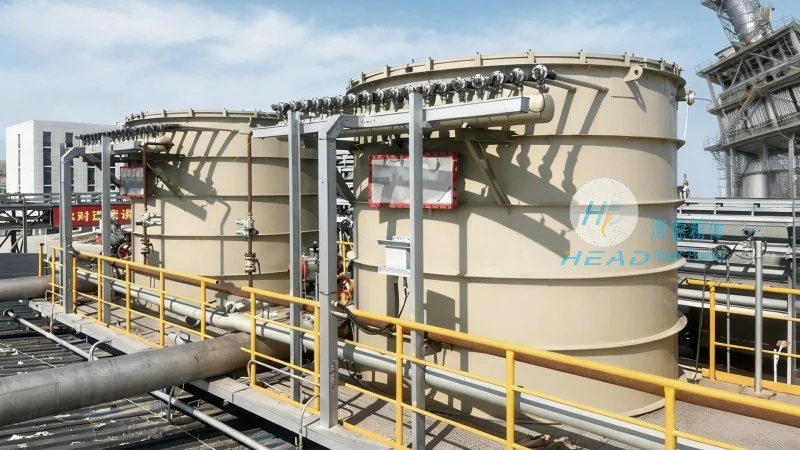
Working Principle of the Conveying System
The operational principle of the calcite powder conveying system is based on the controlled movement of material through the conveyor components. The process begins with the material being fed into the hopper, where it is stored until needed. A motor-driven conveyor (e.g., a screw conveyor) then transports the calcite powder from the hopper to the discharge point. The speed and direction of the conveyor can be adjusted via the control panel to regulate the flow rate, ensuring that the material is delivered at the required rate for downstream processes. Additionally, the system may incorporate features like vibration or air-assisted mechanisms to prevent material bridging and ensure uniform flow.
Advantages and Applications
The calcite powder conveying system offers several advantages that make it an ideal choice for industrial applications. Its design minimizes material degradation and contamination, which is crucial for maintaining product quality in calcite-based products. The system also reduces labor costs by automating the material handling process, allowing for continuous operation with minimal human intervention. In industries such as cement production, paper manufacturing, and chemical processing, this system is widely used to transport calcite powder efficiently and safely.
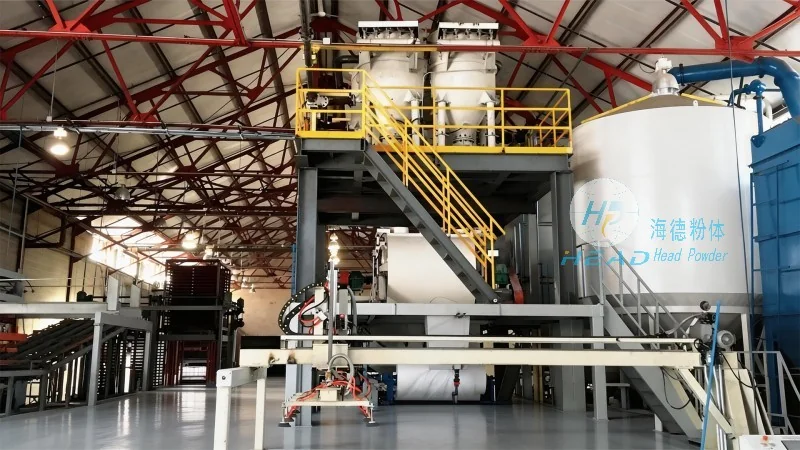
Quality Assurance and Technical Support
HeadPowder is committed to providing high-quality products and reliable technical support to its clients. Our calcite powder conveying systems undergo rigorous quality control tests to ensure compliance with industry standards and customer requirements. We offer comprehensive after-sales services, including maintenance, repair, and technical assistance, to ensure the long-term performance and reliability of our systems. Our team of experienced engineers and technicians is available to provide guidance and support throughout the entire lifecycle of the system.