

Operation Process and Working Principle of Bin Pump Material Handling Line
Bin pumps are a critical component in bulk material handling systems, designed to transport powders and granular materials over long distances with high efficiency and reliability. The bin pump material handling line, as a comprehensive system, integrates various components to ensure seamless material transfer from storage to processing or discharge points. This article will delve into the operation process and working principle of such a line, highlighting key elements and their functions, presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
Key Components of the Bin Pump Material Handling Line
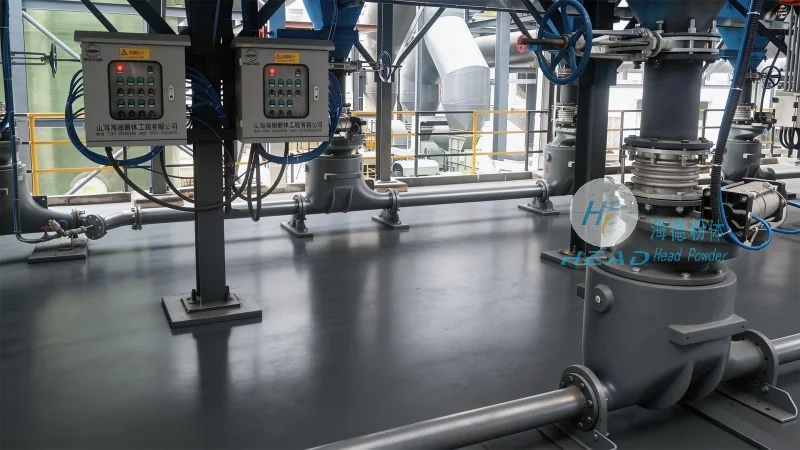
The bin pump material handling line typically consists of several interconnected parts, each playing a vital role in the overall material transfer process. The main components include the bin pump itself, feeders, conveyors, control systems, and discharge equipment. The bin pump, often a positive displacement type, is responsible for creating the pressure needed to move material through the pipeline. Feeders, such as rotary or vibratory types, ensure a consistent and controlled flow of material into the pump. Conveyors, including pneumatic or mechanical systems, transport material from the bin to the pump and then to the discharge point. The control system monitors and regulates the operation of all components, maintaining optimal performance and safety. Discharge equipment, like valves or chutes, directs the material to its final destination.
Working Principle of the Bin Pump Material Handling Line
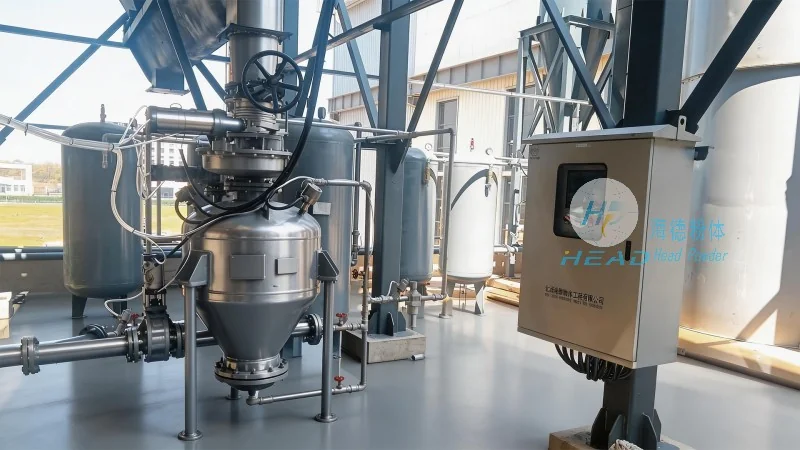
The working principle of the bin pump material handling line is based on the positive displacement mechanism, where the pump's rotor or impeller rotates to trap and move material through the pipeline. When the material is fed into the pump, it is enclosed in the pump chamber and then forced out by the rotating blades or vanes. This creates a pressure differential that drives the material forward. The process is continuous, with the pump operating in cycles to maintain a steady flow rate. The system is designed to handle a wide range of materials, from fine powders to coarse granules, with minimal degradation or segregation. The control system adjusts the speed of the pump and feeders to match the material flow rate, ensuring smooth operation and preventing blockages or overloading.
Operation Process of the Bin Pump Material Handling Line
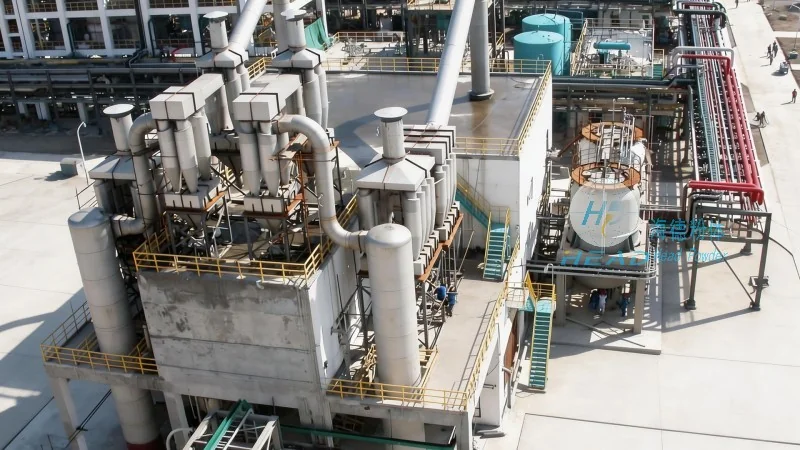
The operation process of the bin pump material handling line involves several steps to ensure efficient and safe material transfer. First, the material is stored in a hopper or silo, from which it is fed into the bin pump feeder. The feeder regulates the flow rate, preventing excess material from entering the pump. Next, the material is drawn into the bin pump chamber as the rotor rotates, creating a vacuum that pulls material in. The trapped material is then expelled through the discharge port, moving it along the pipeline to the next stage. The control system monitors the pressure and flow rate, adjusting the pump speed as needed to maintain consistent performance. During operation, the system is continuously monitored for any signs of blockage or malfunction, with alarms and safety features in place to prevent accidents. The process is automated, with minimal human intervention required, ensuring high efficiency and reliability.
Advantages of the Bin Pump Material Handling Line
The bin pump material handling line offers several advantages over traditional material handling methods. One of the key benefits is its ability to transport materials over long distances without the need for intermediate storage or transfer points. This reduces the overall system complexity and cost. The positive displacement mechanism ensures a consistent flow rate, even with varying material properties or load conditions. The system is also highly flexible, capable of handling a wide range of materials, including those that are abrasive, corrosive, or prone to segregation. Additionally, the automated control system enhances safety and reduces the risk of human error, leading to improved operational efficiency and reduced downtime.
Applications of the Bin Pump Material Handling Line
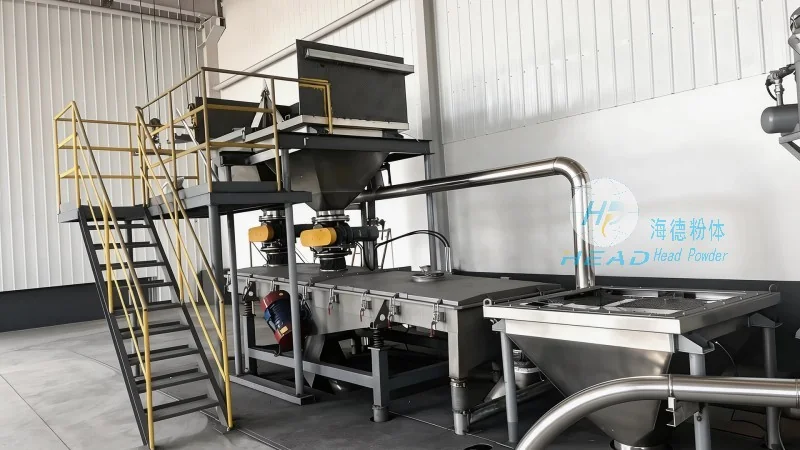
The bin pump material handling line is widely used in various industries, including chemical, pharmaceutical, food, and mining. In the chemical industry, it is used to transport powders and granules for processing, such as in the production of fertilizers or chemicals. In the pharmaceutical industry, the system is used to handle raw materials and finished products, ensuring a clean and controlled environment. The food industry utilizes the line for transporting ingredients like flour, sugar, or spices, maintaining hygiene and quality standards. In the mining industry, the system is used to transport ore and other minerals from storage to processing facilities. The versatility and efficiency of the bin pump material handling line make it an ideal solution for various bulk material handling applications.