

Operation Process and Working Principle of Intelligent Centralized Powder Material Handling System
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder material handling technology, specializes in the research, development, and application of intelligent centralized powder transport systems. The intelligent centralized powder material handling system is a comprehensive solution designed to efficiently manage the storage, transport, and distribution of bulk powder materials in industrial production processes. This system integrates advanced automation technology, precise control systems, and intelligent monitoring capabilities to ensure stable, reliable, and safe operation of powder material handling tasks.
Core Components and System Architecture
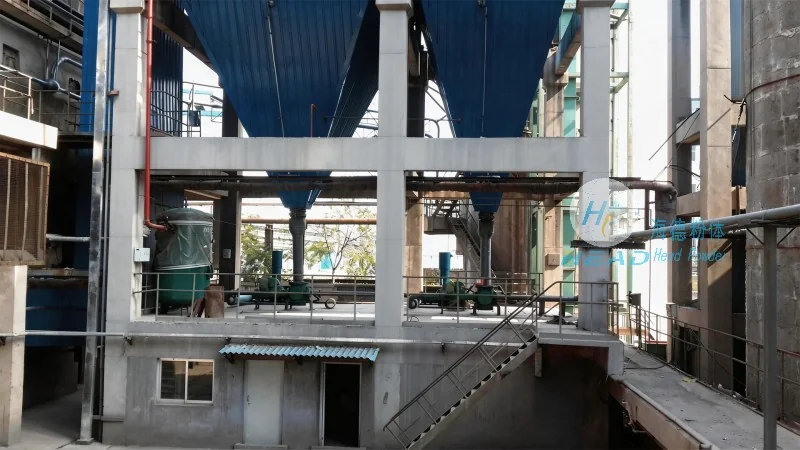
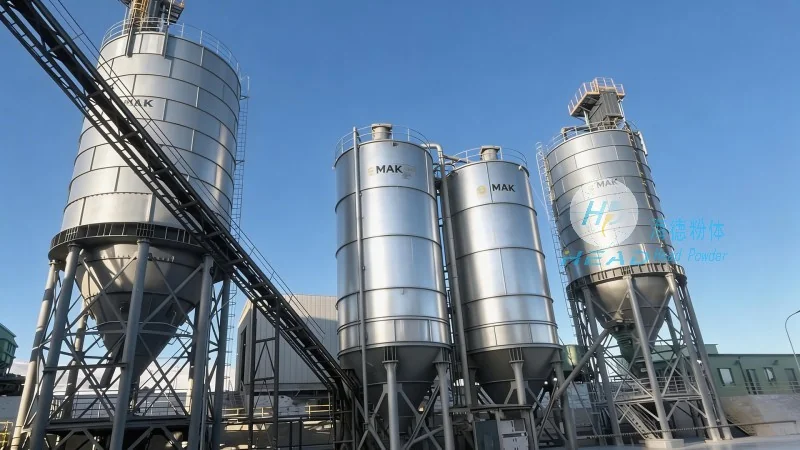
The intelligent centralized powder material handling system typically consists of several key components, including powder storage silos, conveying equipment (such as pneumatic conveying pipelines, screw conveyors, or bucket elevators), automated control systems, and intelligent monitoring devices. The system architecture is designed to achieve seamless coordination among different components, enabling the efficient flow of powder materials from storage to processing points. The storage silos are equipped with level sensors and pressure monitoring devices to ensure accurate material inventory management. The conveying equipment is equipped with variable frequency drives and intelligent control algorithms to adjust conveying speed and pressure according to real-time production requirements, thereby optimizing energy consumption and material transport efficiency.
Operation Process of the System
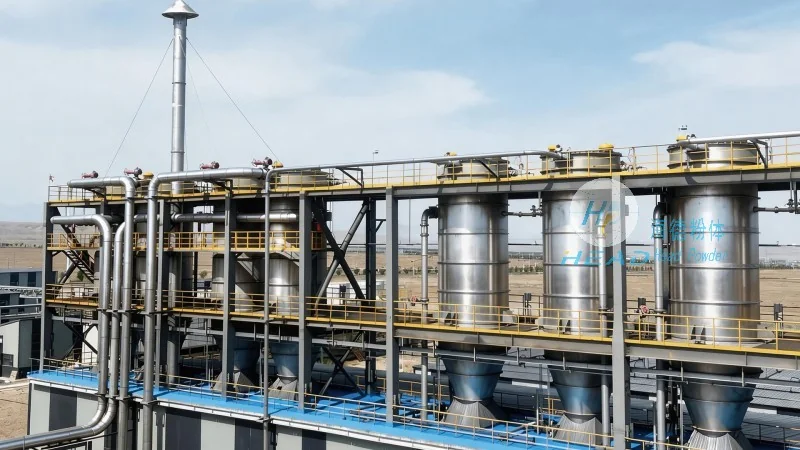
The operation process of the intelligent centralized powder material handling system involves several key steps, starting from material loading into the storage silos to the final delivery to the processing units. First, raw powder materials are loaded into the storage silos through bulk loading equipment or manual feeding. The system then uses level sensors to monitor the material level in each silo, providing real-time data to the control system. When the production line requires powder, the control system initiates the conveying process by activating the appropriate conveying equipment. The system adjusts the conveying parameters (such as air pressure, speed, and flow rate) based on the material characteristics and production demand to ensure stable material flow. During the conveying process, the system continuously monitors the pressure and flow rate in the conveying pipelines to detect any abnormalities, such as blockages or leaks. If an abnormal condition is detected, the system will automatically stop the conveying process and alert the operators, ensuring the safety and reliability of the operation. After the powder is delivered to the processing units, the system updates the inventory data and prepares for the next cycle of material handling.
Working Principle of the System
The working principle of the intelligent centralized powder material handling system is based on the integration of automation control technology and intelligent monitoring. The system uses a central control unit (CCU) to coordinate the operation of all components. The CCU receives input signals from various sensors (such as level sensors, pressure sensors, and flow sensors) and processes them to generate control commands for the conveying equipment and other components. The system employs a closed-loop control strategy, where the actual operation parameters are continuously compared with the set parameters, and adjustments are made in real time to maintain stable operation. For example, when the material level in a silo decreases, the control system will automatically start the feeding process to replenish the material. The system also includes fault diagnosis and self-recovery functions, which can automatically detect and resolve common issues, such as pipeline blockages or equipment malfunctions, reducing downtime and improving system reliability. Additionally, the system supports remote monitoring and management, allowing operators to access real-time data and control the system from a central control room or even remotely, enhancing operational efficiency and flexibility.
Advantages and Applications
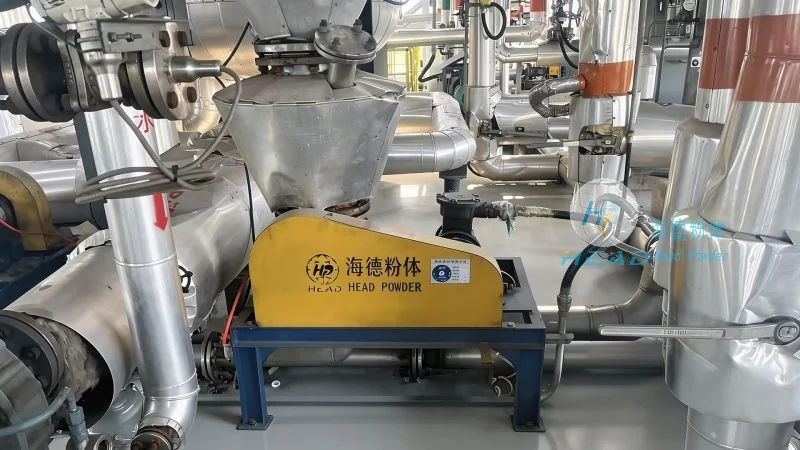
The intelligent centralized powder material handling system offers several advantages over traditional manual or semi-automated powder handling methods. Firstly, it significantly improves the efficiency of powder material handling by automating the entire process, reducing labor costs and human error. Secondly, the system ensures stable and reliable material flow, minimizing material loss and contamination, which is crucial for maintaining product quality in industrial production. Thirdly, the intelligent monitoring and control capabilities of the system provide real-time data on material inventory, conveying status, and equipment performance, enabling better decision-making and process optimization. The system is widely applied in various industries, including chemical, pharmaceutical, food, and cement, where bulk powder materials are involved. For instance, in the chemical industry, the system is used to handle raw materials like powders and granules for chemical synthesis processes. In the pharmaceutical industry, it ensures the safe and hygienic handling of active pharmaceutical ingredients (APIs) and excipients. In the food industry, it is used to handle food powders such as flour, sugar, and protein powders, maintaining product freshness and quality. In the cement industry, it facilitates the efficient transport of cement raw materials and finished products, improving production efficiency and reducing energy consumption.