

What is a Dry Slurry Pneumatic Conveying System? And What Are Its Design Principles?
A dry slurry pneumatic conveying system is a specialized industrial equipment used for transporting dry powders and granular materials in a slurry form through a pipeline using compressed air or other gas as the conveying medium. This technology is widely applied in various industries such as chemical, food, pharmaceutical, and mining, where the efficient and safe transfer of bulk materials is crucial. The system combines the advantages of pneumatic conveying with the characteristics of slurry, offering a flexible and reliable solution for material handling.
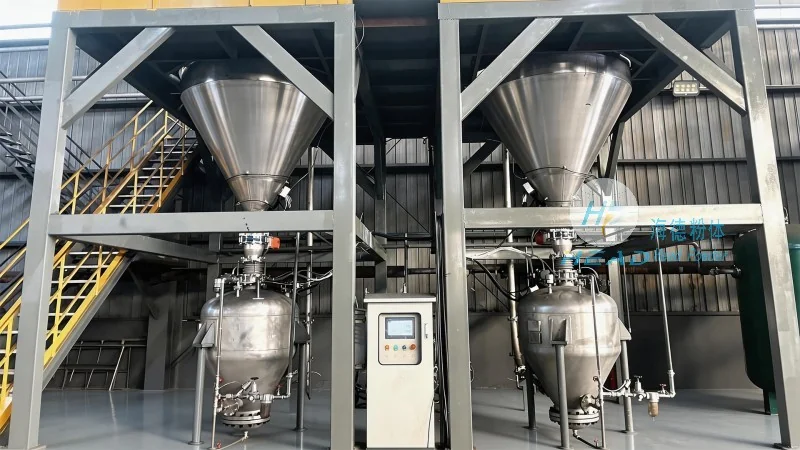
Core Components and Working Principle
The fundamental components of a dry slurry pneumatic conveying system typically include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, a compressor or blower to generate the conveying air, and a receiver for the discharged material. The working principle involves feeding the dry powder or granules into the hopper, where they are mixed with a small amount of liquid to form a slurry. The feeder then introduces the slurry into the pipeline, and the compressor provides the necessary pressure to move the slurry through the pipeline to the receiving hopper. The air pressure and flow rate are carefully controlled to ensure the material is conveyed smoothly without clogging or degradation.
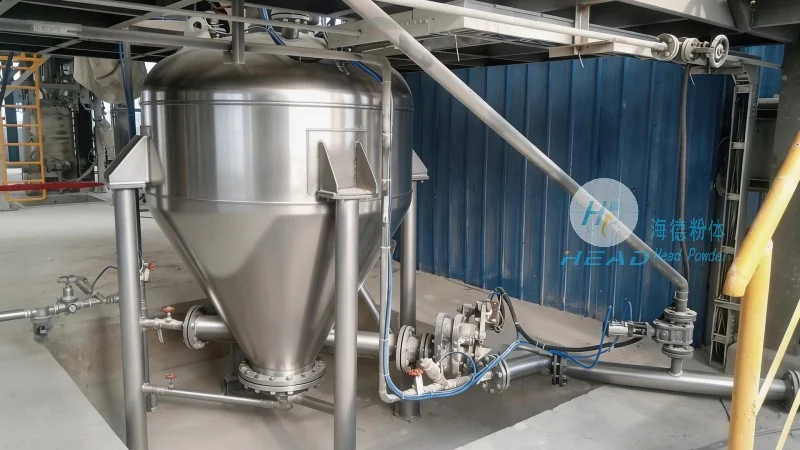
Key Design Principles and Considerations
Designing an effective dry slurry pneumatic conveying system requires careful consideration of several key factors. First, the material properties, including particle size, density, moisture content, and flowability, significantly influence the system's performance. The system must be designed to handle the specific characteristics of the dry slurry, ensuring that the conveying velocity and pressure are optimized to prevent particle segregation or agglomeration. Second, the pipeline layout and diameter are critical. The diameter must be large enough to accommodate the slurry flow without excessive pressure drop, while the length and bends should be minimized to reduce energy consumption and maintain system efficiency. Third, the selection of the compressor or blower is essential. It must provide sufficient air volume and pressure to overcome the system's resistance, including friction losses in the pipeline and the pressure drop across components like valves and filters. Additionally, the system should incorporate features such as air separation and liquid recovery to maintain material purity and reduce waste.
Advantages and Applications
Dry slurry pneumatic conveying systems offer several advantages over traditional conveying methods. They provide a closed system, which helps to prevent dust contamination and environmental pollution, making them suitable for industries with strict hygiene and safety requirements. The system is also flexible, as it can transport materials over long distances and through multiple bends without the need for additional equipment like conveyors or elevators. Furthermore, it can handle a wide range of materials, from fine powders to coarse granules, and can be adapted to different production scales. The applications of this technology are diverse, including the transportation of dry slurry in chemical plants for raw material handling, in food processing facilities for ingredient transfer, in pharmaceutical manufacturing for drug powder movement, and in mining operations for ore and tailings transport.
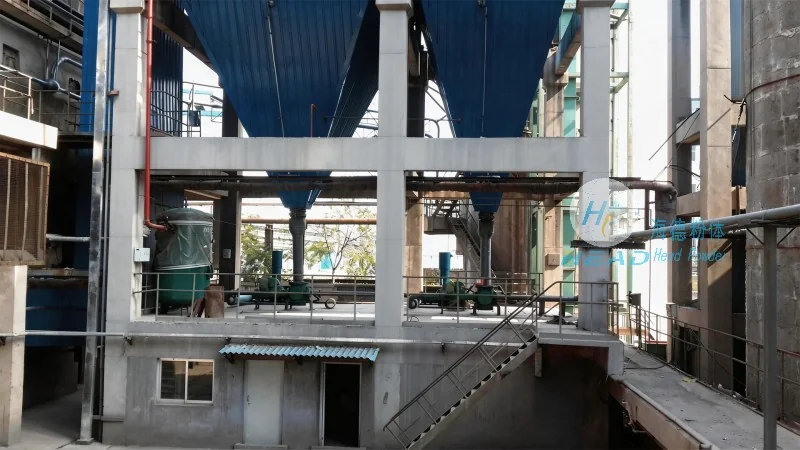
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including dry slurry pneumatic conveying equipment. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the material handling industry. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians dedicated to developing advanced conveying solutions tailored to the specific needs of clients. HeadPowder's products are designed to meet international standards and are known for their reliability, efficiency, and durability. The company provides comprehensive services, including system design, manufacturing, installation, and after-sales support, ensuring that clients receive a complete solution for their material handling challenges.