

Operation Process and Working Principle of Barley Pneumatic Conveying
Barley pneumatic conveying systems are sophisticated industrial solutions designed to efficiently transport barley grains and other bulk materials over short to medium distances. These systems are widely used in the agricultural and food processing industries due to their ability to handle delicate products while maintaining high throughput and minimal product degradation. The operation process and working principle of such systems involve several key components and steps that work in tandem to ensure reliable and efficient material handling.
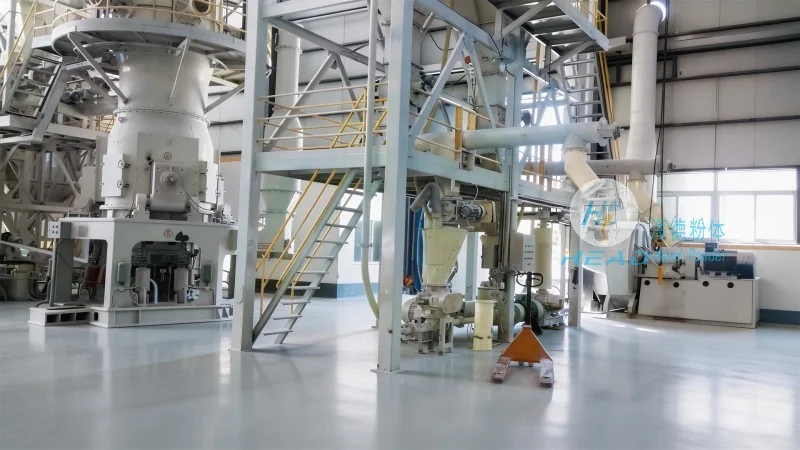
Key Components of Barley Pneumatic Conveying Systems
At the core of a barley pneumatic conveying system are several essential components that work together to facilitate the movement of barley. These components typically include a hopper or storage silo for material storage, a conveying line (often made of metal or flexible tubing), a fan or blower to generate the necessary air pressure, a separator or cyclone to separate the material from the air stream, and a discharge point for the material. The hopper is designed to hold the barley, ensuring a consistent feed rate into the system. The conveying line transports the barley particles along with the air stream, while the fan provides the kinetic energy needed to move the material. The separator then separates the barley from the air, allowing the air to be recirculated or discharged, and the material to be collected at the discharge point.
The Operation Process of Barley Pneumatic Conveying
The operation process of a barley pneumatic conveying system begins with the loading of barley into the hopper. Once the hopper is filled, the fan is activated, creating a low-pressure zone within the conveying line. As the fan operates, it draws air from the hopper and the surrounding environment, and this air is then mixed with the barley particles. The combined air and material stream moves through the conveying line at high velocity, propelled by the fan's output. The material travels to the separator, where centrifugal force or other separation mechanisms separate the barley from the air. The separated barley is then discharged into a collection bin or storage area, while the air is either filtered and recirculated back into the system or released to the atmosphere. This process is continuous as long as the hopper is supplied with barley and the fan remains operational, ensuring a steady flow of material.
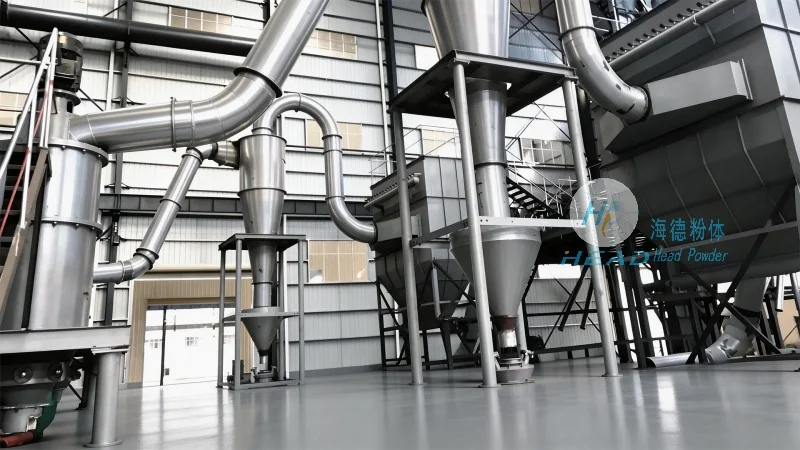
Working Principle of Barley Pneumatic Conveying
The working principle of barley pneumatic conveying is based on the principles of fluid dynamics and particle transport. The system operates by creating a pressure differential between the hopper and the discharge point. The fan generates a negative pressure (or positive pressure, depending on the system design) that pulls the air and barley particles into the conveying line. The air acts as a carrier medium, suspending the barley particles and moving them along the line. The velocity of the air stream is critical; it must be sufficient to keep the barley particles in suspension and overcome any resistance in the conveying line, such as bends or changes in direction. The separator plays a crucial role by using centrifugal force to separate the heavier barley particles from the lighter air stream. This separation is achieved by directing the mixed air and material into a cyclone or other separator, where the particles are forced to the outer wall due to their higher mass, and the air exits through the center. The separated barley is then collected, while the air is either filtered to remove any residual particles or recirculated to improve energy efficiency.
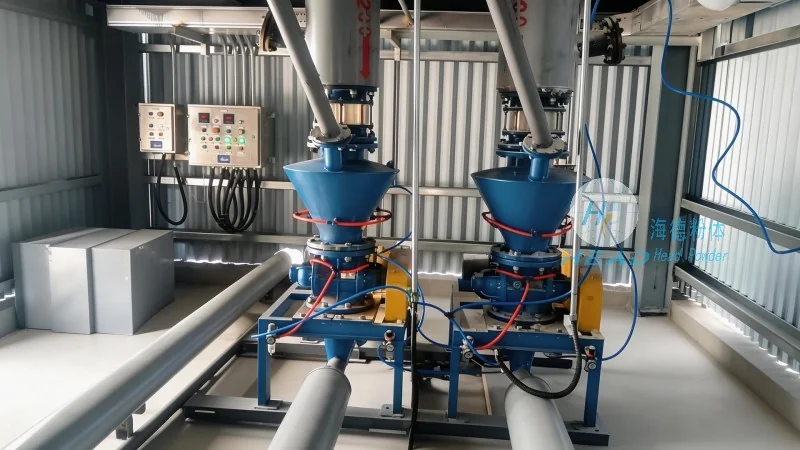
Advantages of Using Barley Pneumatic Conveying Systems
Barley pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. One of the primary benefits is the ability to handle delicate barley grains without causing damage, as the air stream suspends the particles gently. This reduces the risk of breakage or bruising, which is particularly important for maintaining the quality of the grain for brewing or other applications. Additionally, pneumatic conveying systems can operate in a closed environment, minimizing dust emissions and improving workplace safety. The systems are also relatively compact and can be easily integrated into existing production lines, making them suitable for both new installations and retrofitting in existing facilities. Furthermore, the continuous operation of these systems allows for high throughput, which is essential for meeting the demands of modern agricultural and food processing operations. The energy efficiency of modern fans and separators also contributes to lower operational costs over time.
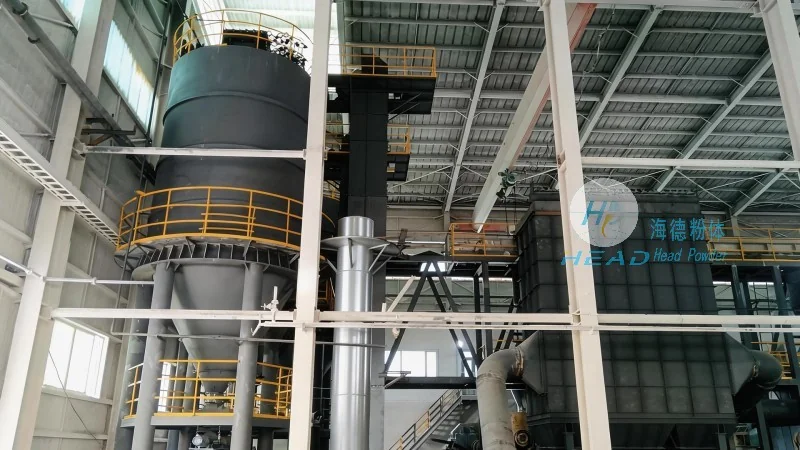
Applications and Industries Using Barley Pneumatic Conveying
Barley pneumatic conveying systems are widely used in various industries that handle barley and other bulk agricultural products. The most common applications include the brewing industry, where barley is used as a key ingredient in beer production. In breweries, these systems are used to transport barley from storage silos to milling and malting equipment. Other industries that benefit from barley pneumatic conveying include feed mills, where barley is used as an ingredient in animal feed, and grain processing facilities, where barley is processed into flour or other products. The systems are also used in research and development facilities for testing new processing methods or improving existing ones. Regardless of the industry, the consistent and efficient transport of barley is crucial for maintaining product quality and operational efficiency.
Conclusion and Company Information
Barley pneumatic conveying systems are essential tools for the efficient and reliable handling of barley in various industrial applications. By understanding the operation process and working principle of these systems, businesses can optimize their material handling processes and improve overall productivity. Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for the agricultural and food processing industries, specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of their clients. With a focus on innovation and customer satisfaction, HeadPowder ensures that their systems meet the highest standards of performance and durability. Located in Shandong, China, HeadPowder leverages its expertise and local resources to deliver reliable solutions that enhance the efficiency of barley processing operations worldwide.