

Principle and Working Scene Characteristics of Automatic Weighing Material Conveying Systems
Automatic weighing material conveying systems represent a sophisticated integration of weighing technology and material handling, designed to enhance efficiency and accuracy in industrial processes. These systems are engineered to handle the transport of bulk materials while simultaneously measuring their weight, providing real-time data for quality control, inventory management, and operational optimization. The core principle revolves around the seamless combination of conveyor mechanisms with precision load cells or scales, ensuring that materials are not only moved efficiently but also weighed accurately at various stages of the production or processing workflow.
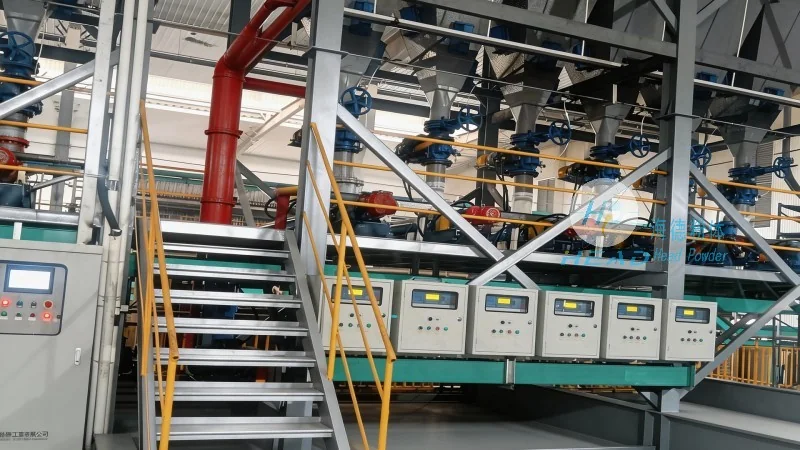
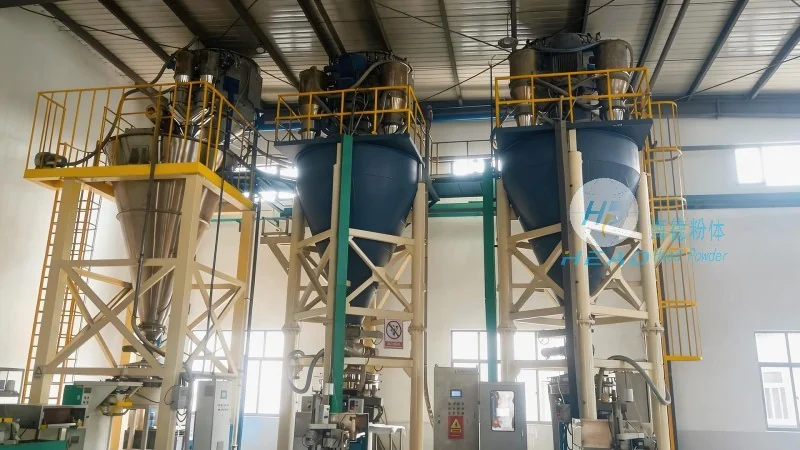
Key Working Principles of the System
The fundamental operation of an automatic weighing material conveying system is built upon several critical principles. First, the system utilizes a conveyor belt or other transport mechanisms to move materials from one location to another. Simultaneously, integrated load cells or weighing sensors are positioned along the conveyor path to capture the weight of the material as it passes. This dual functionality allows for continuous or batch weighing, depending on the system configuration. The weighing data is then processed by a control unit, which may interface with a central system or provide local feedback. Additionally, the system often incorporates features such as automatic batching, where the conveyor stops or adjusts speed based on the target weight, ensuring precise portioning of materials. This integration of transport and weighing minimizes manual intervention, reduces human error, and enhances overall operational consistency.
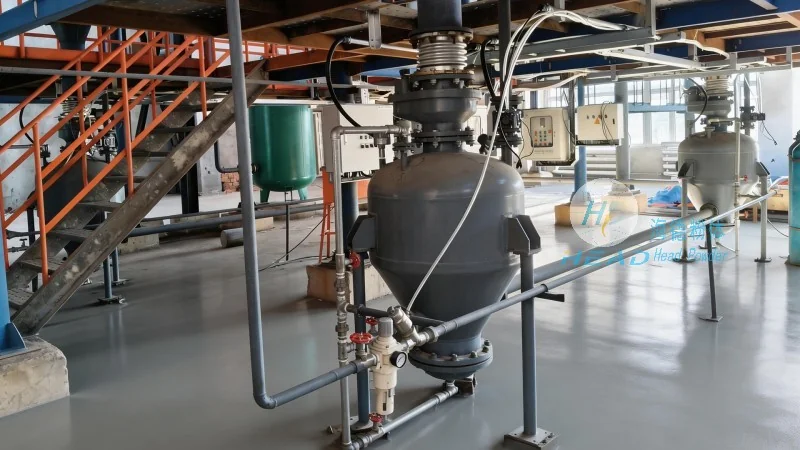
Common Working Scene Characteristics
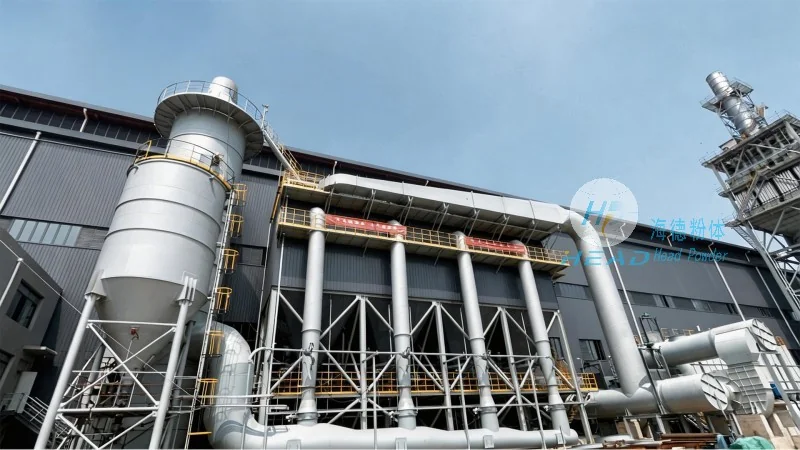
The application of automatic weighing material conveying systems spans a wide range of industrial scenarios, each with distinct characteristics that highlight the system's adaptability. In manufacturing facilities, these systems are commonly used in raw material intake and intermediate product handling, where accurate weight measurement is crucial for maintaining production standards. For example, in the chemical or food processing industries, precise weighing ensures compliance with regulatory requirements and product specifications. In mining and mineral processing, the systems aid in the efficient transport and weighing of ore or raw minerals, optimizing the extraction and processing workflow. Additionally, in logistics and warehousing, the systems can be employed for inventory management, enabling real-time tracking of material quantities and facilitating inventory audits. The working scene characteristics also include the need for robust construction to withstand harsh industrial environments, with features like dust-proofing, corrosion resistance, and easy maintenance to ensure long-term reliability. Furthermore, the systems are often designed to be scalable, allowing for integration with existing production lines or expansion as operational needs grow.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of industrial automation solutions, specializing in the design, manufacturing, and implementation of advanced material handling and weighing systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in various industries, including chemical, food processing, mining, and logistics. HeadPowder's expertise lies in developing customized solutions that meet the unique requirements of each client, ensuring optimal performance and reliability. The company's headquarters is located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services. By focusing on customer needs and technological advancement, headpowder continues to enhance industrial efficiency and contribute to the growth of its clients' operations.