

Principles and Working Scene Characteristics of Intelligent Ingredient Material Conveying Systems
Intelligent ingredient material conveying systems represent a pivotal advancement in modern industrial processing, offering enhanced efficiency, precision, and adaptability for material handling tasks. These systems are designed to streamline the movement of various ingredients and materials within production environments, ensuring optimal performance and reliability. This article explores the fundamental principles underlying such systems and highlights the key characteristics that define their operational effectiveness in diverse industrial settings.
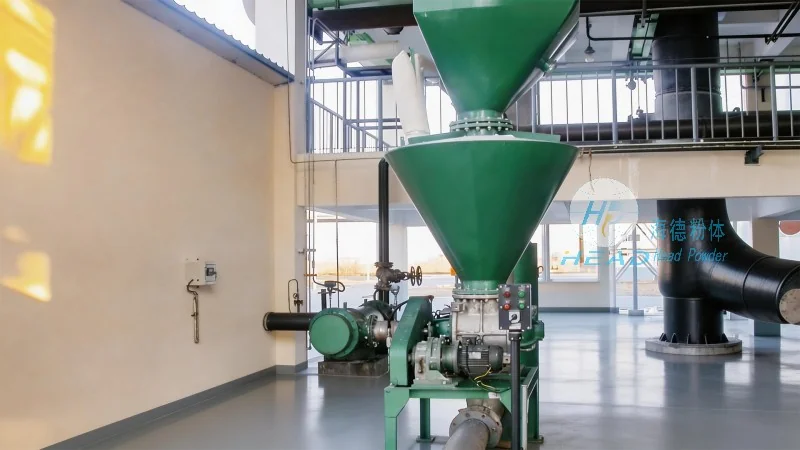
Core Principles of the Conveying System
The intelligent ingredient material conveying system operates on several core principles that enable seamless material transport. At its foundation is a modular design that allows for flexibility in configuration, accommodating different material types, sizes, and processing requirements. The system integrates advanced sensors and control technologies to monitor and adjust the conveying process in real-time, ensuring precise control over material flow rates and positioning. Additionally, automation features, such as programmable logic controllers (PLCs) and artificial intelligence (AI) algorithms, enhance the system's ability to adapt to changing operational conditions, reducing downtime and improving overall productivity. The integration of these principles ensures that the system can handle a wide range of ingredients, from powders and granules to bulk materials, with consistent accuracy and reliability. For instance, in pharmaceutical applications, the system's ability to maintain sterile conditions and prevent cross-contamination is critical, making it an essential component of cleanroom environments. Similarly, in food processing facilities, the system's hygienic design and easy-to-clean features ensure compliance with food safety regulations, while its precise dosing capabilities support consistent product quality. In chemical manufacturing, the system's robust construction and ability to handle corrosive or abrasive materials make it suitable for demanding applications. Each working scene presents unique challenges, and the intelligent conveying system addresses these through tailored features, such as adjustable speed controls, material separation mechanisms, and safety interlocks, ensuring optimal performance in diverse operational contexts.
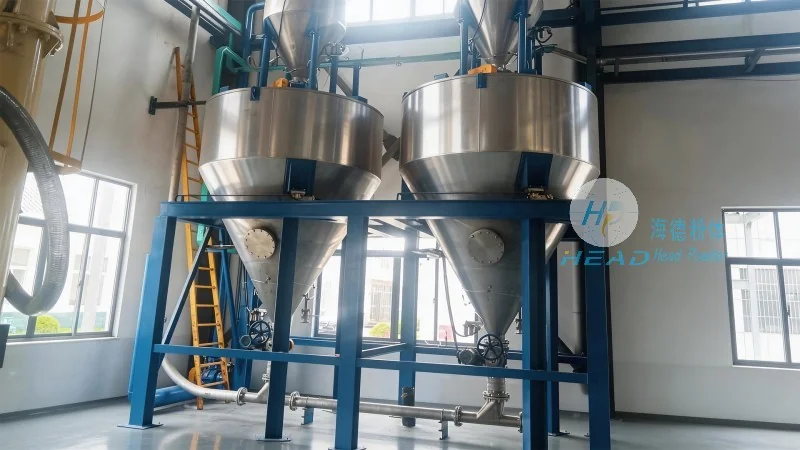
Key Working Scene Characteristics
The effectiveness of intelligent ingredient material conveying systems is significantly influenced by their application in specific working scenes. These systems are commonly employed in industries like pharmaceuticals, food processing, and chemical manufacturing, where the handling of sensitive or high-value materials demands strict control over contamination and loss. In pharmaceutical production, the system's ability to maintain sterile conditions and prevent cross-contamination is critical, making it an essential component of cleanroom environments. The system's modular design allows for easy integration into existing production lines, minimizing disruption during installation. Furthermore, its real-time monitoring capabilities enable operators to track material flow and identify potential issues promptly, enhancing overall process control. In food processing, the system's hygienic features, including smooth surfaces and easy-to-clean components, are crucial for maintaining food safety standards. The precise dosing functionality ensures that ingredients are added in exact proportions, contributing to consistent product quality and reducing waste. In chemical manufacturing, the system's durability and resistance to corrosion and abrasion are key advantages, as it can handle harsh materials without compromising performance. The integration of safety features, such as emergency stop buttons and overload protection, further enhances operational safety in these demanding environments. Overall, the working scene characteristics of intelligent ingredient material conveying systems are tailored to meet the specific needs of each industry, ensuring that the system delivers optimal performance and reliability.
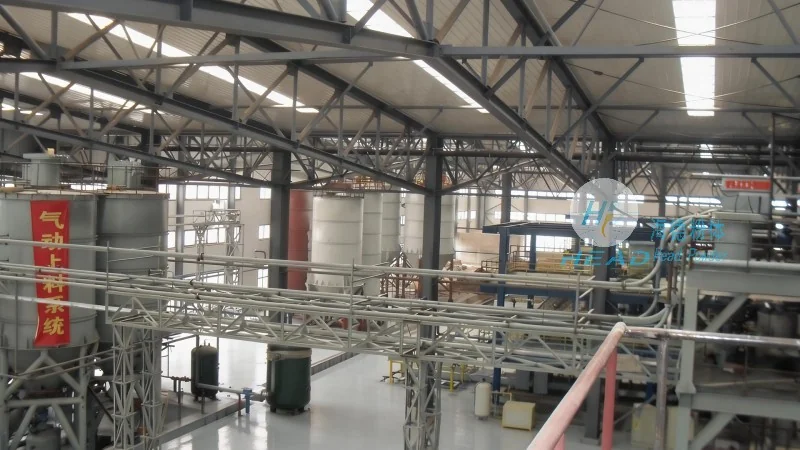
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of industrial conveying solutions, specializes in the design, manufacturing, and implementation of intelligent ingredient material conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's systems are engineered to meet the specific needs of clients, offering customized solutions that enhance operational efficiency and reduce costs. The company's headquarters is located in Shandong, China, where its team of experts leverages years of experience to develop cutting-edge technologies that address the evolving demands of modern manufacturing. By focusing on quality and reliability, HeadPowder ensures that its conveying systems deliver consistent performance, contributing to the success of its clients' production processes. The company's modular and adaptable designs allow for seamless integration into various production environments, supporting the diverse requirements of different industries. HeadPowder's dedication to customer service and technical support ensures that clients receive comprehensive assistance throughout the system's lifecycle, from installation to maintenance. This approach has earned HeadPowder a reputation for excellence in the field, making it a preferred choice for businesses seeking reliable and efficient material conveying solutions.