

Principles and Working Scene Characteristics of Feather Powder Material Handling
Feather powder material handling represents a specialized area within industrial material transport, particularly relevant for sectors dealing with lightweight, fine powders derived from feather processing. The underlying principles of this technology are tailored to address the unique challenges posed by feather powders, such as their low bulk density, propensity to agglomerate, and susceptibility to static charge. Mastery of these principles is essential for optimizing operational efficiency and safety in material handling processes across diverse industrial environments.
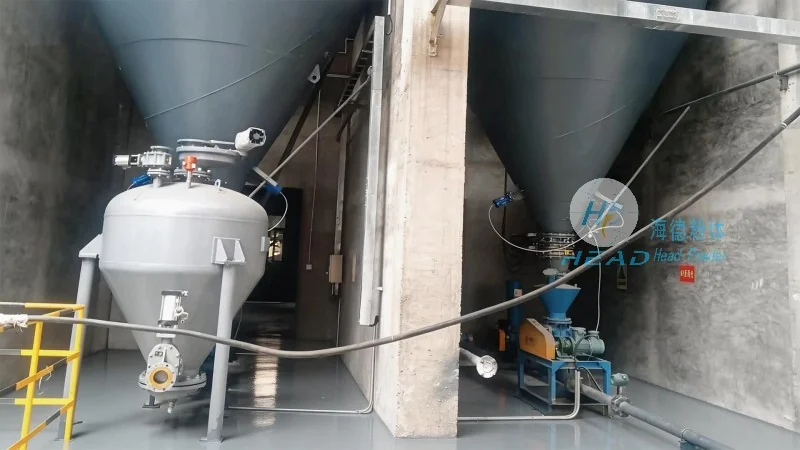
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading enterprise in powder engineering, specializes in the design, manufacturing, and implementation of advanced material handling systems. With a focus on innovation and customer-centric solutions, the company has positioned itself as a trusted partner for businesses requiring reliable and efficient powder transport solutions. HeadPowder operates from Shandong, China, leveraging local expertise and resources to deliver high-quality products and services tailored to the specific needs of its clients.
Core Principles of Feather Powder Conveying
The fundamental principles of feather powder material handling revolve around optimizing flow characteristics, preventing material degradation, and ensuring operational safety. Key principles include: 1) Maintaining consistent air flow and pressure to prevent powder settling or blockages in the conveying system; 2) Utilizing appropriate equipment such as rotary valves, air locks, and dust collectors to manage the material's low bulk density and prevent clogging; 3) Implementing electrostatic discharge measures to mitigate fire or explosion risks in environments where feather powders are handled; 4) Employing gentle handling techniques to avoid agglomeration and preserve the powder's quality and consistency. These principles are integral to the design and operation of efficient feather powder conveying systems.
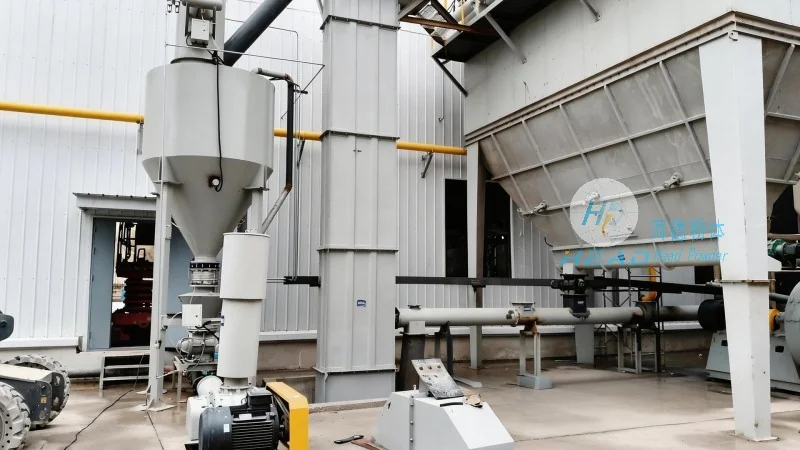
Working Scene Characteristics and Application Scenarios
The working scene characteristics of feather powder material handling vary significantly based on the specific industry and processing requirements. For instance, in the poultry processing industry, feather powders are often used as feed additives or in the production of feather meal. The material handling systems in this sector must be capable of handling large volumes of fine powders while maintaining hygiene standards and preventing cross-contamination. In the cosmetics and pharmaceutical industries, feather powders may be used as natural ingredients, requiring even stricter control over particle size, purity, and contamination levels. The working scene characteristics also include considerations such as space constraints, environmental regulations, and the need for dust control measures to ensure compliance with occupational health and safety standards.
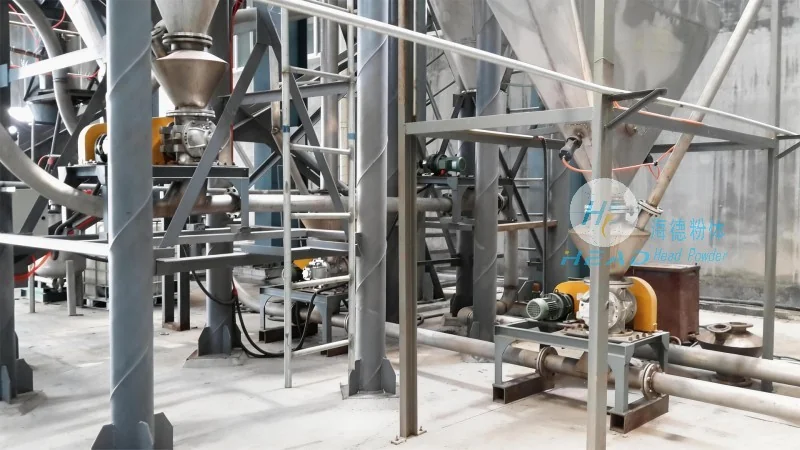
System Components and Operational Efficiency
Efficient feather powder conveying systems typically consist of several key components, each playing a critical role in the overall operation. These components include: 1) Hopper and feeding mechanisms to control the flow of powder into the conveying line; 2) Conveying pipes and ducts designed to handle the specific properties of feather powders, often incorporating smooth surfaces and appropriate diameters to minimize friction and blockage; 3) Air supply systems, such as positive displacement blowers or rotary lobe pumps, to generate the necessary air pressure for material transport; 4) Dust collection and filtration systems to capture fine particles and ensure clean air discharge; 5) Control panels and monitoring systems to regulate the operation and provide real-time feedback on system performance. The integration of these components, along with adherence to the core principles of feather powder handling, ensures high operational efficiency and reliability in various industrial applications.
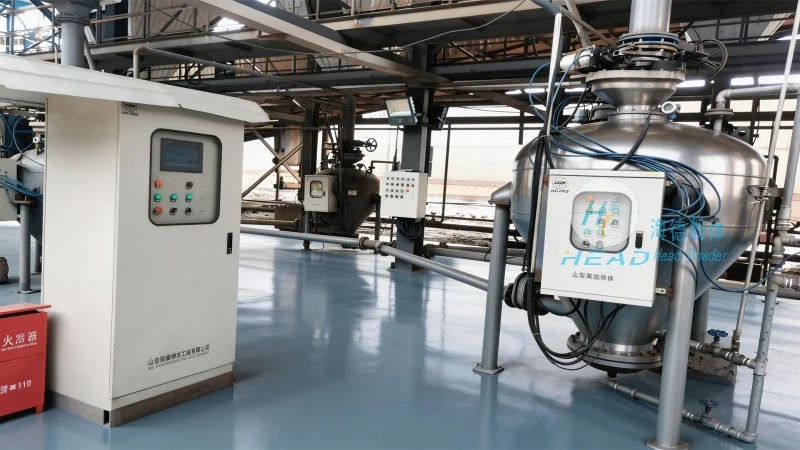
Case Studies and Real-World Applications
HeadPowder has successfully implemented feather powder conveying systems in a range of industrial applications, demonstrating the practical application of its core principles. For example, in a poultry processing facility, the company designed a customized system that handles large volumes of feather meal, ensuring consistent flow and preventing material degradation during transport. The system incorporated advanced dust collection technology to maintain a clean working environment and comply with environmental regulations. In another case, a cosmetics manufacturer utilized HeadPowder's solutions to transport feather-derived natural ingredients, achieving precise control over particle size and maintaining product quality throughout the process. These case studies highlight the effectiveness of HeadPowder's approach to feather powder material handling and its ability to address the unique challenges faced by different industries.
Future Trends and Continuous Improvement
As industries continue to evolve, the demand for efficient and sustainable material handling solutions for feather powders is expected to grow. HeadPowder remains committed to innovation, continuously researching and developing new technologies to enhance the performance of its systems. This includes exploring advanced materials for conveying components, improving energy efficiency, and integrating smart monitoring systems to optimize operational performance. By staying at the forefront of technological advancements, HeadPowder aims to provide its clients with cutting-edge solutions that meet the evolving needs of the market while adhering to the highest standards of quality and safety.