

Efficient Pneumatic Conveying Systems for Inorganic Salt Crystal Transportation
HeadPowder, a leading provider of specialized engineering solutions, specializes in developing and implementing efficient pneumatic conveying systems tailored to the unique challenges of transporting inorganic salt crystals. The company, based in Shandong, China, leverages advanced technology and expertise to address the complexities associated with handling such materials, ensuring reliable and effective material transport in industrial applications.
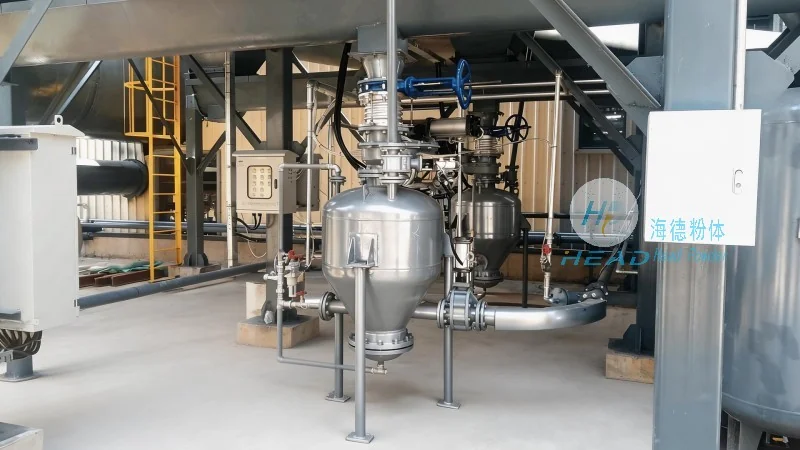
The Unique Challenges of Inorganic Salt Crystal Transportation
Inorganic salt crystals, such as those used in chemical and food processing industries, present distinct challenges during transportation. These challenges include the need for gentle handling to prevent product degradation, the prevention of dust generation, and the efficient management of material flow in varying conditions. Traditional methods like belt conveyors or bucket elevators may struggle with these requirements, leading to inefficiencies and increased operational costs. Pneumatic conveying systems offer a superior alternative by utilizing air to move materials in a controlled manner, minimizing physical contact and reducing the risk of contamination.
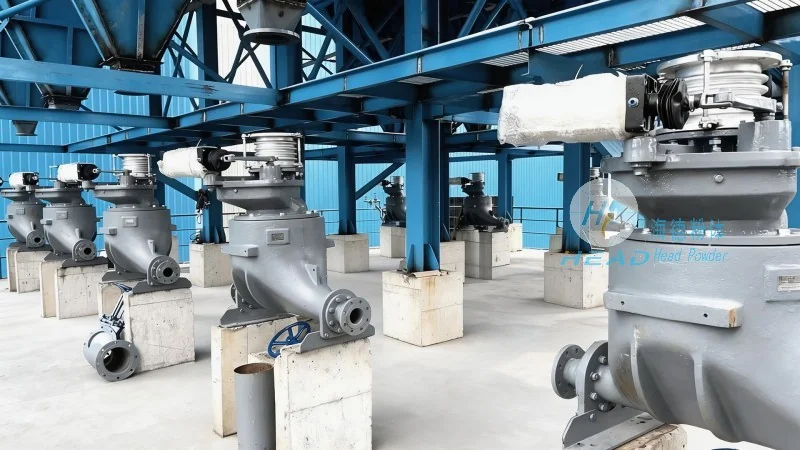
How Pneumatic Conveying Systems Address These Challenges
HeadPowder's pneumatic conveying systems are specifically designed to overcome the challenges of inorganic salt crystal transportation. The systems employ positive or negative pressure air flow to transport materials through pipelines, ensuring a gentle and consistent flow. This approach effectively prevents product breakage and maintains the integrity of the crystals, which is crucial for applications where product quality is paramount. Additionally, the enclosed system design minimizes dust exposure, enhancing workplace safety and compliance with environmental regulations. The technology also allows for flexible system configurations, enabling integration with existing industrial setups or new plant designs. For instance, positive pressure systems are ideal for long-distance transport, while negative pressure systems are suitable for handling fine powders and preventing product loss.
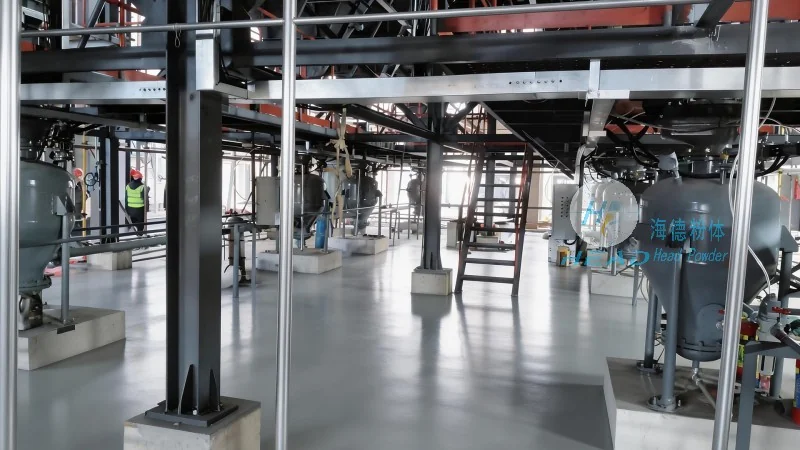
Key Features and Benefits of HeadPowder's Pneumatic Conveying Solutions
HeadPowder's pneumatic conveying systems are equipped with several key features that enhance performance and reliability. These include adjustable air pressure controls to optimize material flow rates, high-efficiency filtration systems to maintain air quality, and robust pipeline materials resistant to corrosion and abrasion from salt crystals. The systems are designed for low maintenance, reducing downtime and operational expenses. Furthermore, the modular design allows for easy expansion or modification as production needs evolve. The benefits of these solutions extend beyond operational efficiency, including improved product quality, reduced environmental impact, and enhanced safety for personnel handling the materials.
Application Examples and Industry Impact
The effectiveness of HeadPowder's pneumatic conveying systems is demonstrated in various industrial applications. In the chemical industry, the systems are used to transport sodium chloride, potassium chloride, and other salts, ensuring smooth integration into production lines. In food processing, the gentle handling of salt crystals prevents clumping and maintains product freshness, which is critical for consumer safety and brand reputation. The systems have also been successfully implemented in pharmaceutical and agricultural sectors, where the purity and integrity of inorganic salts are essential. By addressing the specific needs of each industry, HeadPowder's solutions contribute to increased productivity and cost savings for its clients.
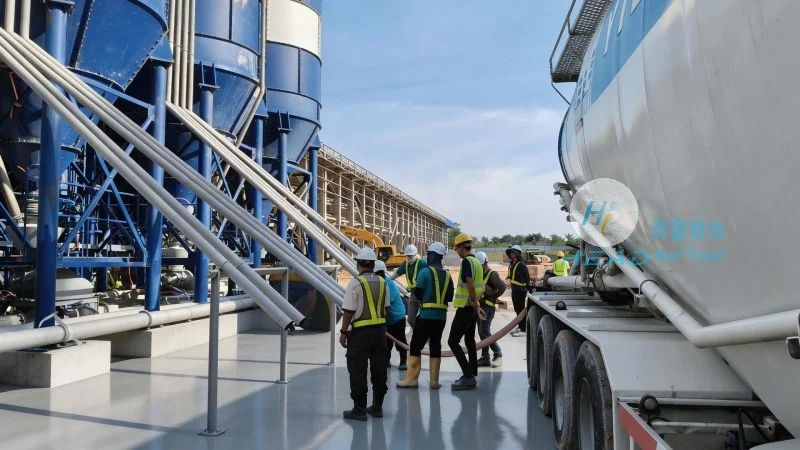
Conclusion and Company Commitment
HeadPowder Engineering Co., Ltd., based in Shandong, China, remains committed to providing innovative and reliable pneumatic conveying solutions for the transportation of inorganic salt crystals. The company's expertise in engineering and material handling ensures that each system is tailored to meet the unique requirements of its clients, delivering sustainable and efficient operations. With a focus on quality, safety, and customer satisfaction, HeadPowder continues to be a trusted partner in the industrial sector, helping businesses overcome the challenges of material transport and achieve their operational goals.