

Principle and Working Scene Characteristics of Fine Coal Powder Pneumatic Conveying Systems
For industrial applications involving the transport of fine coal powder, pneumatic conveying systems represent a sophisticated and efficient solution. These systems leverage the principles of fluid dynamics to move particulate materials through a network of pipes using pressurized air or gas. Understanding the underlying mechanics and the diverse operational environments where such systems are deployed is crucial for optimizing performance and ensuring reliability in material handling processes.
Principle of Fine Coal Powder Pneumatic Conveying Systems
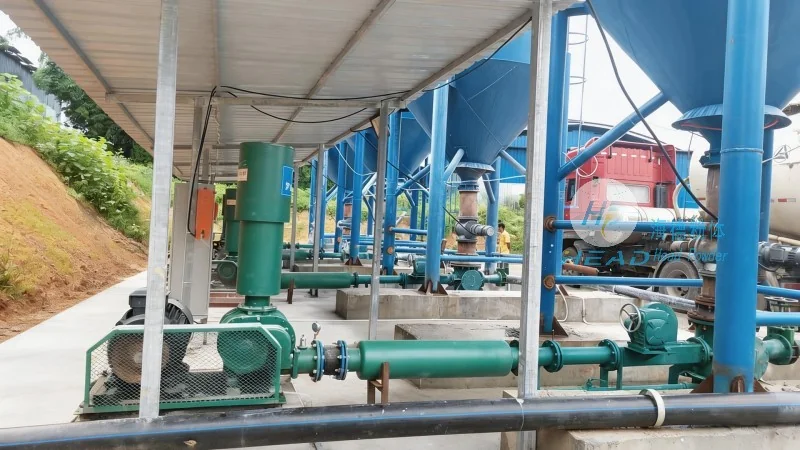
The core principle of fine coal powder pneumatic conveying systems revolves around the interaction between solid particles and a moving gas stream. In a typical setup, fine coal powder is introduced into a pressurized air stream within a pipeline. The air, moving at sufficient velocity, entrains the coal particles, carrying them through the system. This process relies on the balance between the drag force exerted by the air on the particles and the gravitational force pulling them downward. The system can operate in either positive pressure or negative pressure modes, with positive pressure systems being more common for fine coal powder due to their ability to handle high concentrations of particles and maintain consistent flow rates.
Key components of the system include the hopper for material storage, the conveyor pipeline, the air compressor or blower for generating the pressurized air, and the control valves that regulate the flow. The design of the hopper and the inlet of the pipeline is critical to prevent particle segregation and ensure uniform feeding. The pipeline diameter and length are carefully selected based on the particle size distribution, flow rate requirements, and the desired pressure drop across the system. The air compressor must provide enough pressure to overcome the resistance from the pipeline and the weight of the coal particles, while maintaining energy efficiency.
Working Scene Characteristics of Fine Coal Powder Pneumatic Conveying Systems
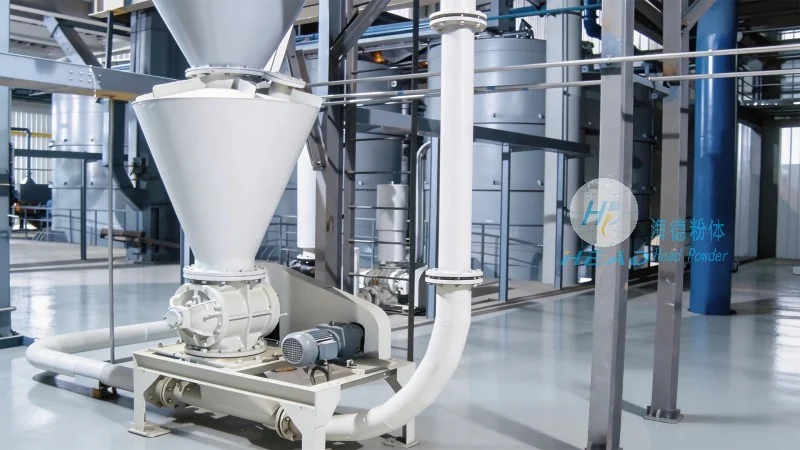
Fine coal powder pneumatic conveying systems are widely utilized across various industrial sectors, each presenting unique characteristics that influence system design and operation. In power plants, these systems are essential for transporting coal from storage silos to boilers, where consistent and reliable fuel supply is vital for efficient combustion. The high concentration of fine coal particles in these applications requires robust pipeline materials and precise control mechanisms to prevent blockages and ensure smooth operation.
In coal processing facilities, such as preparation plants, pneumatic conveying systems are used to move coal from grinding mills to classifiers and then to storage bins. The fine particle size and the need for minimal material loss make the system's efficiency and cleanliness paramount. Here, the working scene involves continuous operation with high throughput, demanding systems that can handle abrasive particles without excessive wear and tear.
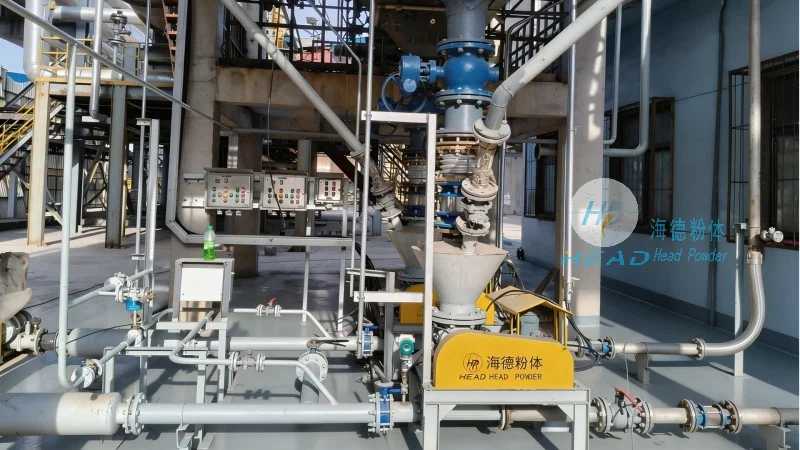
In the chemical and metallurgical industries, fine coal powder may be used as a raw material or a reagent, and pneumatic conveying systems facilitate its transport from storage to processing units. The working environment in these sectors often involves higher temperatures and more corrosive conditions, necessitating materials like stainless steel or special coatings for the pipeline and components to ensure durability and prevent contamination.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for the transportation of fine coal powder and other particulate materials. With a focus on engineering excellence and customer-centric solutions, the company leverages years of industry experience to deliver systems that meet the specific requirements of diverse industrial applications. HeadPowder's expertise in material handling technology ensures that their systems are not only efficient and reliable but also adaptable to the unique challenges posed by different working environments.
The company's commitment to quality and innovation is reflected in its use of cutting-edge technologies and rigorous testing protocols. By collaborating closely with clients to understand their operational needs and material characteristics, HeadPowder provides customized solutions that enhance productivity, reduce downtime, and minimize operational costs. Based in Shandong, China, the company serves a global market, delivering systems that are built to withstand the demands of industrial environments while maintaining compliance with international standards for safety and performance.