

Principle and Working Scene Characteristics of High-Temperature Ash Pneumatic Conveying Systems
High-temperature ash pneumatic conveying systems are integral to modern industrial operations, particularly in power generation and waste management sectors. These systems are engineered to transport hot ash, typically generated from coal-fired boilers or other combustion processes, from the source to a designated storage or processing location. The technology leverages pneumatic principles to move bulk materials through pipelines using air or gas, offering a flexible and efficient alternative to traditional mechanical conveyors. Understanding the core principles and operational characteristics of these systems is crucial for optimizing performance, ensuring safety, and maintaining operational efficiency in high-temperature material handling applications.
The Fundamental Principle of Pneumatic Conveying for High-Temperature Ash
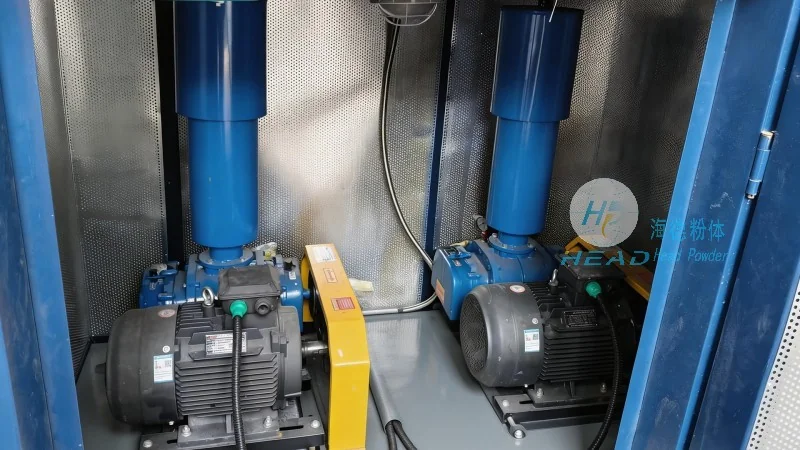
The core principle of pneumatic conveying involves the use of air pressure to transport solid particles through a pipeline. In high-temperature ash applications, the system must be designed to withstand extreme temperatures, often ranging from 400°C to 800°C, while effectively conveying abrasive and potentially corrosive ash materials. The process typically operates under positive or negative pressure conditions, where air is either blown (positive pressure) or sucked (negative pressure) to move the ash particles. Key components of the system include ash feeders, conveying pipelines, dust collectors, and control systems that regulate air flow and pressure to maintain consistent material transport. The ash feeders are designed to handle the high-temperature feed, ensuring a steady supply of material into the conveying line. The pipelines are constructed from high-temperature-resistant materials, such as stainless steel or specialized alloys, to prevent degradation under extreme conditions. Dust collectors are integrated to capture any airborne particles, ensuring compliance with environmental regulations and maintaining air quality in the operational environment.
Working Scene Characteristics and Typical Application Scenarios
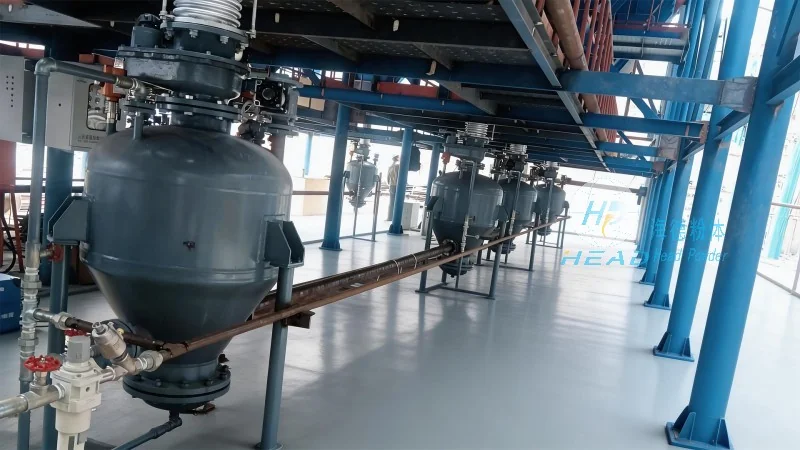
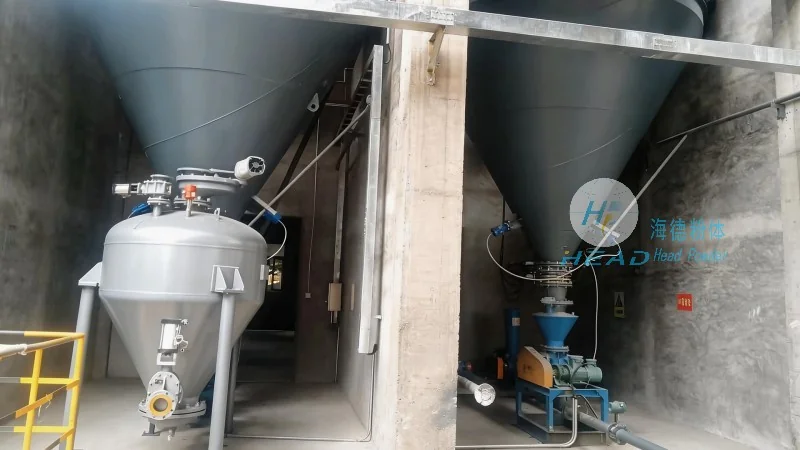
High-temperature ash pneumatic conveying systems are deployed in diverse industrial settings, each with unique operational requirements. In thermal power plants, these systems are commonly used to transport fly ash from boiler hoppers to storage silos or for further use in cement production. The working scene characteristics include continuous operation, high ambient temperatures, and the need for reliable, low-maintenance equipment capable of handling abrasive ash particles without excessive wear. Additionally, the systems must be designed to minimize emissions and comply with environmental standards, ensuring that the conveying process does not contribute to air pollution. Other applications may include industrial incinerators, where ash is generated from waste processing, or in cement plants that utilize ash as a raw material for clinker production. In each scenario, the system's design must accommodate the specific temperature, particle size, and flow rate of the ash material to ensure optimal performance.
Key Features and Advantages of High-Temperature Ash Pneumatic Conveying Systems
HeadPowder, a leading manufacturer of pneumatic conveying solutions, offers advanced high-temperature ash pneumatic conveying systems that incorporate several key features. These systems are constructed using high-temperature-resistant materials, such as 304 or 316 stainless steel, and specialized alloys to withstand extreme operating temperatures. The design includes efficient ash feed mechanisms that ensure consistent material flow, reducing the risk of blockages or uneven transport. Additionally, the systems are equipped with advanced control systems that monitor air pressure, temperature, and material flow in real-time, allowing for immediate adjustments to maintain optimal performance. The advantages of these systems include reduced labor costs due to automated operation, lower maintenance requirements compared to traditional mechanical conveyors, and improved safety by eliminating the need for manual handling of hot ash. Furthermore, the systems are designed to be energy-efficient, minimizing operational costs while maximizing throughput. HeadPowder's expertise in customizing systems to meet specific client needs ensures that each solution is tailored to the unique challenges of the application, providing a reliable and efficient solution for high-temperature ash transport.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in pneumatic conveying equipment and systems. With a focus on innovation and quality, the company has established itself as a trusted provider of high-temperature ash pneumatic conveying solutions. HeadPowder's products are designed to meet the specific needs of industrial clients, offering customized solutions that enhance operational efficiency and safety. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder's commitment to research and development ensures that its products remain at the forefront of industry standards, providing reliable and efficient solutions for material handling challenges. The company adheres to international quality standards and has a team of experienced engineers and technicians who work closely with clients to understand their requirements and provide tailored solutions. HeadPowder's reputation for reliability and performance has made it a preferred choice for many industrial facilities seeking advanced pneumatic conveying systems for high-temperature ash applications.