

Working Principle and Features of Rapeseed Material Handling
For agricultural operations dealing with rapeseed, efficient material handling is crucial to streamline processing and enhance productivity. The rapeseed material handling system, developed by Shandong HeadPowder Engineering Co., Ltd. based in China, offers a reliable solution for transporting and managing rapeseed from harvest to processing stages. This article explores the working principle and key features of this system, highlighting how it optimizes the handling process.
Understanding the Working Principle of Rapeseed Material Handling
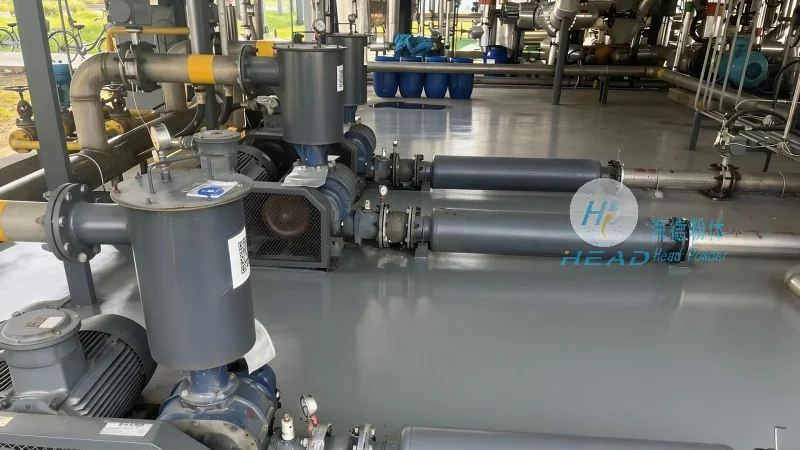
The rapeseed material handling system operates through a series of integrated components designed to move, store, and prepare rapeseed for further processing. At its core, the system utilizes mechanical and hydraulic mechanisms to ensure smooth material flow. The process typically begins with the collection of harvested rapeseed, which is then transferred into the handling equipment. Within the system, components such as conveyor belts, elevators, and storage bins work in tandem to transport the material. The conveyor belts, for instance, use motor-driven rollers to move the rapeseed from one location to another, while elevators lift the material vertically to different levels of the processing facility. Storage bins are strategically placed to hold the rapeseed temporarily, allowing for batch processing and reducing downtime. The hydraulic systems provide additional support by controlling the movement of gates and valves, ensuring precise control over the material flow. This integrated approach ensures that the rapeseed is handled safely and efficiently, minimizing the risk of damage or loss during transport.
Key Features of the Rapeseed Material Handling System
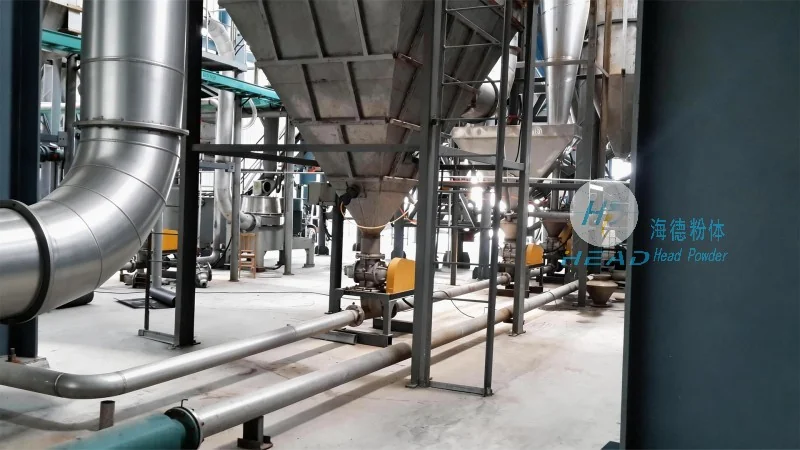
The rapeseed material handling system by Shandong HeadPowder Engineering Co., Ltd. incorporates several advanced features that enhance its performance and adaptability. One of the primary features is the modular design, which allows for easy customization based on the specific needs of the agricultural operation. This modularity enables the system to be expanded or reconfigured as production volumes change, providing long-term value. Another notable feature is the high-capacity conveyor system, which is engineered to handle large volumes of rapeseed without compromising speed or efficiency. The system’s durability is also a significant advantage, as it is constructed from robust materials that can withstand the rigors of continuous operation in agricultural settings. Additionally, the system includes advanced monitoring and control capabilities, allowing operators to track the material flow in real-time and make adjustments as needed. This level of control helps maintain optimal processing conditions and reduces the likelihood of bottlenecks or inefficiencies. The system also prioritizes safety, with features such as emergency stop buttons and protective guards to prevent accidents during operation. These safety measures ensure that the system is not only efficient but also safe for the operators and the environment.
Benefits of Implementing the Rapeseed Material Handling System
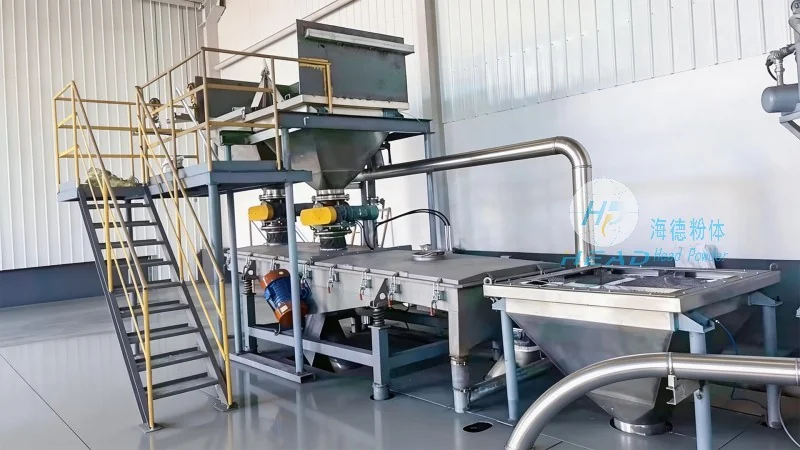
Adopting the rapeseed material handling system offers numerous benefits for agricultural businesses. The most obvious advantage is the significant improvement in operational efficiency. By automating the material handling process, the system reduces the need for manual labor, allowing workers to focus on other critical tasks. This leads to faster processing times and increased overall productivity. The system also minimizes material loss, as the integrated components ensure that the rapeseed is handled gently and without damage. This not only preserves the quality of the rapeseed but also reduces waste, contributing to cost savings. Furthermore, the system’s adaptability allows it to be integrated into existing agricultural facilities with minimal disruption. This makes it an ideal solution for both new and existing operations looking to upgrade their material handling capabilities. The system’s reliability is another key benefit, as it is designed to operate continuously without frequent breakdowns. This reduces downtime and ensures that the processing line remains operational, even during peak production periods. Overall, the rapeseed material handling system provides a comprehensive solution for managing rapeseed efficiently, supporting the growth and success of agricultural enterprises.
Conclusion
In conclusion, the rapeseed material handling system developed by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and effective solution for agricultural operations. Its working principle, based on integrated mechanical and hydraulic components, ensures smooth and efficient material flow. The key features, including modularity, high capacity, and advanced monitoring, enhance its performance and adaptability. The benefits of implementing this system, such as improved efficiency, reduced waste, and increased productivity, make it a valuable investment for agricultural businesses. By leveraging this technology, operations can streamline their processes and achieve greater success in rapeseed handling and processing. Shandong HeadPowder Engineering Co., Ltd. continues to provide innovative solutions that meet the evolving needs of the agricultural industry, ensuring that rapeseed material handling remains efficient and reliable.