

Working Principle and Features of Sugar Material Conveying
Understanding the working principle and features of sugar material conveying systems is crucial for optimizing industrial processes in the sugar industry. This article provides an in-depth overview of how these systems operate and their key characteristics, tailored for professionals seeking efficient material handling solutions.
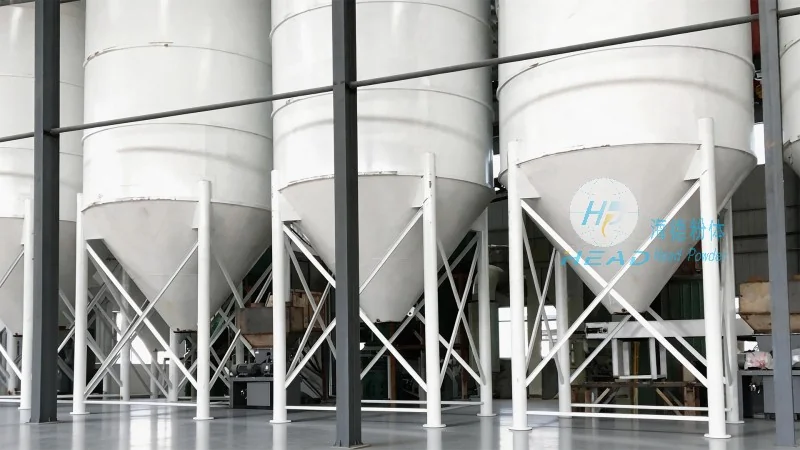
Working Principle of Sugar Material Conveying
Sugar material conveying systems typically operate through a combination of mechanical components designed to transport bulk sugar from one location to another within a processing facility. The core mechanism often involves a conveyor belt or similar transport medium that moves the sugar through a series of stages, such as loading, transport, and unloading. These systems may utilize gravity, mechanical power, or a combination of both to ensure smooth and continuous movement of the material. The process begins with the sugar being fed into the system, where it is then carried along the conveyor path by rollers or a belt. As the material travels, it may undergo intermediate processing steps, such as screening or sorting, before reaching the final destination. The efficiency of the conveying system depends on factors like the type of equipment used, the volume of material being handled, and the distance over which it needs to be transported. Modern systems often incorporate advanced control technologies to adjust speed and direction based on real-time operational needs, enhancing overall performance and reducing downtime.
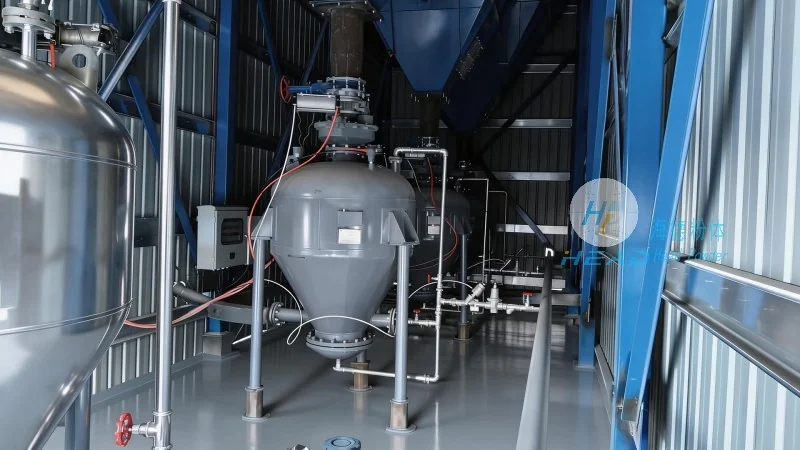
Key Features of Sugar Material Conveying Systems
Effective sugar material conveying systems exhibit several distinct features that contribute to their reliability and performance. One of the primary features is the ability to handle large volumes of bulk material with minimal human intervention. This automation reduces labor costs and improves safety by minimizing exposure to heavy machinery and moving parts. Another important feature is the system's adaptability to different sugar types and particle sizes. Whether dealing with raw sugar, refined sugar, or other sugar derivatives, the conveying equipment can be adjusted to accommodate variations in density and flow characteristics. Durability is also a critical feature, as sugar handling environments can be harsh, with high humidity and potential for abrasion. High-quality materials, such as stainless steel or specialized coatings, are used to ensure the equipment withstands these conditions over extended periods. Additionally, energy efficiency is a key consideration in modern conveying systems. Advanced designs incorporate energy-saving mechanisms, such as variable speed drives, to reduce power consumption while maintaining optimal performance. This not only lowers operational costs but also aligns with sustainability goals in the industry.
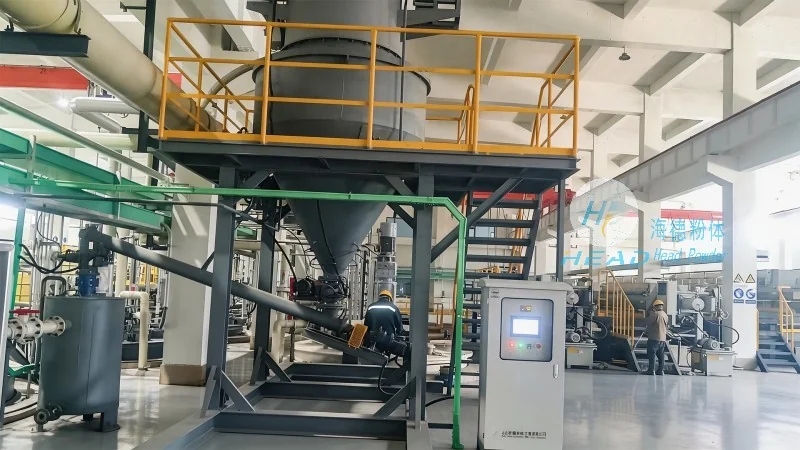
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in industrial conveying solutions for the sugar sector. With a strong presence in China, the company has built a reputation for delivering high-quality equipment tailored to the unique demands of sugar processing. HeadPowder's expertise lies in designing and manufacturing systems that enhance efficiency, safety, and durability in material handling operations. The company's commitment to innovation ensures that their products incorporate the latest technological advancements, providing clients with reliable and cost-effective solutions. By focusing on customer needs and industry standards, HeadPowder has established itself as a trusted partner for sugar manufacturers seeking to optimize their conveying processes.
Conclusion
In summary, sugar material conveying systems rely on a well-engineered combination of mechanical components and control technologies to efficiently transport bulk sugar. Their key features, including automation, adaptability, durability, and energy efficiency, make them essential for modern sugar processing facilities. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these advanced solutions, helping the industry maintain high standards of productivity and safety. As the sugar industry continues to evolve, the importance of reliable conveying systems will only grow, making them a critical component of efficient operations.