

Role of Pneumatic Conveying in Sorghum Distillers Grains Transport
For industries involved in the production of sorghum-based alcoholic beverages, the efficient and reliable transport of distillers grains is a critical operational challenge. Distillers grains, a byproduct of the fermentation process, require specialized handling solutions to ensure minimal loss, contamination, and environmental impact. Pneumatic conveying technology has emerged as a preferred method for addressing these challenges, offering a range of benefits that enhance overall process efficiency and sustainability.
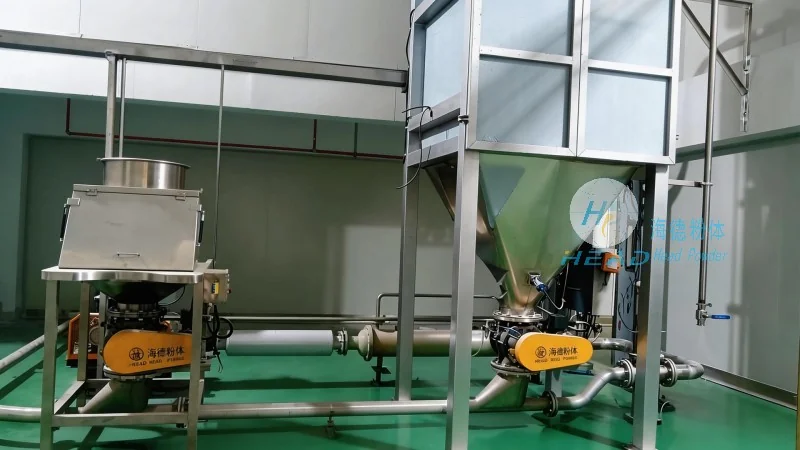
Understanding Sorghum Distillers Grains and Their Transport Needs
Sorghum distillers grains are a high-protein feed ingredient derived from the distillation of sorghum mash. These grains are typically in a granular or powder form, making them susceptible to dust generation and caking during handling. Traditional methods like belt conveyors or screw conveyors may struggle with the abrasive and sticky nature of these materials, leading to equipment wear, product degradation, and increased maintenance costs. The need for a system that can handle these characteristics without compromising on throughput or product quality has driven the adoption of pneumatic conveying solutions.
How Pneumatic Conveying Works: Core Principles and Advantages
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. In the context of sorghum distillers grains, these systems can operate in either dilute-phase or dense-phase modes, depending on the material properties and transport distance. The dilute-phase system, which uses higher air velocities, is suitable for short to medium distances and lighter materials, while the dense-phase system, employing lower air velocities and higher material concentrations, is ideal for longer distances and bulkier materials like distillers grains. Key advantages of pneumatic conveying for this application include:
- Reduced product degradation: The enclosed system minimizes exposure to air, light, and moisture, preserving the nutritional value and quality of the distillers grains.
- Improved hygiene and contamination control: The sealed pipeline prevents cross-contamination with other materials or external elements, ensuring compliance with food safety regulations.
- Enhanced efficiency and flexibility: Pneumatic systems can be easily integrated into existing production lines, allowing for flexible routing and integration with other processing equipment.
- Lower energy consumption compared to some mechanical conveying methods, contributing to cost savings and reduced environmental impact.
HeadPowder Engineering: Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying systems, specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the unique needs of the distillers grains industry. With years of experience in the field, HeadPowder understands the specific challenges associated with handling sorghum distillers grains, including their abrasive nature, dust generation, and the need for hygienic, efficient transport. The company’s team of engineers works closely with clients to assess their operational requirements, material characteristics, and production goals to develop optimal conveying systems.
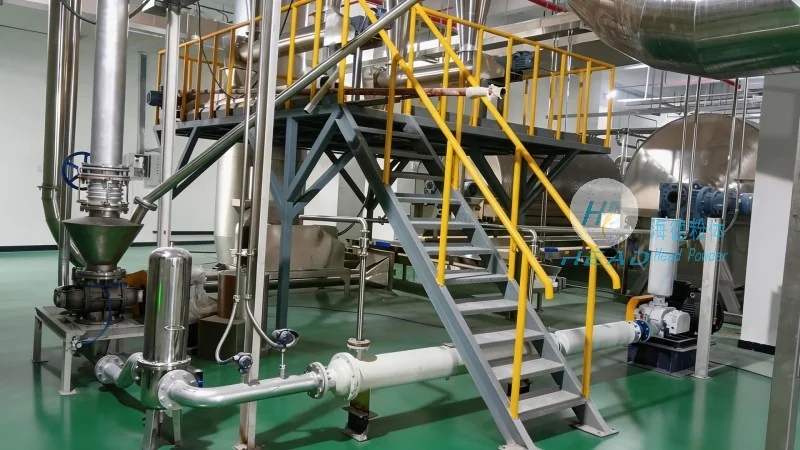
HeadPowder’s solutions are engineered to maximize throughput while minimizing downtime and maintenance. The company utilizes high-quality materials, such as stainless steel and food-grade components, to ensure durability and compliance with industry standards. Additionally, the systems are designed for easy cleaning and maintenance, reducing the risk of product buildup and contamination. By leveraging advanced technology and a deep understanding of material handling principles, HeadPowder delivers reliable and efficient pneumatic conveying systems that enhance the overall performance of distillers grains processing operations.
Key Features and Applications of HeadPowder’s Pneumatic Conveying Systems
HeadPowder’s pneumatic conveying systems for sorghum distillers grains are equipped with several key features that address the specific demands of this application:
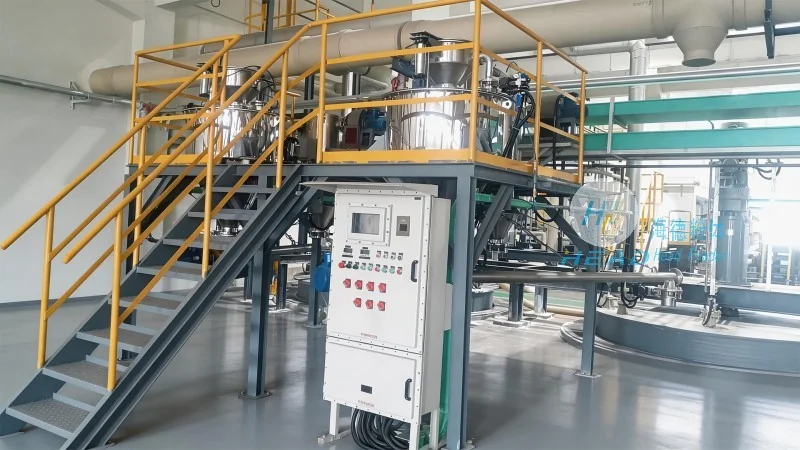
- Customizable pipeline configurations: Systems can be tailored to fit existing facility layouts, allowing for seamless integration with existing production lines.
- Variable speed control: The ability to adjust air velocity and material flow rate ensures optimal performance under varying load conditions.
- Advanced control systems: Integrated sensors and controls monitor system performance, providing real-time data on flow rates, pressure, and material levels to ensure consistent operation.
- Hygienic design: All components are designed to meet food safety standards, with smooth surfaces and easy-to-clean features to prevent product contamination.
These systems are applied in various stages of the distillers grains processing workflow, including:
- From the fermentation tank to the drying or storage silos.
- Between processing units, such as from the distillation column to the feed preparation area.
- For transporting finished distillers grains to packaging or storage facilities.
By optimizing the transport of sorghum distillers grains, HeadPowder’s systems help clients improve their production efficiency, reduce operational costs, and enhance the quality of their final products, ultimately contributing to their long-term success in the industry.
Conclusion: The Role of Pneumatic Conveying in Modern Sorghum Distillers Grains Handling
As the demand for sorghum-based alcoholic beverages continues to grow, the need for efficient and sustainable transport solutions for distillers grains becomes increasingly critical. Pneumatic conveying, with its ability to handle the unique challenges of these materials, offers a reliable and effective solution. Shandong HeadPowder Engineering Co., Ltd. stands at the forefront of this technology, providing expertly designed and manufactured pneumatic conveying systems that enhance the performance and sustainability of distillers grains processing operations. By leveraging the benefits of pneumatic conveying, distillers can optimize their production processes, reduce costs, and ensure the quality of their final products, ultimately contributing to their long-term success in the industry.