

Working Principle and Features of Borax Material Handling
Borax, a widely used chemical compound in various industries, requires efficient and reliable material handling systems to ensure smooth production processes. The working principle and features of borax material handling equipment are crucial for optimizing operations and maintaining product quality. This article explores the core mechanisms behind borax material handling and highlights the key characteristics that make such systems effective.

Understanding the Working Principle of Borax Material Handling
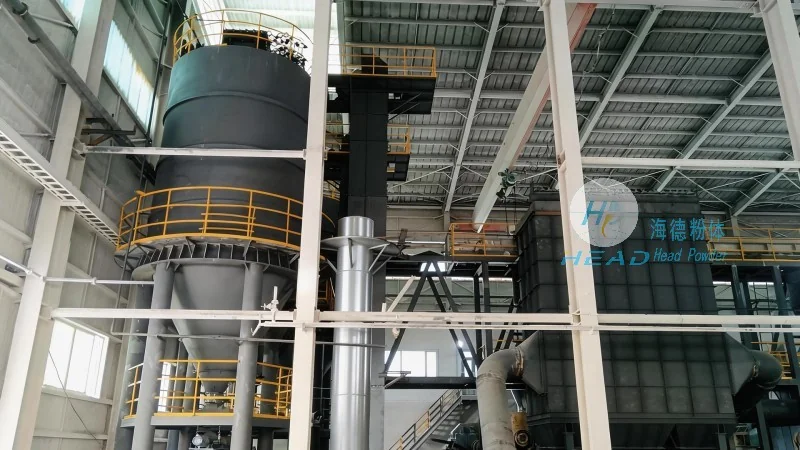
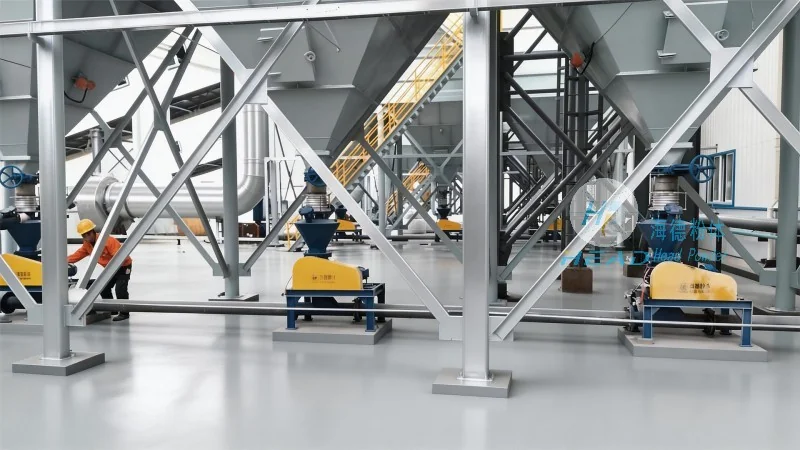
The working principle of borax material handling typically involves a combination of mechanical and automated processes designed to transport, store, and manage borax in industrial settings. At the heart of these systems are components such as conveyors, elevators, and storage silos that work in tandem to move borax from its source to processing units or storage areas. The process begins with the collection of borax from bulk containers or production lines, where it is then transferred into a conveyor system. This system may include belt conveyors, screw conveyors, or pneumatic conveyors, depending on the specific application and material characteristics. The choice of conveyor type is critical as it directly impacts the efficiency and safety of the material handling operation. For instance, belt conveyors are commonly used for transporting loose borax due to their ability to handle bulk quantities with minimal product degradation. Screw conveyors, on the other hand, are ideal for transporting borax in a more controlled manner, especially when dealing with finer powders that require precise dosing. Pneumatic conveyors offer an alternative for handling borax in a dust-free environment, which is essential for maintaining product purity and worker safety. Once the borax is moved through the conveyor system, it may be directed into storage silos or processing equipment. The storage silos are designed to hold large volumes of borax and are equipped with level sensors and discharge mechanisms to regulate the flow of material. These sensors ensure that the silos are not overfilled or underfilled, preventing issues such as product spillage or equipment overload. The discharge mechanisms, often controlled by automated valves or gates, allow for controlled release of borax into processing units or packaging lines. The entire process is typically monitored by a control system that integrates data from various sensors and adjusts the operation of the equipment as needed. This closed-loop control system enhances the efficiency of the material handling operation by minimizing downtime and maximizing throughput. In summary, the working principle of borax material handling revolves around the coordinated operation of conveyors, storage systems, and control mechanisms to ensure the safe and efficient movement of borax throughout the production process.
Key Features of Borax Material Handling Systems
Borax material handling systems are characterized by several key features that distinguish them from other material handling solutions. These features are designed to address the unique challenges associated with handling borax, such as its chemical properties, particle size, and the need for dust control. One of the primary features is the emphasis on dust-free operation. Borax is a fine powder that can easily generate dust, which not only poses health risks to workers but also affects product quality by causing contamination. To mitigate these issues, borax material handling systems incorporate dust suppression measures, such as sealed conveyor systems, dust collection hoods, and air filtration units. These features help maintain a clean working environment and prevent the spread of borax dust throughout the facility. Another important feature is the ability to handle varying particle sizes and bulk densities. Borax can exist in different forms, including granules, powders, and crystals, each with distinct handling characteristics. The systems are designed to accommodate these variations by using adjustable conveyor speeds, variable screw pitch, and flexible storage silos. This adaptability ensures that the material handling process remains efficient regardless of the borax's physical state. Additionally, borax material handling systems prioritize safety and compliance with industrial standards. They are equipped with safety features such as emergency stop buttons, overload protection, and material flow sensors. These features help prevent accidents and ensure that the operation adheres to regulatory requirements. The systems also often include maintenance-friendly designs, with easy access to components for inspection and repair. This reduces downtime and lowers the overall cost of ownership. Furthermore, the integration of automation and control systems is a hallmark of modern borax material handling solutions. These systems allow for real-time monitoring of the process, data logging, and remote operation. This level of automation enhances operational efficiency and provides valuable insights into the performance of the material handling system. In conclusion, the key features of borax material handling systems focus on dust control, adaptability to different material forms, safety, and automation. These features collectively contribute to the effectiveness and reliability of borax material handling operations.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized material handling solutions for the chemical industry. With its headquarters located in Shandong, China, the company has established itself as a trusted partner for businesses dealing with borax and other chemical materials. HeadPowder specializes in designing, manufacturing, and installing custom material handling systems tailored to the specific needs of its clients. The company's expertise lies in understanding the unique challenges of handling chemicals like borax and developing solutions that address these challenges effectively. By leveraging advanced technology and a deep understanding of industrial processes, HeadPowder delivers systems that enhance productivity, improve safety, and ensure product quality. The company's commitment to quality and customer satisfaction has earned it a reputation as a reliable supplier in the industry. HeadPowder's team of engineers and technicians work closely with clients to understand their operational requirements and provide tailored solutions. This collaborative approach ensures that the material handling systems are optimized for the specific application, whether it involves bulk storage, processing, or packaging. The company's facilities in Shandong, China, are equipped with state-of-the-art equipment and testing facilities, allowing for the development and testing of new material handling technologies. This enables HeadPowder to stay at the forefront of industry advancements and offer cutting-edge solutions to its clients. In summary, Shandong HeadPowder Engineering Co., Ltd. is a reputable company dedicated to providing high-quality material handling solutions for the borax and chemical industries. Its focus on customization, safety, and efficiency makes it a preferred choice for businesses seeking reliable material handling systems.