

Working Principle and Features of a Carbonate Manganese Powder Pneumatic Conveying System
For industrial applications involving the handling of carbonate manganese powder, efficient and reliable material transport is crucial. The pneumatic conveying system designed specifically for this purpose offers a solution that combines advanced technology with practical design to meet the demands of modern manufacturing processes.
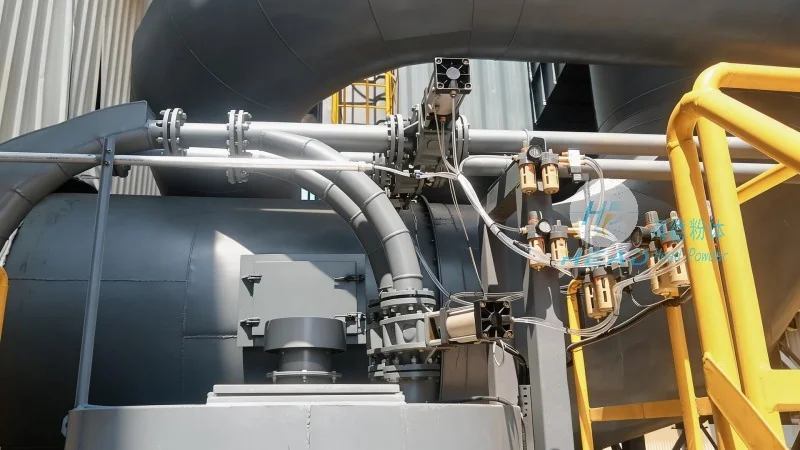
Introduction to Carbonate Manganese Powder Pneumatic Conveying Systems
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the development and production of pneumatic conveying equipment tailored for various powder materials, including carbonate manganese. This system is engineered to handle the unique properties of carbonate manganese powder, such as its fine particle size and potential for static charge accumulation, ensuring safe and efficient material transport from source to destination.
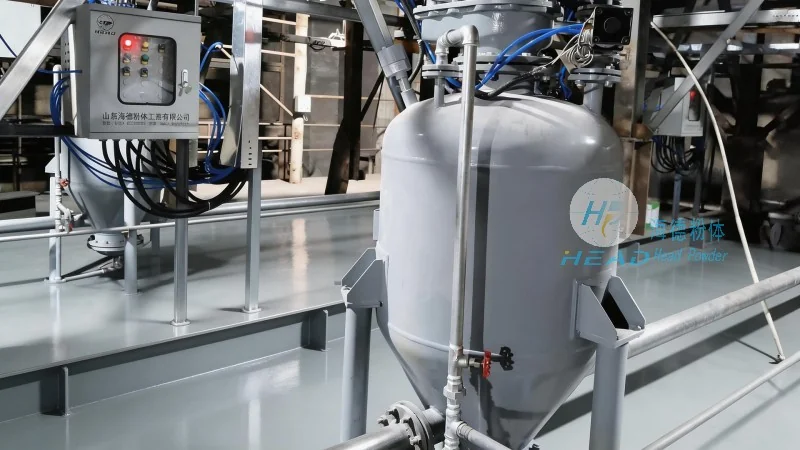
The Working Principle of the Pneumatic Conveying System
The core of the carbonate manganese powder pneumatic conveying system is its pneumatic transport mechanism, which operates by using compressed air to move the powder through a network of pipes. The process begins with the powder being fed into a hopper or feeder, where it is then drawn into the conveying line by the pressure differential created by the air flow. As the air and powder mixture travels through the pipeline, the system maintains a consistent flow rate, preventing blockages and ensuring uniform material distribution. The system typically includes components such as a blower, cyclone separator, and dust collector, each playing a critical role in the overall operation.
Key Features and Advantages
Several key features distinguish the carbonate manganese powder pneumatic conveying system from traditional methods. Firstly, it provides a dust-free and enclosed transport environment, which is essential for maintaining product purity and preventing contamination. Secondly, the system offers high efficiency in terms of material handling, with the ability to transport large quantities of powder over significant distances without the need for manual intervention. Additionally, the design minimizes material degradation and loss, as the powder is handled gently within the sealed system. Another notable advantage is the flexibility of the system, which can be adjusted to accommodate varying powder flow rates and particle sizes, making it suitable for diverse industrial applications.
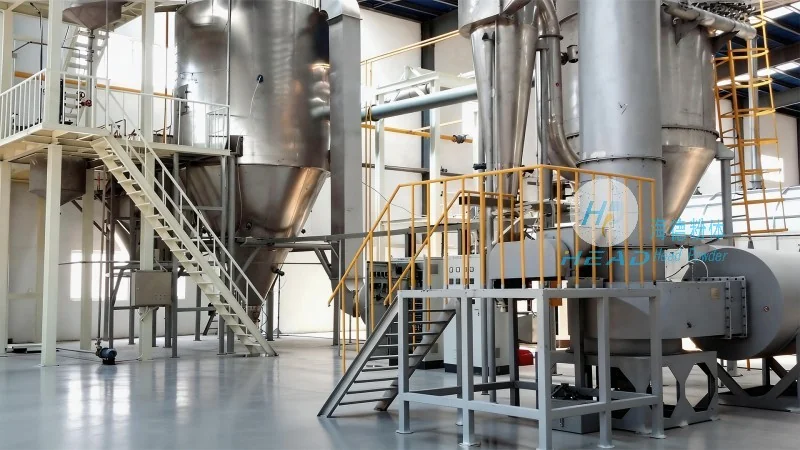
Technical Specifications and Customization Options
HeadPowder Engineering Co., Ltd. offers customizable pneumatic conveying systems that can be tailored to meet specific operational requirements. The systems are available in various configurations, including positive pressure and negative pressure designs, to suit different plant layouts and material handling needs. Technical specifications such as air pressure, flow rate, and pipe diameter can be adjusted based on the volume of carbonate manganese powder to be transported. The company also provides maintenance and support services to ensure the long-term reliability and performance of the equipment.