

What is a Fertilizer Material Pneumatic Conveying Machine? And What Are Its Design Principles?
When it comes to efficiently transporting bulk materials like fertilizers, pneumatic conveying systems have become a cornerstone of modern industrial operations. These machines, often referred to as fertilizer material pneumatic conveying machines, offer a reliable and efficient solution for moving granular or powdered materials over short to medium distances. In this article, we will explore what these machines are, how they work, and the key design principles that underpin their functionality.
Understanding Pneumatic Conveying Systems for Fertilizer Handling
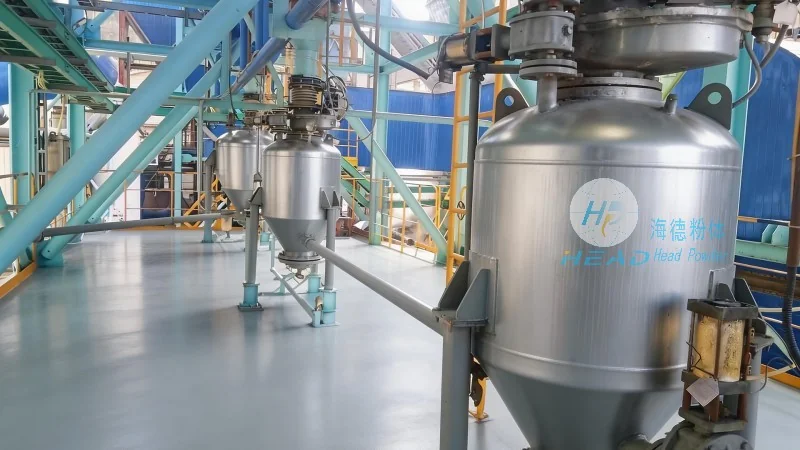
A fertilizer material pneumatic conveying machine is a specialized piece of equipment designed to transport bulk solid materials, such as fertilizers, through a pipeline using a flow of air or other gas. Unlike traditional mechanical conveyors that rely on belts or screws, pneumatic systems utilize the force of compressed air to move materials, making them particularly suitable for handling fine powders and granules that might be prone to caking or degradation under mechanical stress.
Key Components and Working Principle
The core of a pneumatic conveying machine consists of several essential components, each playing a critical role in the material transport process. The primary components include a material hopper or feeder, a compressor or air source, a pipeline system, and a discharge or receiver unit. The process typically begins with the material being fed into the hopper, where it is then drawn into the pipeline by the moving air stream generated by the compressor.
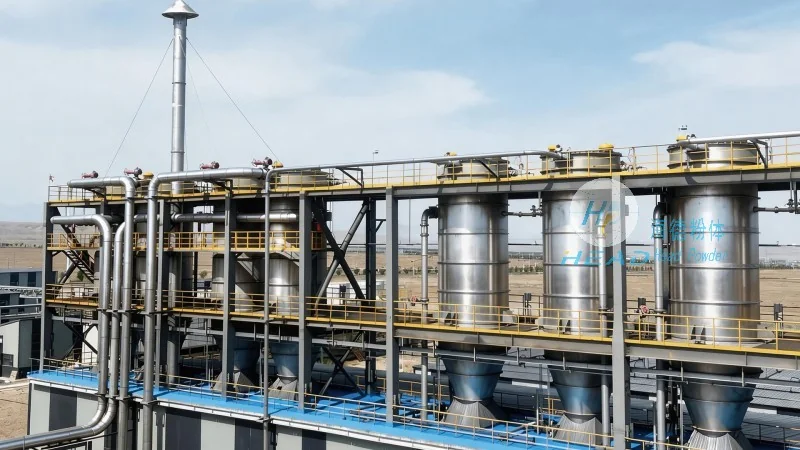
As the air flows through the pipeline, it carries the fertilizer particles along with it, creating a dense or dilute phase flow depending on the system design. The design of the pipeline, including the use of bends, valves, and expansion joints, is crucial for maintaining the integrity of the material flow and preventing blockages or pressure losses. The compressor provides the necessary pressure to overcome friction losses in the system and ensure the material reaches its destination efficiently.
Design Principles for Optimal Performance
The design of a fertilizer material pneumatic conveying machine is governed by several key principles aimed at maximizing efficiency, minimizing energy consumption, and ensuring reliable operation. One of the most critical design considerations is the selection of the appropriate air velocity and pressure. The air velocity must be high enough to prevent material settling or clogging in the pipeline but low enough to avoid excessive wear on the system components.
Another important design principle is the system's capacity and scale. The conveying capacity is determined by factors such as the material's bulk density, particle size distribution, and the desired conveying distance. Engineers must carefully calculate the required air volume and pressure to achieve the desired throughput without compromising system efficiency or durability. The use of appropriate materials for the pipeline and components, such as stainless steel or corrosion-resistant alloys, is also essential to handle the chemical properties of fertilizers and prevent degradation over time.
Applications and Benefits in Fertilizer Industry
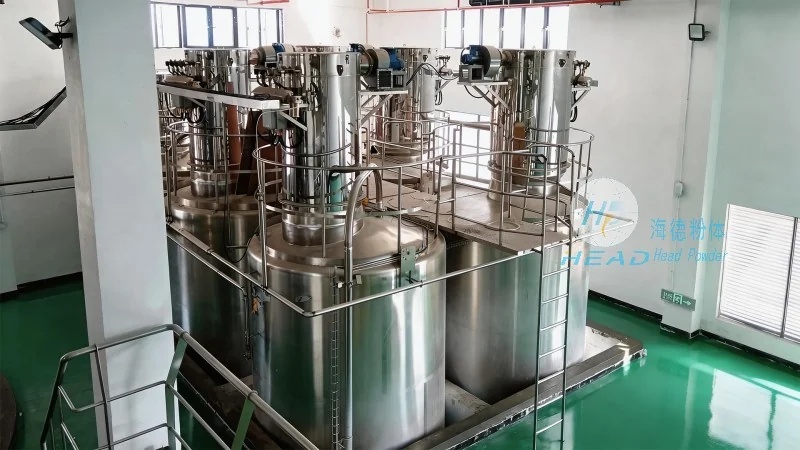
Fertilizer material pneumatic conveying machines are widely used in various stages of the fertilizer production and distribution process. They are commonly employed for transporting raw materials from storage silos to processing units, moving finished products from production lines to packaging areas, and even for handling bulk fertilizers in agricultural supply chains. The benefits of using pneumatic conveying systems in the fertilizer industry include improved safety, as there is no direct human contact with the material, reduced labor costs due to automated operation, and enhanced product quality by minimizing exposure to moisture and contaminants.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design and production of pneumatic conveying equipment for the fertilizer industry. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's products are engineered to meet the specific demands of the fertilizer sector, ensuring durability, energy efficiency, and consistent performance in demanding operational environments.
Conclusion
In conclusion, fertilizer material pneumatic conveying machines represent a sophisticated and efficient solution for the transportation of bulk fertilizers. By understanding the design principles and components of these systems, industries can optimize their material handling processes, reduce operational costs, and enhance overall productivity. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. continues to advance the technology and deliver high-quality equipment that meets the evolving needs of the fertilizer industry.