

Capsule Pneumatic Conveying: How to Efficiently Transport Powders and Granules with Air Flow?
Capsule pneumatic conveying is a sophisticated method used to transport powders and granules through a system driven by air flow. This technology offers a reliable and efficient alternative to traditional material handling methods, particularly in industries where dust control, product integrity, and process automation are critical. The core principle involves using compressed air to move bulk materials through a network of pipes, often utilizing specialized capsules or flexible hoses that can adapt to varying flow rates and material characteristics.
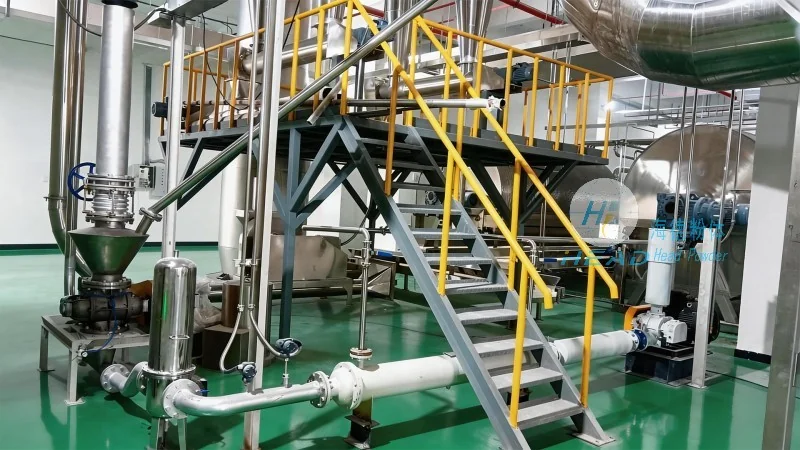
Understanding the Technology Behind Capsule Pneumatic Conveying
At the heart of capsule pneumatic conveying is the use of flexible, air-filled capsules that act as the transport medium. These capsules, also known as "pneumatic conveying tubes" or "air hoses," are designed to carry powders and granules from a source to a destination. The system typically includes a feeding mechanism, a conveying line, and a discharge unit. As air is introduced into the capsule, it expands and creates a low-pressure environment that draws the material into the tube. The capsules then move the material along the pipeline, ensuring minimal product degradation and consistent flow rates. This method is particularly effective for handling fine powders, which are prone to caking or agglomeration in traditional systems.
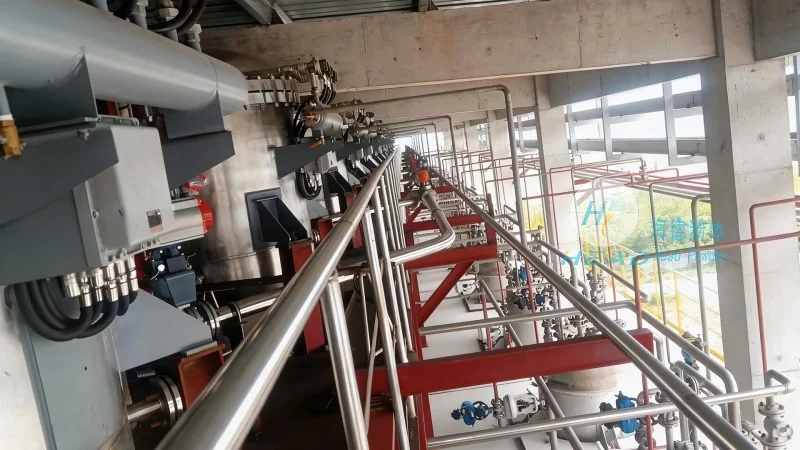
Key Advantages of Capsule Pneumatic Conveying Systems
One of the primary benefits of capsule pneumatic conveying is its ability to maintain product purity and quality. Unlike rigid pipelines, which can cause friction and particle attrition, the flexible capsules reduce the risk of contamination and material degradation. Additionally, this technology offers excellent dust control, as the material is contained within the capsules and the system, minimizing the risk of airborne particles. Another significant advantage is the system's adaptability to different material types and flow rates. The capsules can be adjusted to accommodate various particle sizes, densities, and moisture levels, making it suitable for a wide range of applications. Furthermore, capsule pneumatic conveying systems are relatively easy to install and maintain, with fewer moving parts compared to traditional mechanical conveyors. This leads to lower operational costs and reduced downtime.
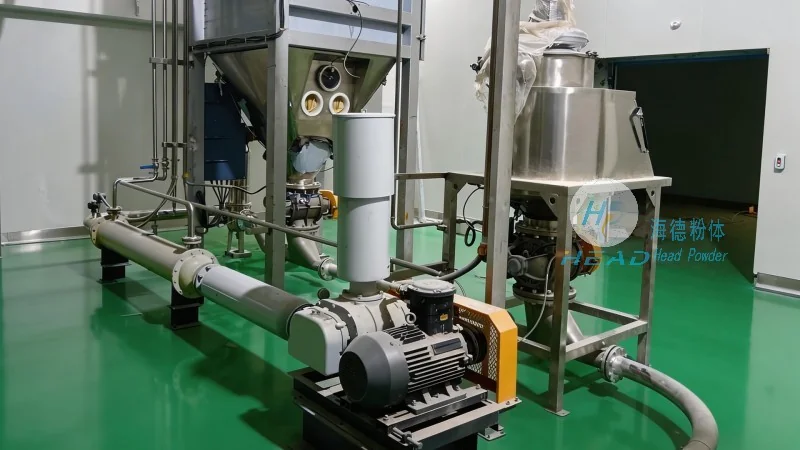
Applications in Various Industries
Capsule pneumatic conveying is widely used across multiple industries due to its versatility and efficiency. In the pharmaceutical industry, for example, it is used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements. The system's ability to maintain product integrity and prevent cross-contamination makes it ideal for handling sensitive materials. In the food and beverage sector, capsule pneumatic conveying is employed to transport powders such as flour, sugar, and spices, ensuring that the products remain fresh and free from contamination. The chemical industry also benefits from this technology, as it can handle corrosive or hazardous materials safely and efficiently. Additionally, in the agricultural sector, capsule pneumatic conveying is used to transport grain and other agricultural products, improving the efficiency of storage and processing operations.
How Shandong HeadPowder Engineering Co., Ltd. Enhances Capsule Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing advanced capsule pneumatic conveying systems. With years of experience in the industry, the company has developed state-of-the-art technology that meets the diverse needs of various sectors. HeadPowder's solutions are tailored to specific applications, ensuring optimal performance and efficiency. The company's team of experts works closely with clients to understand their unique requirements and provide customized solutions that enhance productivity and reduce operational costs. HeadPowder, headquartered in Shandong, China, has established itself as a trusted partner for businesses seeking reliable and efficient material transport solutions. The company's facilities are equipped with the latest manufacturing technologies, ensuring that each system is built to the highest standards of durability and performance. By leveraging the expertise of HeadPowder, industries can achieve improved process efficiency, reduced maintenance costs, and enhanced product quality.
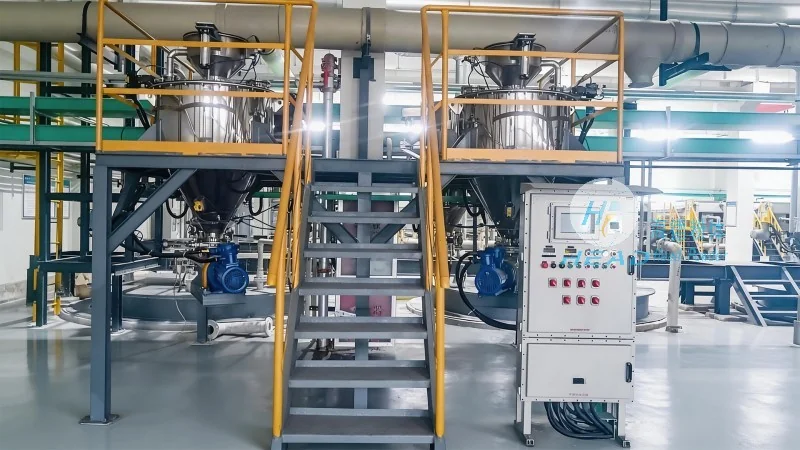
Conclusion: The Future of Efficient Powder and Granule Transport
Capsule pneumatic conveying represents a significant advancement in material handling technology, offering a sustainable and efficient solution for transporting powders and granules. As industries continue to prioritize product quality, process automation, and operational efficiency, this technology will play an increasingly important role. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this innovation, providing cutting-edge solutions that meet the evolving needs of the market. By investing in capsule pneumatic conveying systems, businesses can enhance their operational capabilities, reduce costs, and improve overall productivity. The future of efficient material transport is clearly aligned with the capabilities of capsule pneumatic conveying, and companies like HeadPowder are leading the way in this transformation.