

Principle and Working Scene Characteristics of Coal Fly Ash Material Handling Systems
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of efficient coal fly ash material handling systems. This article explores the fundamental principles underlying these systems and highlights the key characteristics of their operational environments.
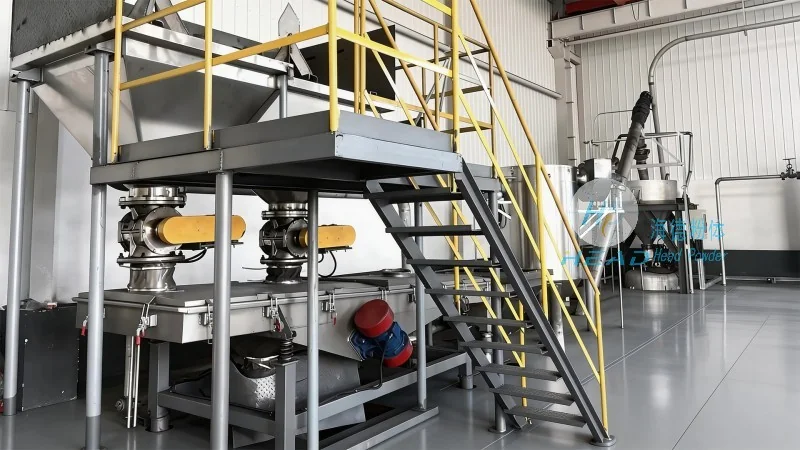
Overview of Coal Fly Ash Material Handling Systems
Coal fly ash, a byproduct of coal combustion in power plants, is a valuable resource that requires specialized handling to ensure safe and efficient transportation. The material handling systems designed for coal fly ash typically involve a combination of equipment such as conveyors, silos, and storage facilities. These systems are engineered to manage the unique properties of fly ash, including its fine particle size, abrasive nature, and potential for dust generation. By integrating advanced technologies and robust engineering, these systems ensure that coal fly ash can be transported from production sites to processing or disposal locations with minimal loss and maximum safety.
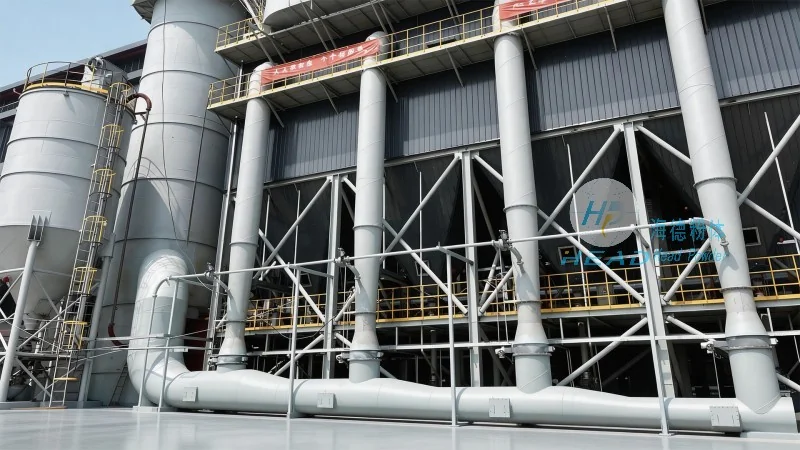
Core Principles of Material Handling
The operation of coal fly ash material handling systems is governed by several core principles that ensure optimal performance. First, the system must maintain a consistent flow of material, preventing blockages or overloading of equipment. This is achieved through the use of variable speed drives, level sensors, and automated control systems that adjust the flow rate based on real-time conditions. Second, the system must address the challenges posed by fly ash's fine particle size and dust generation. This involves implementing dust suppression measures, such as wetting systems or enclosed conveyor designs, to minimize air pollution and protect personnel. Third, the system must prioritize safety and compliance with environmental regulations. This includes features like explosion-proof designs for certain components, regular maintenance schedules, and adherence to local and national standards for material handling.
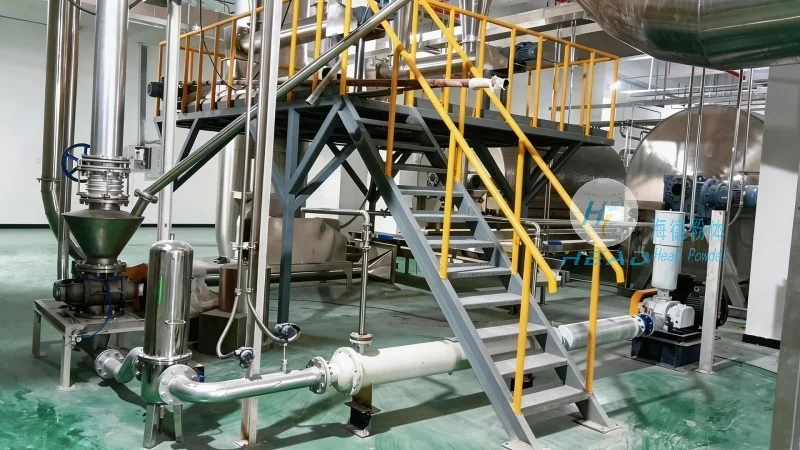
Working Scene Characteristics
The operational environments where coal fly ash material handling systems are deployed vary significantly, each presenting unique challenges and requirements. In power plant settings, these systems are often integrated with existing infrastructure, requiring seamless integration with other industrial processes. The working scene may involve high-volume material flow, with systems designed to handle large quantities of fly ash in a continuous operation. In contrast, systems used for smaller-scale applications or in remote locations may focus on portability and adaptability, with components that can be easily transported and set up. The environmental conditions also play a critical role, as systems must be able to operate in diverse climates, from hot and humid regions to cold and arid areas. Additionally, the systems must be designed to accommodate different storage and transportation needs, such as bulk storage in silos or the loading of trucks and ships for off-site disposal or utilization.
Key Features and Benefits
Modern coal fly ash material handling systems from HeadPowder are equipped with several key features that enhance their performance and reliability. These include advanced control systems that provide real-time monitoring of system parameters, such as flow rate, pressure, and temperature. The systems also incorporate robust materials and coatings to withstand the abrasive nature of fly ash, extending the lifespan of components and reducing maintenance costs. Furthermore, the use of energy-efficient designs helps to minimize operational costs while reducing the environmental impact of the system. The benefits of these systems extend beyond mere functionality, as they contribute to improved safety for workers, reduced environmental pollution, and increased operational efficiency for power plants and other facilities.
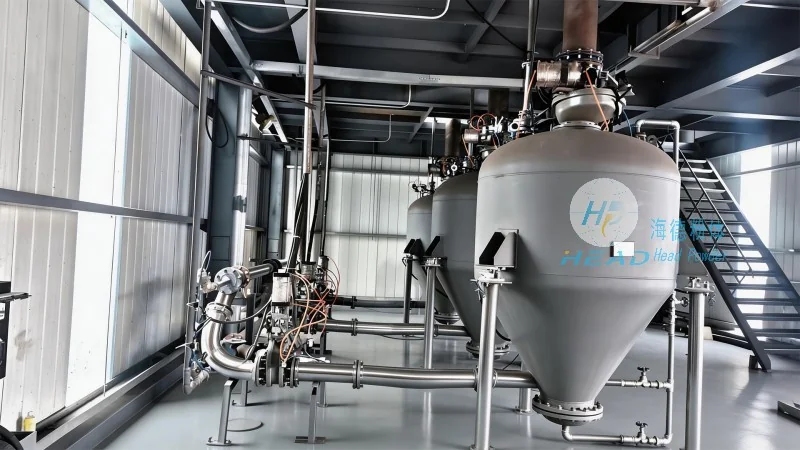
Conclusion
Coal fly ash material handling systems are critical components of modern industrial operations, enabling the safe and efficient management of a valuable byproduct. By adhering to the core principles of consistent flow, dust control, and safety compliance, these systems ensure that coal fly ash can be handled effectively in diverse working environments. HeadPowder's expertise in designing and implementing such systems positions them as a trusted partner for power plants and other facilities seeking reliable material handling solutions. The continued development of advanced technologies in this field will further enhance the efficiency and sustainability of coal fly ash management, supporting the broader goals of industrial and environmental responsibility.