

Principle and Working Scene Characteristics of High-Pressure Bin Pump Pneumatic Conveying Systems
HeadPowder, also known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of pneumatic conveying equipment. The company is based in Shandong, China, and specializes in the design, development, and production of advanced high-pressure bin pump systems for various industrial applications. With a strong focus on innovation and quality, HeadPowder provides reliable solutions for material handling and transportation in diverse industries.
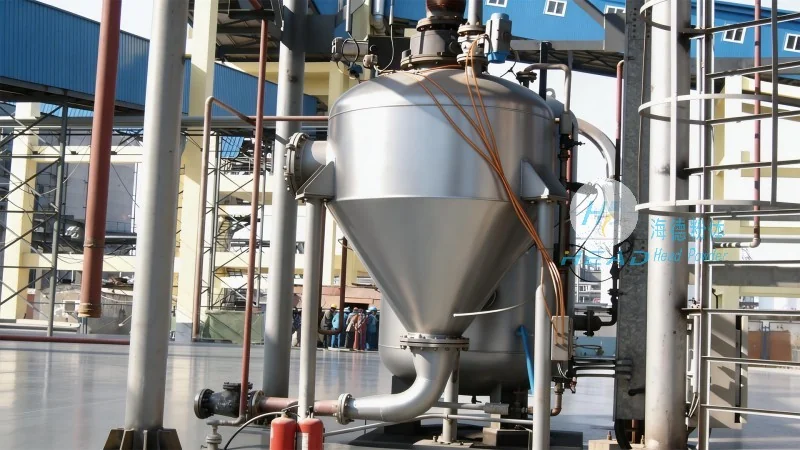
Principle of High-Pressure Bin Pump Pneumatic Conveying Systems
High-pressure bin pump pneumatic conveying systems operate based on the principle of creating a high-pressure air flow within a storage bin or hopper. The system uses a high-pressure pump to generate the necessary pressure, which forces the material to be conveyed through a pipeline. The process involves several key components, including a storage bin, a high-pressure pump, a control system, and a pipeline network. The material is first loaded into the storage bin, and then the pump creates a high-pressure air stream that draws the material into the pipeline. The material is then transported to the destination point, where it is discharged. This method of conveying is particularly effective for handling bulk materials such as powders, granules, and fine particles, as it allows for efficient and continuous material transport without the need for mechanical components like belts or buckets.
Working Scene Characteristics of High-Pressure Bin Pump Systems
High-pressure bin pump pneumatic conveying systems are widely used in various industrial settings due to their versatility and efficiency. These systems are commonly employed in industries such as chemical, food, pharmaceutical, and mining, where the transportation of bulk materials is essential. The working scene characteristics of these systems include high conveying capacity, long-distance transport capabilities, and the ability to handle a wide range of materials with different properties. Additionally, the systems are designed to be compact and easy to install, making them suitable for both new and existing facilities. The high-pressure operation also ensures that the material is conveyed with minimal degradation, preserving its quality and integrity. Furthermore, the control systems used in these pumps allow for precise regulation of the conveying process, enabling operators to adjust the flow rate and pressure as needed to meet specific production requirements.
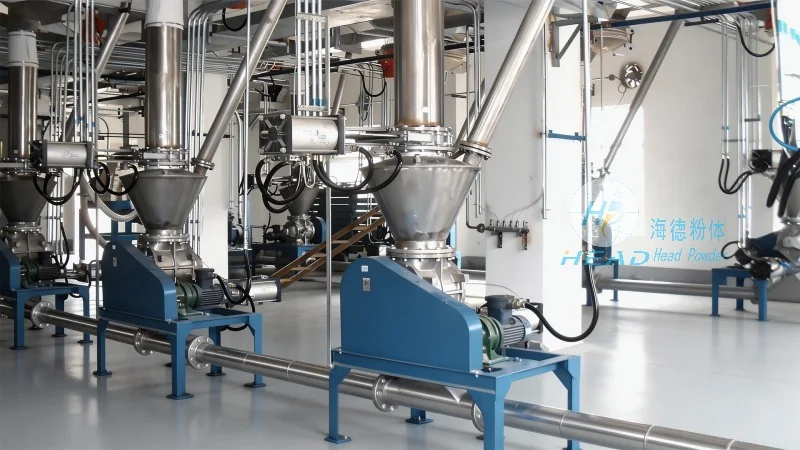
Application Examples in Industrial Fields
In the chemical industry, high-pressure bin pump systems are used to transport various powders and granules, such as chemicals, pigments, and additives. The systems are capable of handling materials with different particle sizes and moisture contents, ensuring consistent and reliable transport. In the food industry, these pumps are employed to convey food powders, such as flour, sugar, and spices, maintaining hygiene and preventing contamination. The pharmaceutical industry also utilizes high-pressure bin pumps to transport active pharmaceutical ingredients (APIs) and other fine powders, where product purity is critical. In the mining sector, the systems are used to convey raw materials like ores and minerals from storage bins to processing equipment, improving operational efficiency and reducing downtime.
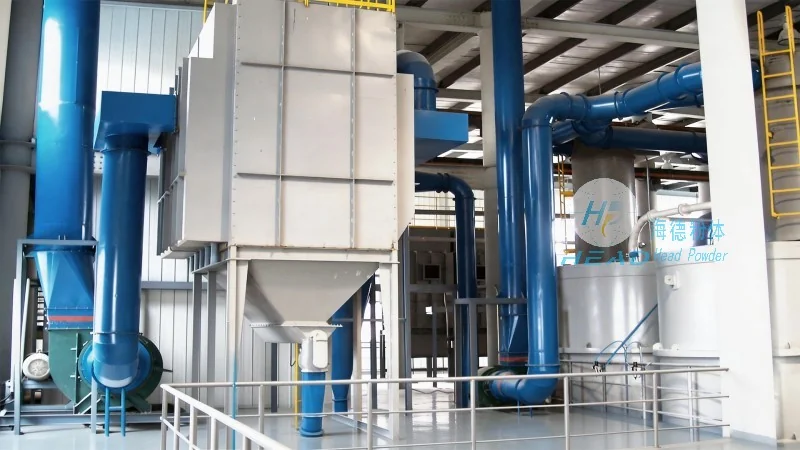
Advantages and Benefits
High-pressure bin pump pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. One of the main benefits is the ability to transport materials over long distances with minimal energy consumption. The systems are also more flexible, as they can be easily reconfigured to accommodate changes in production processes or material types. Additionally, the lack of moving parts reduces maintenance requirements and extends the lifespan of the equipment. The high-pressure operation ensures that the material is conveyed at a consistent speed, which helps to prevent material degradation and improve product quality. Furthermore, the control systems allow for real-time monitoring and adjustment, enhancing operational safety and efficiency.
Conclusion
High-pressure bin pump pneumatic conveying systems are a reliable and efficient solution for material handling and transportation in various industrial applications. With their advanced design and robust performance, these systems provide consistent and high-quality material transport, meeting the demands of modern industrial production. HeadPowder, as a leading manufacturer in this field, continues to innovate and improve its products to meet the evolving needs of the industry. By leveraging the principles of high-pressure air flow and advanced control systems, these pumps offer a cost-effective and sustainable solution for bulk material transport.