

Working Principle and Characteristics of Ammonia Fertilizer Powder Pneumatic Conveying
Ammonia fertilizer powder pneumatic conveying is a critical technology in the agricultural and chemical industries, designed to efficiently transport granular or powdered ammonia-based fertilizers. This method leverages the principles of fluidization and air movement to move bulk materials over long distances with minimal mechanical wear and energy consumption. The process involves several key components and steps that ensure reliable and safe material handling.
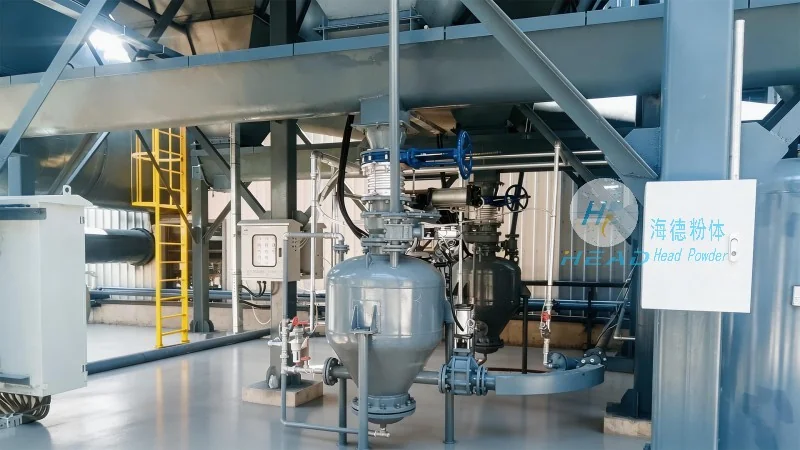
Working Principle of Ammonia Fertilizer Powder Pneumatic Conveying
The core mechanism of ammonia fertilizer powder pneumatic conveying is based on the creation of a high-velocity air stream that entrains the fertilizer particles. The system typically consists of a hopper, a blower or compressor, a pipeline network, and a discharge point. As the fertilizer is released from the hopper, it falls into the pipeline where the high-pressure air from the blower is introduced. The air stream lifts and transports the powder through the pipeline by creating a suspension of particles in the air. This suspension is maintained by the continuous flow of air, ensuring that the fertilizer moves efficiently to the destination. The process is often categorized into two main types: dilute phase and dense phase conveying, each with distinct characteristics that affect performance and application.

Key Characteristics of Ammonia Fertilizer Powder Pneumatic Conveying Systems
Several notable characteristics define the effectiveness and advantages of ammonia fertilizer powder pneumatic conveying systems. First, the system offers a high degree of flexibility in terms of layout and distance. It can transport materials over long distances without the need for multiple transfer points, making it suitable for large-scale agricultural operations and industrial facilities. Second, the method minimizes material degradation and contamination. Unlike mechanical conveying systems, which may cause abrasion or mixing with other materials, pneumatic conveying maintains the purity and integrity of the ammonia fertilizer, which is crucial for maintaining its effectiveness as a nutrient source. Third, the system is highly efficient in terms of energy use. By optimizing the air velocity and pressure, the conveying process can achieve significant energy savings compared to traditional methods such as truck or belt transport. Additionally, the equipment is relatively simple and requires less maintenance, reducing operational costs over time.
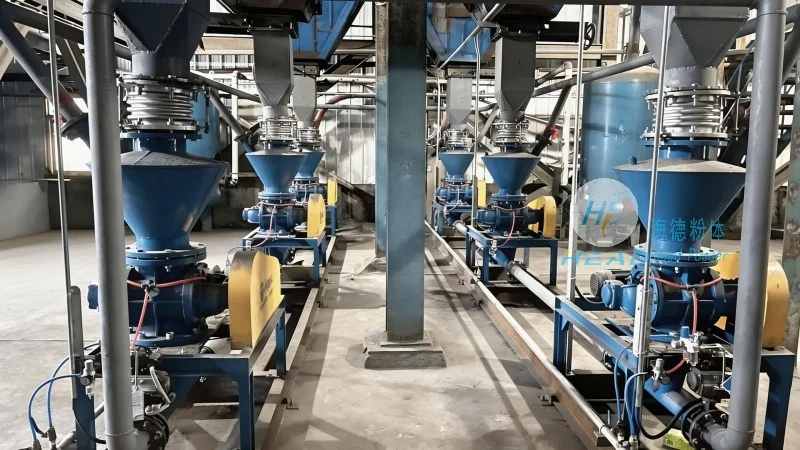
Applications and Advantages in Agricultural and Industrial Settings
Ammonia fertilizer powder pneumatic conveying is widely used in both agricultural and industrial contexts. In agricultural settings, it is employed to transport bulk ammonia-based fertilizers from storage facilities to application sites, such as farms or greenhouses. This method ensures that the fertilizer is delivered in a consistent and controlled manner, improving the efficiency of nutrient distribution and reducing waste. In industrial applications, the technology is used in chemical plants and manufacturing facilities to handle large quantities of powdered ammonia fertilizers, facilitating the production and processing of these materials. The advantages of this system, including its ability to handle high volumes, maintain material quality, and reduce operational costs, make it a preferred choice for many industries. Furthermore, the system's adaptability allows it to be integrated into existing infrastructure, making it a cost-effective solution for upgrading or expanding material handling capabilities.
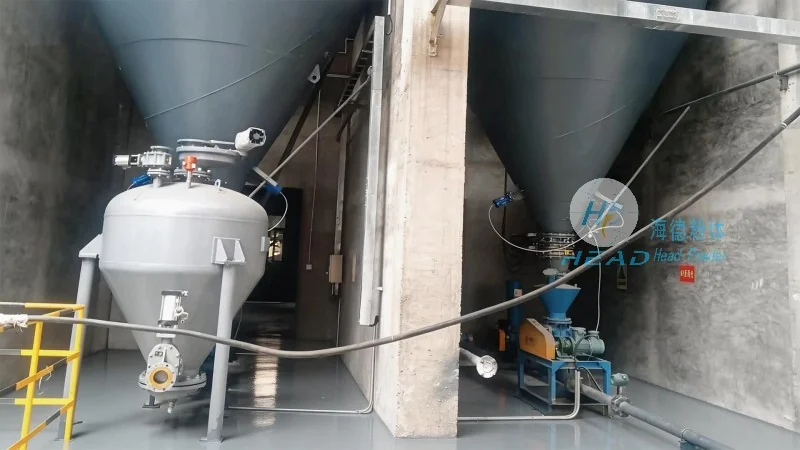
Conclusion and Company Overview
Ammonia fertilizer powder pneumatic conveying represents a sophisticated and efficient solution for the transportation of bulk ammonia-based fertilizers. By leveraging the principles of pneumatic transport, this technology offers significant benefits in terms of efficiency, material integrity, and operational flexibility. The system's ability to handle large volumes over long distances, combined with its low maintenance requirements and energy efficiency, makes it an attractive option for both agricultural and industrial sectors. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the specific needs of ammonia fertilizer handling. With a focus on quality and innovation, the company ensures that its products meet the highest standards of performance and reliability, supporting the efficient operation of fertilizer production and distribution networks.