

Working Principle and Features of Magnesium Oxide Material Handling Systems
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions for various industrial applications. This article delves into the working principles and distinctive features of magnesium oxide material handling systems, highlighting how these systems enhance operational efficiency and safety in industrial settings.
Working Principle of Magnesium Oxide Material Handling Systems
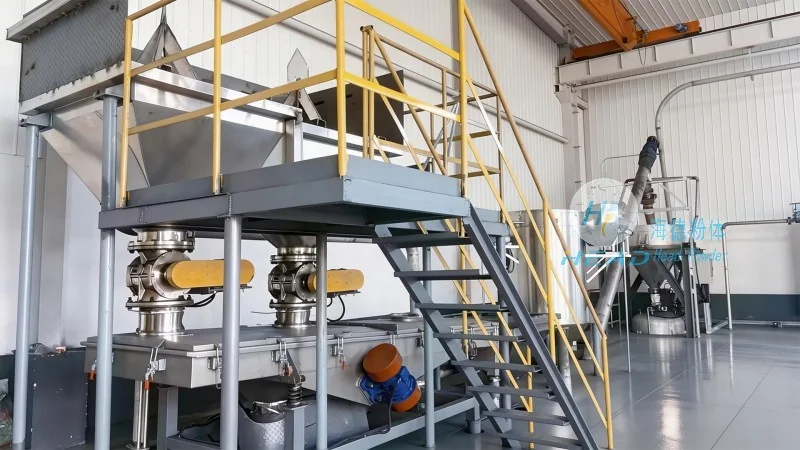
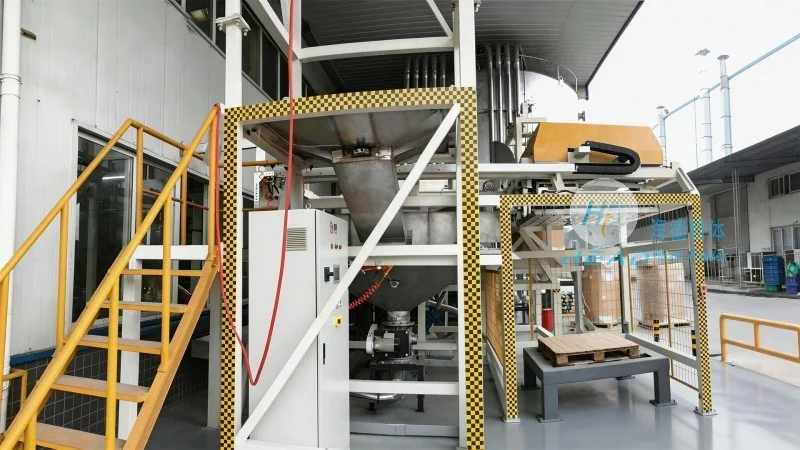
The core functionality of a magnesium oxide material handling system revolves around the efficient transport and management of magnesium oxide, a critical material used in multiple industries such as construction, chemical manufacturing, and pharmaceuticals. These systems typically integrate several key components, including conveyors, storage silos, and control panels, working in tandem to ensure seamless material flow. The process begins with the loading of magnesium oxide into a storage silo, where it is stored under controlled conditions to maintain quality and prevent caking. From the silo, the material is transferred to a conveyor system, which may include belt conveyors, screw conveyors, or pneumatic conveyors, depending on the specific requirements of the application. The conveyor system then transports the magnesium oxide to the processing or packaging area, where it is further handled by downstream equipment. Advanced control systems monitor the entire process, adjusting parameters like flow rate and pressure to optimize performance and prevent system downtime. This integrated approach ensures that the material is handled safely and efficiently, minimizing the risk of spills, dust emissions, and operational disruptions.
Key Features of Magnesium Oxide Material Handling Systems
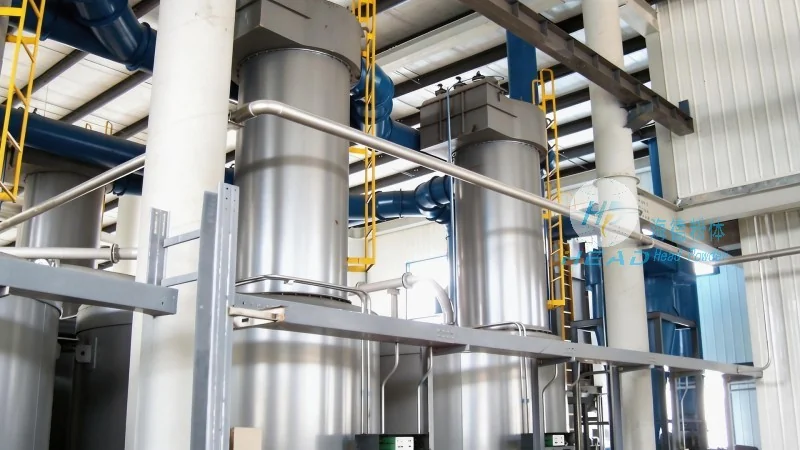
Magnesium oxide material handling systems from HeadPowder are characterized by several key features that set them apart in the industry. Firstly, they are designed with durability and reliability in mind, utilizing high-quality materials and robust construction to withstand the rigors of continuous industrial use. The systems are also equipped with advanced safety features, including dust suppression mechanisms, emergency stop buttons, and overload protection, ensuring compliance with safety regulations and protecting personnel and equipment. Another notable feature is the flexibility of these systems, which can be customized to accommodate different material types, flow rates, and operational requirements. This adaptability makes them suitable for a wide range of applications, from small-scale operations to large-scale industrial plants. Additionally, the integration of smart technology, such as sensors and data logging systems, allows for real-time monitoring and analysis of system performance, enabling proactive maintenance and improved operational efficiency. The systems also prioritize energy efficiency, incorporating energy-saving components and optimized designs to reduce operational costs and environmental impact. These features collectively contribute to the effectiveness and sustainability of magnesium oxide material handling systems, making them a preferred choice for industries seeking reliable and efficient material handling solutions.
Conclusion
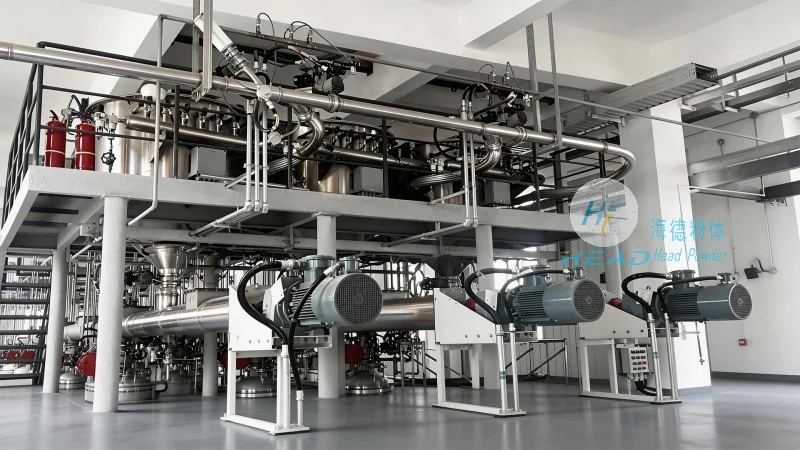
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers comprehensive magnesium oxide material handling systems that combine advanced technology, robust design, and superior performance. By understanding the working principles and key features of these systems, industrial clients can make informed decisions to enhance their operational efficiency, ensure safety, and achieve cost savings. The company's commitment to quality and innovation ensures that their material handling solutions meet the evolving needs of the industry, providing long-term value and reliability.