

What is a Crystalline Powder Conveying System Equipment? And What Are Its Design Principles?
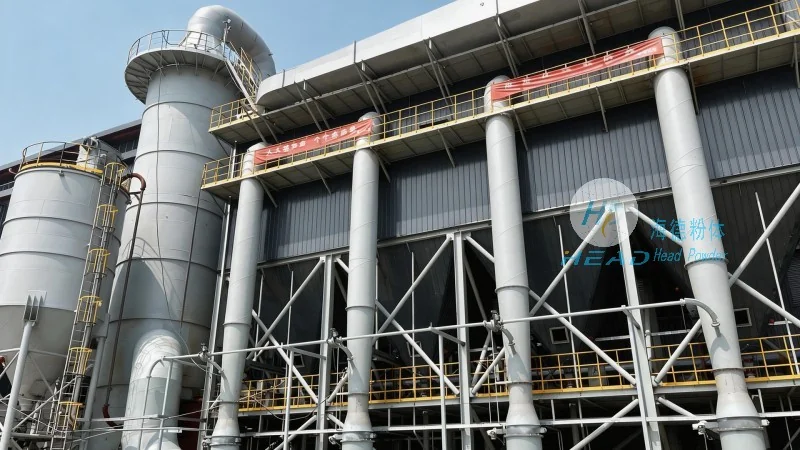
Crystalline powder conveying systems are specialized equipment designed to handle and transport crystalline powders efficiently. These systems are crucial in various industrial applications, including pharmaceuticals, chemicals, and food processing, where the precise movement of such powders is essential for maintaining product quality and operational efficiency.
Introduction to Crystalline Powder Conveying Systems
At the core of many industrial processes, crystalline powders require reliable and gentle handling to prevent degradation, caking, or loss of product integrity. A crystalline powder conveying system addresses these challenges by integrating advanced engineering solutions tailored to the unique properties of crystalline materials. These systems are engineered to ensure minimal product attrition, consistent flow rates, and optimal control over the conveying process, making them indispensable in industries where material quality is paramount.
Key Components of a Crystalline Powder Conveying System
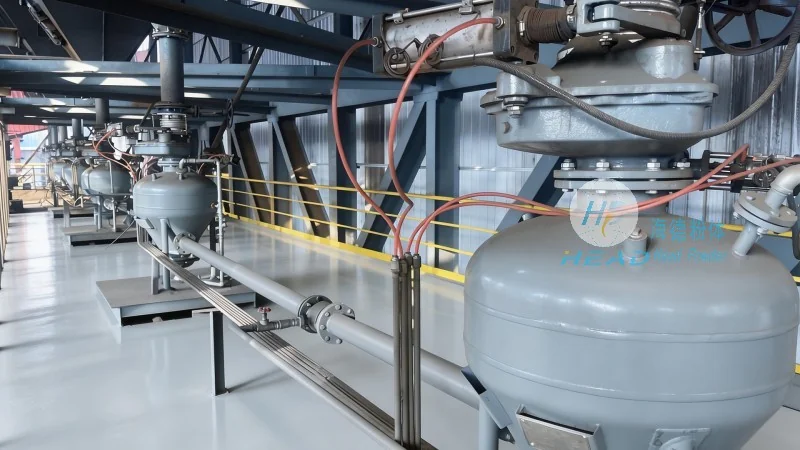
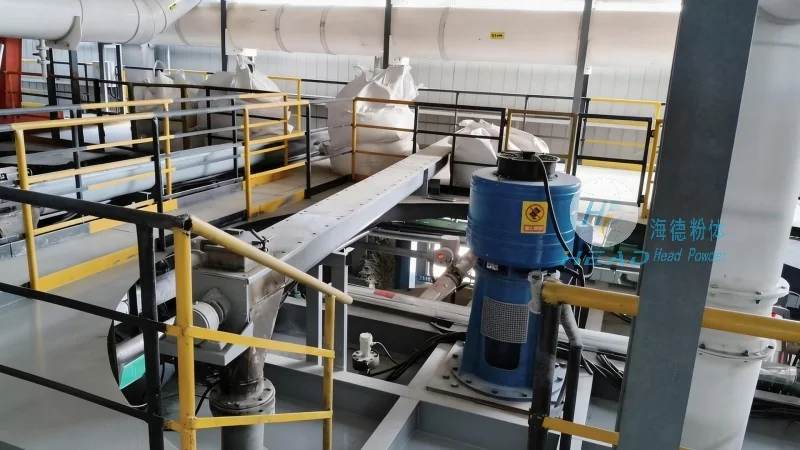
The design of a crystalline powder conveying system typically involves several critical components that work in harmony to achieve efficient material transport. These components include feed hoppers, which are designed to accommodate the bulk storage and controlled release of crystalline powders, often equipped with level sensors and flow control mechanisms to regulate the feed rate. The conveying mechanism itself, such as screw conveyors, pneumatic systems, or belt conveyors, is selected based on the specific characteristics of the powder, including particle size, density, and flowability. For crystalline powders, which may have cohesive or sticky properties, specialized conveying elements like flexible screw conveyors or air slides are often employed to prevent blockages and ensure smooth movement.
Design Principles for Efficient Crystalline Powder Conveying
The design principles of a crystalline powder conveying system are centered on minimizing stress on the material and maximizing operational reliability. One of the primary design considerations is the prevention of product degradation, which can occur due to excessive shear, impact, or temperature changes. To achieve this, the system incorporates gentle handling features, such as low-speed screw rotation, smooth internal surfaces, and temperature-controlled zones. Additionally, the system is designed with easy access for cleaning and maintenance, as crystalline powders can adhere to surfaces and require thorough sanitation to prevent cross-contamination. The integration of sensors and control systems allows for real-time monitoring of flow rates, pressure, and material levels, enabling operators to adjust the conveying process dynamically and maintain optimal performance.
Applications and Benefits of Crystalline Powder Conveying Systems
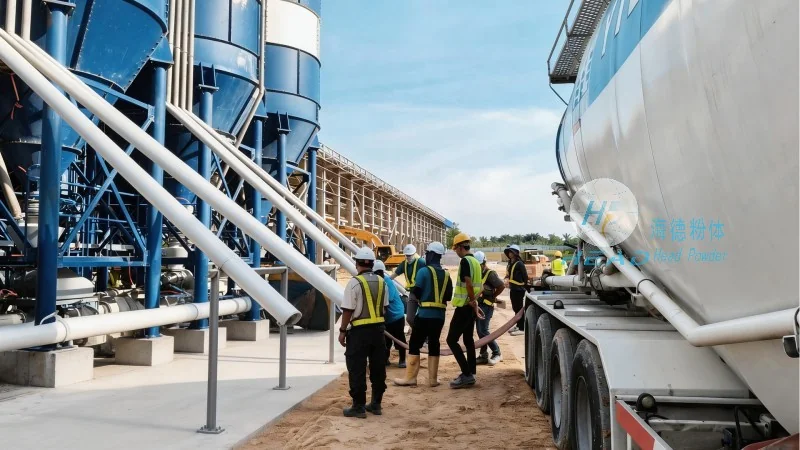
Crystalline powder conveying systems find widespread application in industries where the handling of fine, cohesive powders is critical. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final dosage forms meet stringent quality standards. In the chemical industry, they facilitate the transport of catalysts, reagents, and other crystalline chemicals, supporting continuous production processes. The benefits of such systems extend beyond material handling; they also contribute to improved safety by reducing manual handling of powders, enhancing workplace hygiene, and minimizing the risk of dust explosions through proper dust collection and containment systems.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer specializing in the design and production of advanced powder handling equipment. With a focus on innovation and customer-centric solutions, HeadPowder provides tailored crystalline powder conveying systems that meet the specific needs of various industries. HeadPowder's engineering team leverages years of experience in powder technology to develop systems that optimize material flow, reduce downtime, and enhance overall operational efficiency. The company is committed to delivering high-quality, reliable equipment that adheres to international standards, ensuring long-term performance and customer satisfaction.
Conclusion
In summary, a crystalline powder conveying system is a sophisticated piece of equipment designed to handle crystalline powders with precision and care. Its design principles prioritize gentle material handling, efficient transport, and operational reliability, making it an essential component in industries where product quality and process efficiency are non-negotiable. By understanding the key components and design principles of such systems, industries can select and implement the most suitable equipment to meet their specific requirements, ultimately enhancing their production capabilities and maintaining competitive advantages.