

What is Maltose Pneumatic Conveying Equipment? And What Are Its Design Principles?
Maltose pneumatic conveying equipment is a specialized system designed for the efficient transport of maltose, a key sugar in the food and beverage industry. This equipment utilizes air as the primary medium to move maltose particles from one location to another, offering a clean and effective solution for material handling. The design of such equipment is crucial for ensuring optimal performance, reliability, and safety in industrial applications.
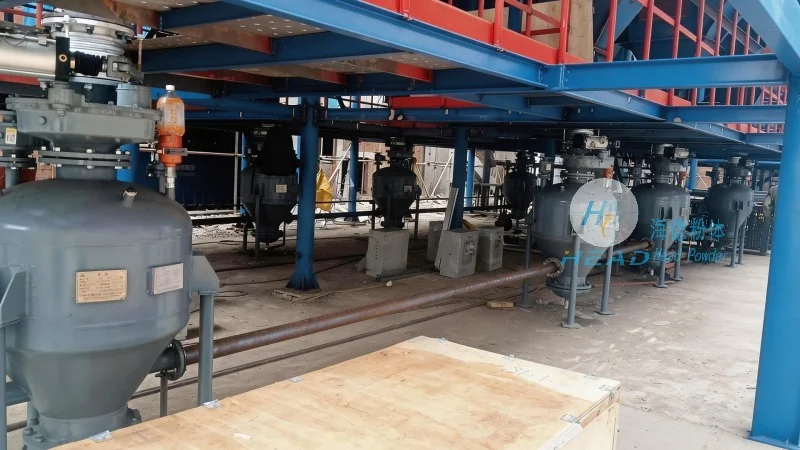
Key Components of Maltose Pneumatic Conveying Systems
The core components of a maltose pneumatic conveying system typically include a hopper for material storage, a conveyor line where the maltose is transported via air, and a receiver for the final delivery. Additionally, these systems may incorporate elements like air compressors, filters, and control valves to regulate the flow and pressure of the air, ensuring consistent and controlled movement of the maltose particles. Each component plays a vital role in the overall functionality and efficiency of the equipment.
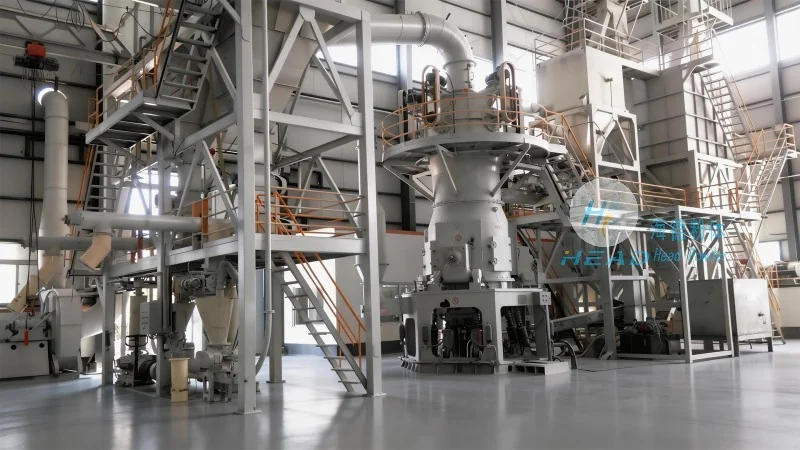
Design Principles Behind Maltose Pneumatic Conveying Equipment
The design principles of maltose pneumatic conveying equipment are centered around the principles of fluid dynamics and material handling. The system operates by creating a pressure differential between the inlet and outlet of the conveyor line. This differential is achieved through the use of air compressors, which generate the necessary airflow to lift and move the maltose particles. The design must consider factors such as particle size, density, and moisture content of the maltose, as these characteristics influence the air velocity required for effective transport. Furthermore, the equipment is engineered to minimize product degradation and contamination, which is critical in food processing applications.
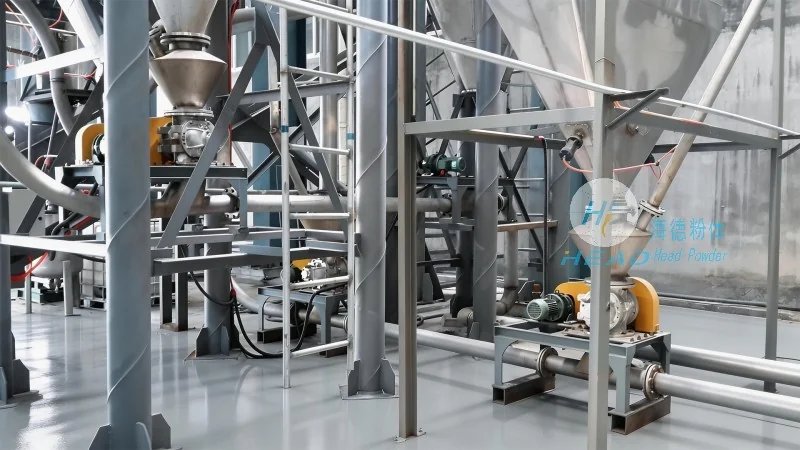
Advantages of Using Maltose Pneumatic Conveying Equipment
Implementing maltose pneumatic conveying equipment offers several advantages over traditional mechanical conveying methods. One of the primary benefits is the ability to handle maltose in a dust-free environment, reducing the risk of product contamination and improving workplace safety. The system also allows for flexible and compact installation, as it can be configured to fit into existing production layouts without requiring extensive structural modifications. Additionally, pneumatic conveying systems can handle a wide range of maltose particle sizes and flow rates, providing versatility in various industrial settings. The continuous operation of these systems also contributes to increased productivity and reduced downtime compared to batch processing methods.
Applications in the Food and Beverage Industry
Maltose pneumatic conveying equipment is widely used in the food and beverage industry, particularly in the production of beverages, baked goods, and confectionery products. In beverage manufacturing, it is used to transport maltose from storage silos to mixing tanks, ensuring a consistent supply of raw material. In the production of baked goods, the equipment helps in the efficient delivery of maltose to mixing and kneading processes. The equipment's ability to maintain product quality and hygiene makes it an ideal choice for applications where product purity is paramount. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, specialize in designing and manufacturing such equipment tailored to the specific needs of the food industry.
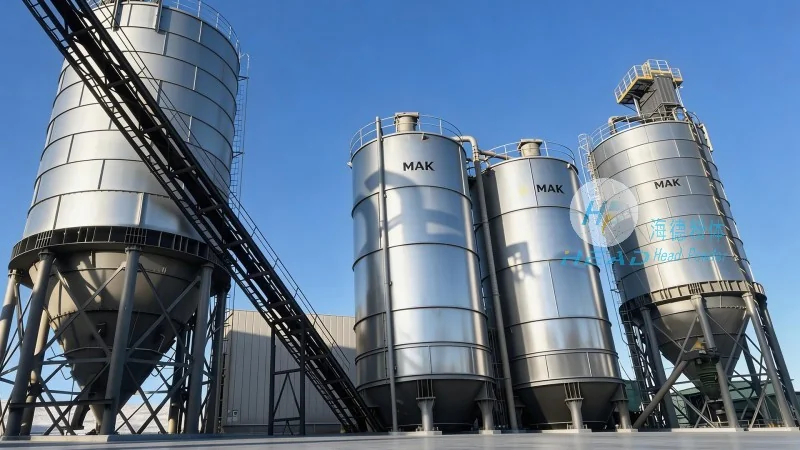
Conclusion and Company Overview
Maltose pneumatic conveying equipment represents a sophisticated solution for the efficient and safe handling of maltose in industrial settings. The design principles, which focus on fluid dynamics, material characteristics, and operational efficiency, ensure that the equipment performs reliably while maintaining product quality. The advantages of using such systems, including dust-free operation and flexibility, make them a preferred choice in the food and beverage industry. Shandong HeadPowder Engineering Co., Ltd., a company based in China, is dedicated to providing high-quality pneumatic conveying solutions tailored to the demands of the maltose processing industry, ensuring that clients receive equipment that meets both performance and regulatory standards.