

Technical Parameters and Conveying System for Sorghum Distiller's Grains
HeadPowder, a leading engineering firm based in Shandong, China, specializes in providing advanced solutions for the processing of sorghum distiller's grains. This article delves into the critical technical parameters and the efficient conveying system processes that are essential for optimizing the handling and utilization of this valuable byproduct in the distillation industry.
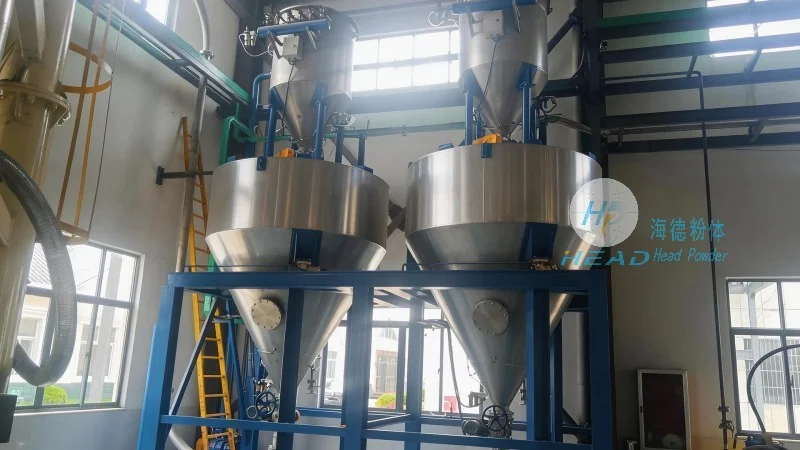
Key Technical Parameters of Sorghum Distiller's Grains
Sorghum distiller's grains are a nutrient-rich residue generated during the production of ethanol from sorghum. The technical parameters of these grains significantly influence their handling, storage, and downstream processing. Key parameters include moisture content, bulk density, particle size distribution, and ash content. For instance, moisture levels typically range from 60% to 80% depending on the drying process, while bulk density can vary between 0.5 to 0.8 g/cm³. Proper management of these parameters is crucial to prevent spoilage and ensure consistent quality. The particle size distribution, often characterized by a mix of fine and coarse fractions, affects the efficiency of conveying systems and downstream equipment such as mixers and pelletizers.
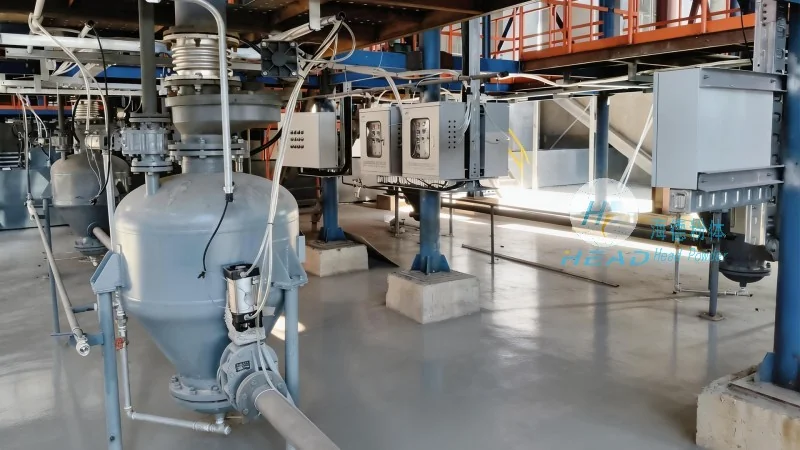
The Conveying System Process for Sorghum Distiller's Grains
Efficient conveying of sorghum distiller's grains is vital to maintain product integrity and operational efficiency in distillery operations. The conveying system typically involves a combination of mechanical and pneumatic methods tailored to the specific characteristics of the grains. Mechanical conveyors, such as belt conveyors and screw conveyors, are commonly used for horizontal and vertical transport due to their reliability and ability to handle high volumes. These systems are designed to minimize product degradation by reducing friction and impact. Pneumatic conveying, including positive and negative pressure systems, is employed for longer distances or when handling fine particles that are prone to dusting. The process begins with the collection of the grains from the distillation unit, followed by pre-processing steps like screening to remove foreign materials. The grains are then conveyed to storage silos or directly to downstream processing equipment such as feed mills or biogas digesters.
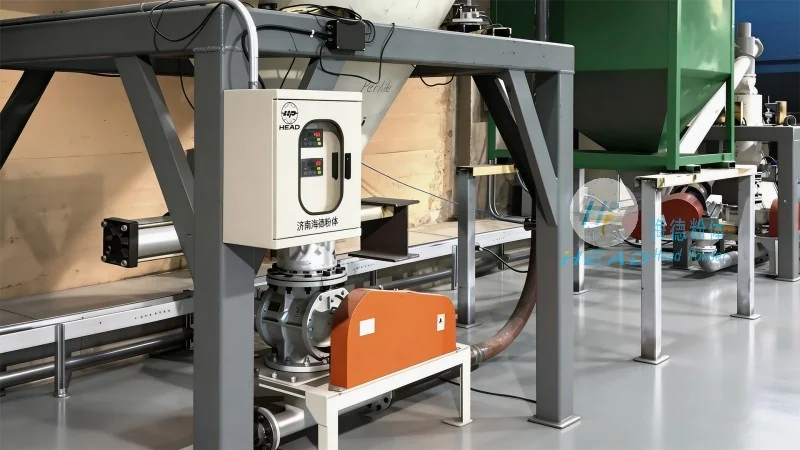
Engineering Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, offers comprehensive engineering solutions tailored to the unique requirements of sorghum distiller's grains handling. The company leverages its expertise in material handling and process engineering to design customized conveying systems that meet the specific technical parameters of the grains. Their solutions include advanced control systems, energy-efficient designs, and robust construction to ensure long-term reliability. By integrating state-of-the-art technology with practical application knowledge, HeadPowder helps distilleries optimize their operations, reduce costs, and enhance the overall value of sorghum distiller's grains as a feed ingredient or biofuel feedstock.
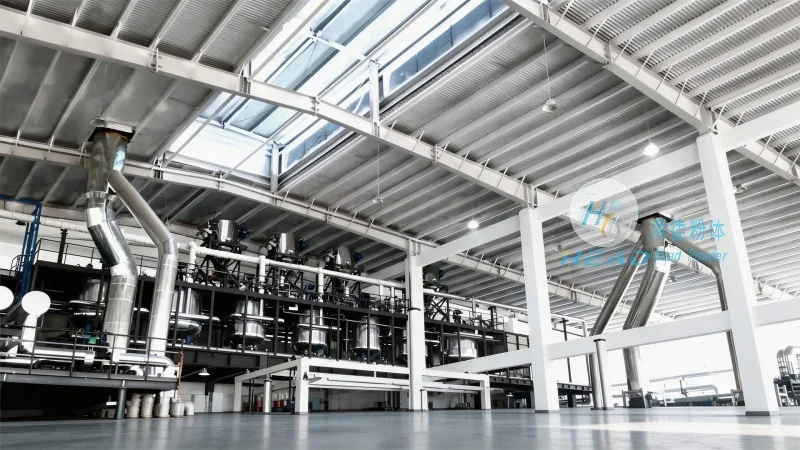
Conclusion and Application
In conclusion, the technical parameters of sorghum distiller's grains and the efficiency of the conveying system are interdependent factors that directly impact the performance of distillery operations. Proper understanding and management of these aspects are essential for maximizing the utilization of this valuable byproduct. With its headquarters in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing tailored engineering solutions that address the specific needs of the distillation industry, ensuring sustainable and efficient processing of sorghum distiller's grains.