

Principle and Working Scene Characteristics of Alumina Hydroxide Powder Pneumatic Conveying System
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. This article focuses on the principle and working scene characteristics of a pneumatic conveying system specifically designed for alumina hydroxide powder, a critical component in various industrial applications.
Introduction to Pneumatic Conveying Systems
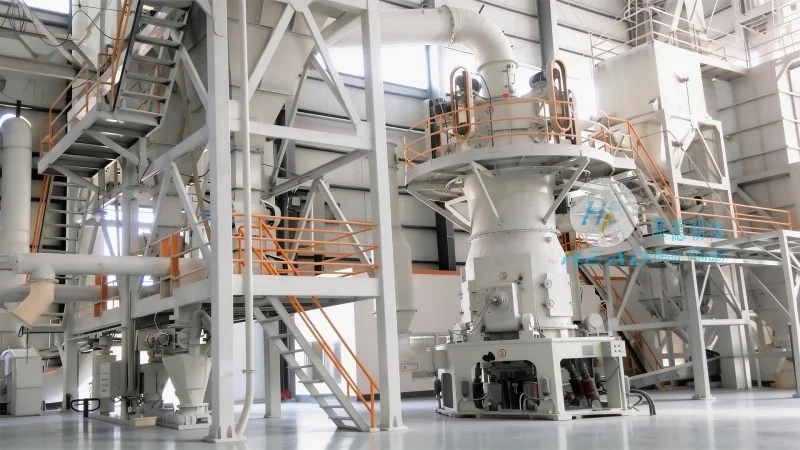
Pneumatic conveying systems utilize air or other gases to transport bulk materials like powders, granules, and small particles from one location to another. This method offers several advantages over traditional mechanical conveying, including reduced equipment wear, lower maintenance costs, and the ability to handle materials in a closed system, minimizing dust and contamination. The system typically consists of a hopper, a conveying line, a control valve, and a receiver, with the material being drawn or pushed through the system by the air flow.
Principle of Alumina Hydroxide Powder Pneumatic Conveying
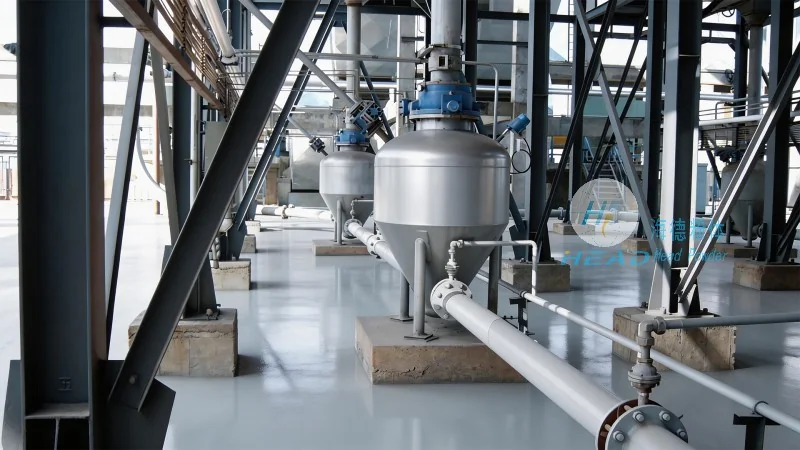
The core principle of the alumina hydroxide powder pneumatic conveying system is based on the creation of a stable and efficient air-solid flow. The system operates by introducing compressed air into the hopper, which lifts the powder particles and propels them through the conveying line. The key to successful operation lies in achieving the right air-to-solid ratio, which ensures that the powder remains suspended in the air stream without settling or clogging the system. This is achieved through precise control of air pressure, flow rate, and the design of the conveying line, including the use of appropriate bends, elbows, and expansion chambers to maintain flow stability.
Working Scene Characteristics of the System
The working scene characteristics of the alumina hydroxide powder pneumatic conveying system are tailored to meet the specific demands of industrial environments where this material is processed. These characteristics include high efficiency in material transport over long distances, minimal product degradation due to the closed system and gentle handling, and the ability to integrate with existing production lines without significant modifications. The system is particularly suitable for applications in the chemical, pharmaceutical, and ceramics industries, where the purity and quality of alumina hydroxide are critical. Additionally, the system's flexibility allows for adjustments in conveying capacity and speed to accommodate varying production needs, ensuring optimal performance under different operational conditions.
Application Scenarios and Benefits
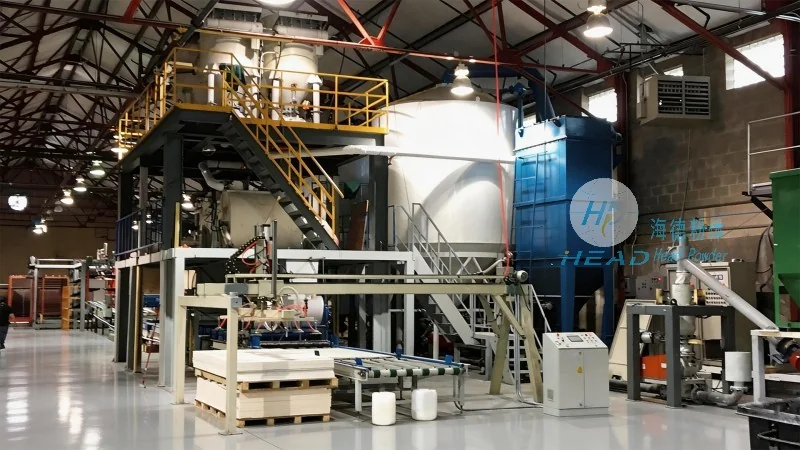
The alumina hydroxide powder pneumatic conveying system is widely used in various industrial settings, including chemical plants, where it is used to transport raw materials to processing units, and in pharmaceutical manufacturing facilities, where it is used to move ingredients to mixing and packaging areas. The benefits of this system extend beyond efficient material transport; it also contributes to improved workplace safety by containing dust and preventing exposure to airborne particles. Furthermore, the system's ability to handle large volumes of material in a compact and space-saving design makes it an ideal solution for facilities with limited floor space. The consistent and reliable performance of the system ensures that production processes remain uninterrupted, leading to increased productivity and reduced downtime.
Conclusion
In conclusion, the alumina hydroxide powder pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and efficient solution for the transportation of this critical material. By understanding the principle of air-solid flow and implementing advanced control technologies, the system ensures optimal performance, reliability, and safety in industrial applications. The working scene characteristics and benefits of this system make it a preferred choice for industries that demand high-quality material handling solutions, contributing to enhanced operational efficiency and product quality.