

Principle and Working Scene Characteristics of Vacuum Suction Type Material Handling Equipment
HeadPowder, a leading manufacturer in the material handling industry, specializes in vacuum suction type equipment designed to efficiently transport bulk materials. This article explores the fundamental principles behind this technology and highlights key working scene characteristics that make it an ideal solution for various industrial applications.
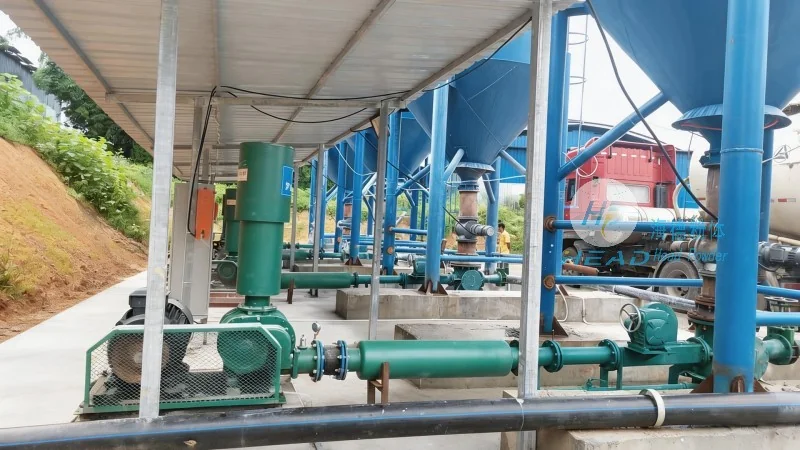
Understanding the Vacuum Suction Principle
The core of vacuum suction material handling equipment lies in creating a negative pressure environment. By using a vacuum pump or other vacuum generation systems, the equipment draws material from a source into a collection system or directly to a processing unit. This method eliminates the need for mechanical conveyors, reducing friction and wear while minimizing material degradation. The vacuum system ensures that materials are transported in a sealed, controlled manner, preventing contamination and dust dispersion. This principle is particularly effective for handling fine powders, granules, and other loose bulk materials that are prone to segregation or degradation under traditional conveying methods.
Key Working Scene Characteristics
One of the most significant advantages of vacuum suction equipment is its adaptability to diverse working environments. The system can operate over long distances, often exceeding 100 meters, making it suitable for large-scale industrial facilities where material transport between different sections is required. The sealed conveying process ensures that the material remains contained, reducing the risk of environmental contamination and improving workplace safety. This is especially crucial in industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and regulatory compliance are paramount.
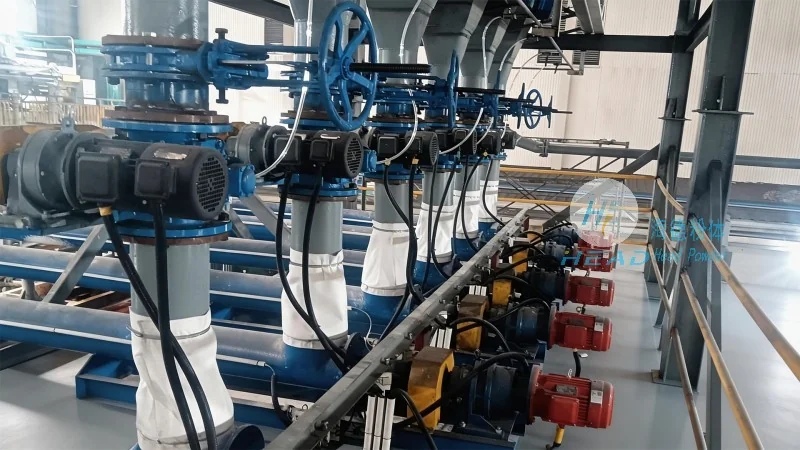
Another notable characteristic is the flexibility in handling different material types. Whether dealing with dry powders, wet granules, or even mixed materials, the vacuum suction system can be adjusted to accommodate varying particle sizes and flow properties. The equipment's design allows for easy integration with existing production lines, minimizing downtime during installation and operation. This adaptability makes it a versatile solution for companies looking to enhance their material handling efficiency without significant infrastructure changes.
Application in Industrial Settings
HeadPowder's vacuum suction material handling equipment has been successfully implemented in a wide range of industrial settings. In the chemical industry, it is used to transport raw materials and finished products, ensuring a clean and efficient workflow. The pharmaceutical sector benefits from the equipment's ability to maintain sterile conditions, as the sealed system prevents cross-contamination. Similarly, in food processing plants, the vacuum suction method preserves the quality and freshness of ingredients, meeting stringent hygiene standards. These applications demonstrate the equipment's reliability and effectiveness in high-demand environments where precision and safety are critical.
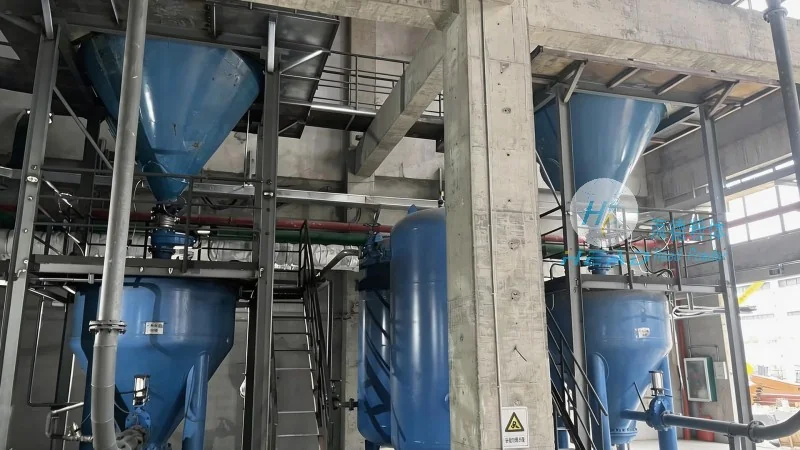
Advantages Over Traditional Conveying Methods
Compared to traditional mechanical conveyors, vacuum suction systems offer several distinct advantages. The absence of moving parts reduces maintenance costs and extends the equipment's lifespan. Additionally, the sealed operation minimizes energy consumption by preventing air leakage and reducing the need for additional filtration systems. This results in lower operational costs and a more sustainable approach to material handling. Furthermore, the system's ability to handle fine powders without clogging or blockages makes it superior to methods like screw conveyors or belt conveyors, which are prone to material buildup and maintenance issues.
Conclusion
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to innovate in the field of vacuum suction material handling equipment. By leveraging advanced vacuum technology and robust engineering, the company provides solutions that enhance productivity, improve safety, and ensure compliance with industry standards. The working scene characteristics of this equipment, including its adaptability, efficiency, and environmental benefits, make it a valuable asset for businesses seeking to optimize their material handling processes. As industries evolve, the demand for reliable and sustainable material transport solutions will only increase, and vacuum suction equipment remains at the forefront of meeting these needs.