

Principles and Application Scenarios of Dust-Free and Airtight Material Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free and airtight material conveying systems. These systems are engineered to handle various industrial materials while maintaining strict environmental standards, ensuring minimal contamination and efficient operation across diverse industrial applications.
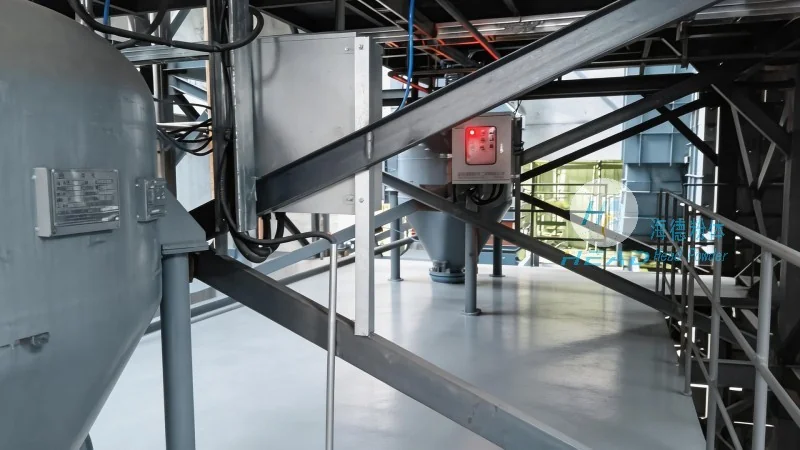
Understanding the Core Principles of Dust-Free and Airtight Conveying Systems
The fundamental principle behind dust-free and airtight material conveying equipment lies in creating a sealed environment that prevents the release of particulate matter into the surrounding air. This is achieved through a combination of robust construction materials, precise sealing mechanisms, and advanced control systems. The equipment typically features enclosed conveyor belts or pipes that transport materials from one location to another without exposing them to the external atmosphere. By maintaining a negative pressure or positive pressure differential within the system, these devices effectively contain dust and other airborne contaminants, ensuring compliance with industrial hygiene and environmental regulations.
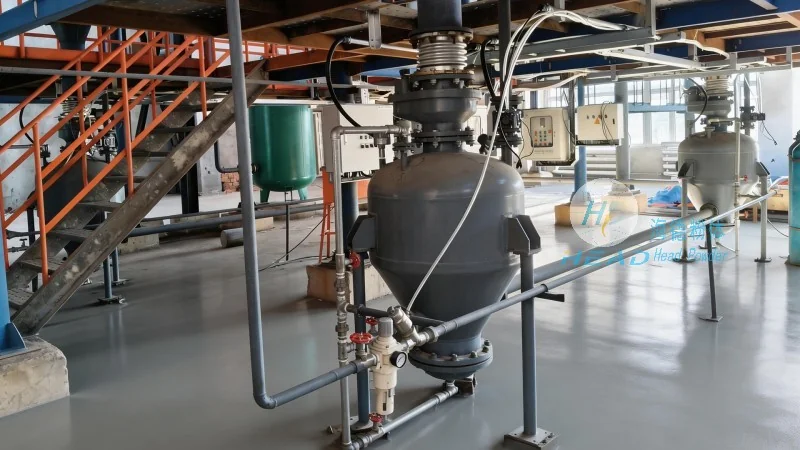
Key Components and Their Functions in the Conveying Process
Several critical components work in tandem to ensure the smooth and efficient operation of dust-free conveying systems. The primary components include the feeding hopper, which introduces materials into the system; the conveyor mechanism, such as a belt or screw, which transports the material; and the discharge outlet, which delivers the material to its final destination. Sealing elements, like gaskets and O-rings, are strategically placed at joints and connections to prevent air leakage and dust escape. Additionally, the system may incorporate filtration units to capture any residual particles before they are released into the environment. Control panels with programmable logic controllers (PLCs) allow operators to monitor and adjust the system's parameters, such as speed and pressure, to optimize performance and maintain consistent material handling.
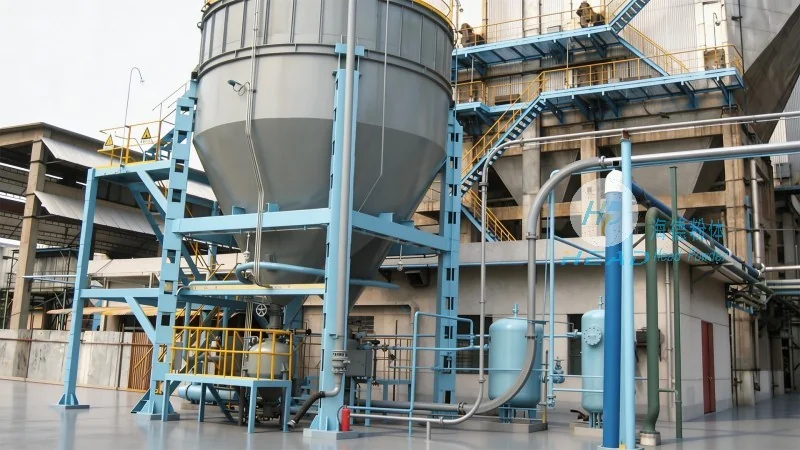
Application Scenarios and Industry-Specific Benefits
Dust-free and airtight material conveying equipment finds extensive application across multiple industries, each benefiting from the system's ability to maintain cleanliness and operational efficiency. In the pharmaceutical and food processing sectors, these systems are essential for handling powders and granules without cross-contamination, ensuring product purity and safety. The chemical industry utilizes them to transport hazardous or reactive materials, minimizing the risk of exposure and environmental impact. In the electronics manufacturing industry, the equipment helps maintain a cleanroom environment by preventing dust particles from entering sensitive production areas. Furthermore, in the cement and mining industries, these systems enhance material handling efficiency while reducing dust-related health hazards for workers.
Customization and Adaptability for Diverse Material Handling Needs
HeadPowder recognizes that different industries and applications have unique material handling requirements. Therefore, the company offers customized solutions tailored to specific needs. Customers can choose from various conveyor types, including belt conveyors, screw conveyors, and pneumatic conveying systems, depending on the material's characteristics and the desired transport method. The equipment can be adapted to handle a wide range of materials, from fine powders to bulk granules, and can be integrated with existing production lines or new facilities. Additionally, the systems can be equipped with sensors and monitoring tools to provide real-time data on material flow, temperature, and pressure, enabling proactive maintenance and process optimization.
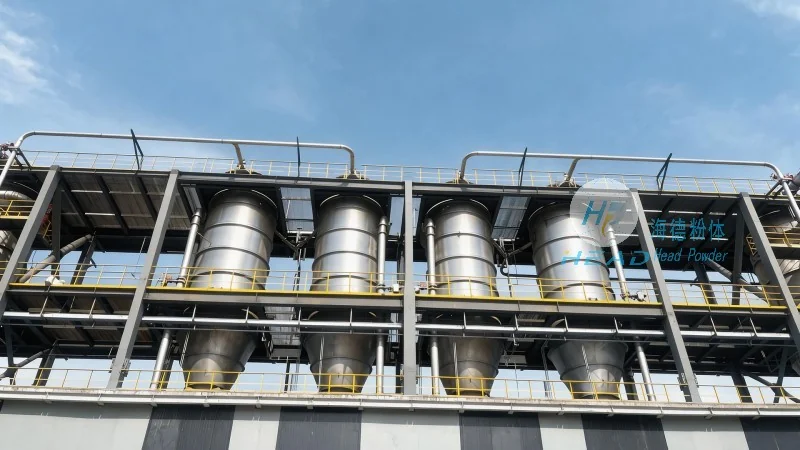
Ensuring Compliance and Long-Term Reliability
HeadPowder's dust-free and airtight conveying systems are designed to meet or exceed industry standards and regulatory requirements. The company adheres to strict quality control measures throughout the manufacturing process, ensuring that each component is built to withstand the rigors of industrial use. Regular maintenance and inspection protocols are recommended to maintain the system's performance and longevity. By investing in reliable equipment from HeadPowder, businesses can achieve consistent material handling, reduce operational downtime, and enhance overall productivity while adhering to environmental and safety regulations.