

Principles and Working Scene Characteristics of Glucose Powder Conveying Lines
Glucose powder conveying lines are critical industrial systems engineered to transport fine glucose particles efficiently and safely. These systems are indispensable in sectors such as pharmaceuticals, food processing, and chemicals, where precise handling of powders is essential to maintain product quality and operational efficiency. Understanding the underlying principles and the distinct working scene characteristics of these lines is vital for optimizing production workflows and ensuring compliance with industry standards.
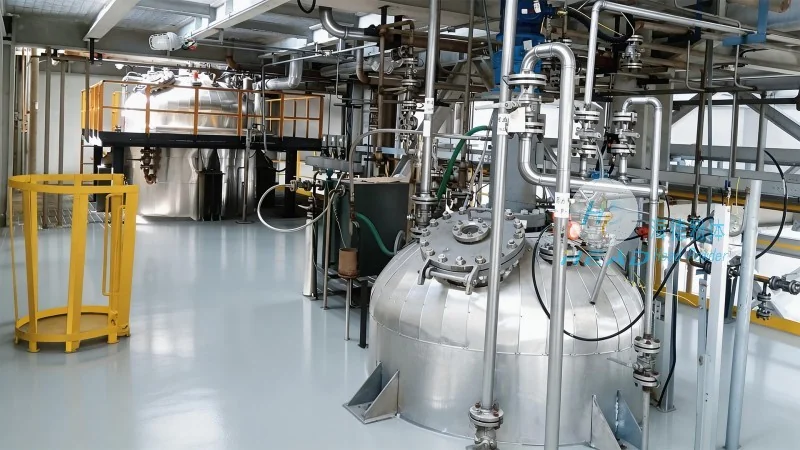
Core Principles of Glucose Powder Conveying Systems
The fundamental principles of glucose powder conveying lines revolve around the seamless transfer of fine particles from a source to a destination. Key components typically include feeders, conveyors, and control mechanisms that work in concert to maintain consistent flow rates and prevent material degradation. The design often incorporates dust suppression, temperature regulation, and material separation technologies to preserve the integrity of the glucose powder throughout the process. For instance, positive pressure or vacuum systems may be employed based on application requirements, providing flexibility for diverse operational environments. Advanced materials and engineering ensure durability and minimal product loss, making these systems reliable for continuous production.
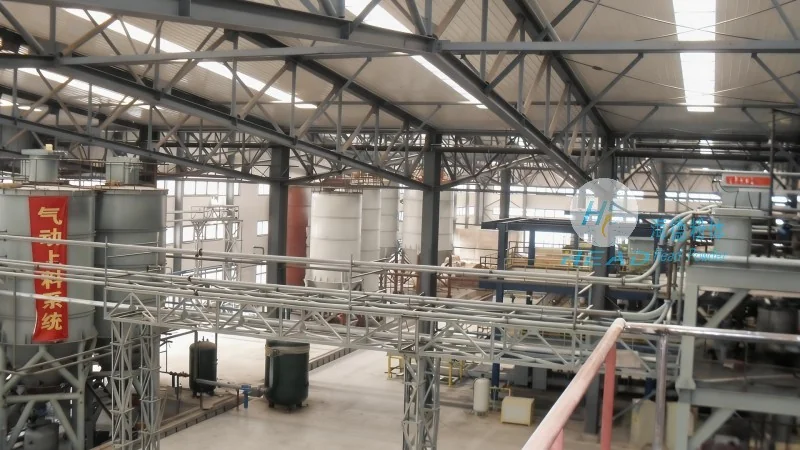
Working Scene Characteristics and Application Scenarios
Glucose powder conveying lines are deployed across various industrial settings, each with unique characteristics that influence system design and operation. In pharmaceutical manufacturing, these lines are crucial for transporting glucose powder used in oral medications and injectables. The working scene demands high-purity equipment and stringent contamination control to meet regulatory mandates. Similarly, in the food industry, glucose powder conveying lines are integral to confectionery production, where powder consistency directly impacts final product quality. Food processing environments often require high throughput and easy-to-clean designs to adhere to hygiene regulations. Chemical industries may utilize these systems for bulk handling of glucose-based raw materials, emphasizing safety and material compatibility.
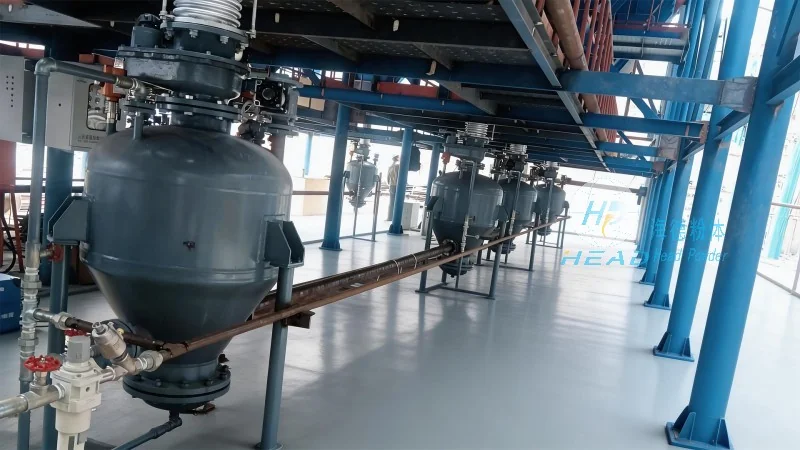
Technical Advantages and Operational Efficiency
Modern glucose powder conveying lines from Shandong HeadPowder Engineering Co., Ltd. leverage advanced technologies to enhance performance and reliability. These systems minimize product degradation, reduce energy consumption, and improve process control. High-quality materials and precision manufacturing ensure long-term durability. Integration of automation and monitoring allows real-time parameter tracking, enabling operators to adjust settings dynamically and enhance safety by reducing manual handling risks. This results in increased productivity and operational stability.
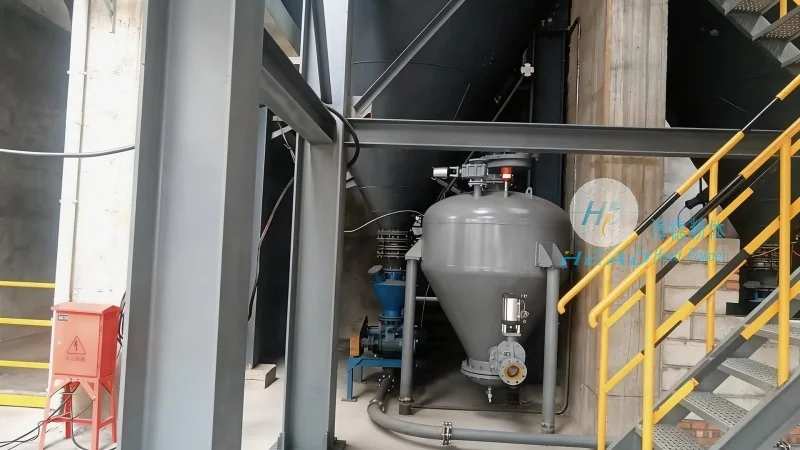
Company Profile and Industry Expertise
HeadPowder, a leading manufacturer of powder handling equipment, specializes in designing and producing customized glucose powder conveying lines. Headquartered in Shandong, China, the company has established a reputation for delivering innovative solutions tailored to diverse industry needs. The team comprises experienced engineers and technicians with deep expertise in powder technology and industrial applications. This expertise enables the development of bespoke systems addressing unique client challenges in pharmaceutical, food, and chemical sectors. The company adheres to international quality standards and continuously improves its offerings, focusing on customer satisfaction and operational excellence.