

Principle and Working Scene Characteristics of Dry Pebble Powder Conveying Lines
Efficient and reliable material handling is a critical aspect of modern industrial operations, and the dry pebble powder conveying line represents a sophisticated solution designed to meet the demands of transporting bulk materials in various applications. This system is engineered to handle dry, granular materials such as pebbles, powders, and other similar substances with precision and minimal loss, making it an essential component in sectors ranging from mining and construction to chemical processing and environmental remediation.
Overview of Dry Pebble Powder Conveying Lines
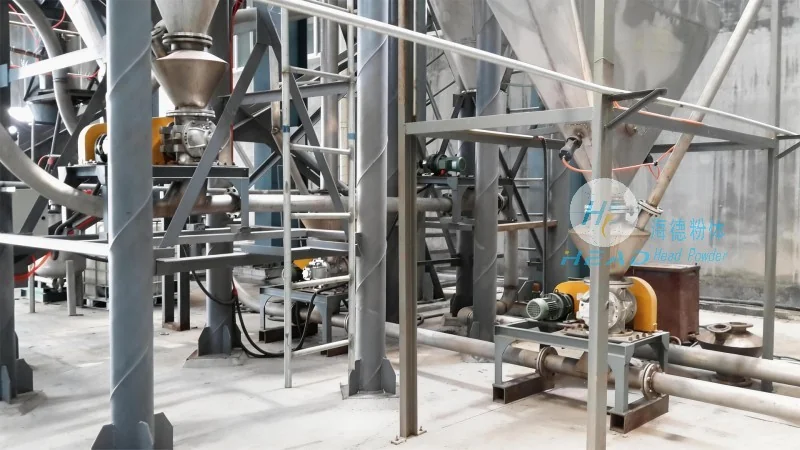
The dry pebble powder conveying line, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized system that integrates advanced technology to ensure seamless material transport. At its core, the system comprises several key components, including feeders, conveyors, control systems, and dust suppression mechanisms. Each component is meticulously designed to work in harmony, optimizing the overall performance and safety of the operation. The system is built to handle a wide range of particle sizes and material densities, making it versatile for diverse industrial needs.
Working Principle of the Conveying System
The operational principle of the dry pebble powder conveying line is centered on the use of air or mechanical force to move materials through a closed pipeline. The process begins with the material being fed into the system via a hopper or feeder, where it is then introduced into the conveying line. Depending on the specific design, the material may be transported using pneumatic systems (air pressure) or mechanical systems (e.g., screw conveyors or belt conveyors). The choice of method is determined by factors such as material characteristics, distance, and required throughput. In pneumatic systems, compressed air creates a flow that propels the material forward, while mechanical systems rely on rotating components to push the material along the pipeline. Both approaches are engineered to minimize material degradation and ensure consistent flow rates.
Key Features and Advantages
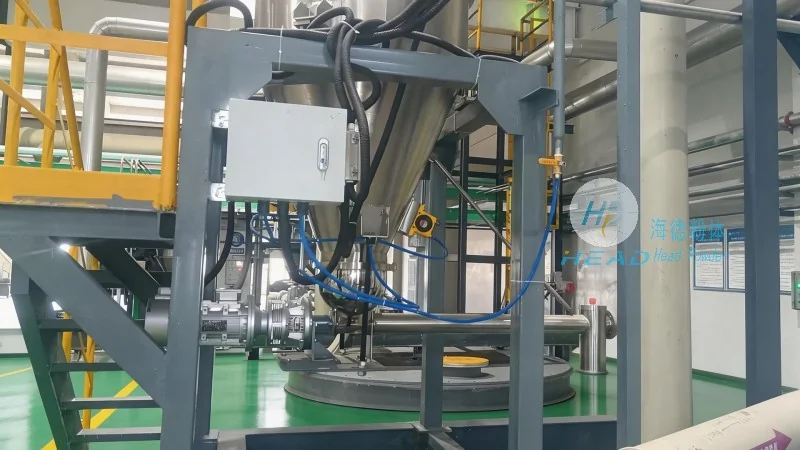
One of the primary advantages of the dry pebble powder conveying line is its ability to maintain material integrity during transport. Unlike traditional methods that may cause dust, segregation, or degradation, this system uses enclosed pipelines and controlled airflow to preserve the quality of the material. Additionally, the system offers high efficiency in terms of energy consumption and operational speed, allowing for rapid material movement over long distances. The design also incorporates safety features, such as dust suppression and overpressure protection, to ensure a secure working environment. The modular nature of the system enables easy integration with existing production lines and allows for scalability to accommodate increased production demands.
Application Scenarios and Industry Use Cases
The dry pebble powder conveying line is widely utilized across various industries due to its adaptability and efficiency. In the mining sector, it is employed to transport crushed rock and ore from processing plants to storage facilities or for further processing. In construction, the system is used to move aggregates, sand, and other construction materials to job sites, ensuring a steady supply of raw materials. The chemical industry benefits from the system's ability to handle powders and granules without contamination, which is crucial for maintaining product quality. Environmental remediation projects also utilize this technology to transport soil and other materials during cleanup operations. Each application leverages the system's ability to handle bulk materials with minimal human intervention, reducing labor costs and improving operational safety.
Customization and Integration Capabilities
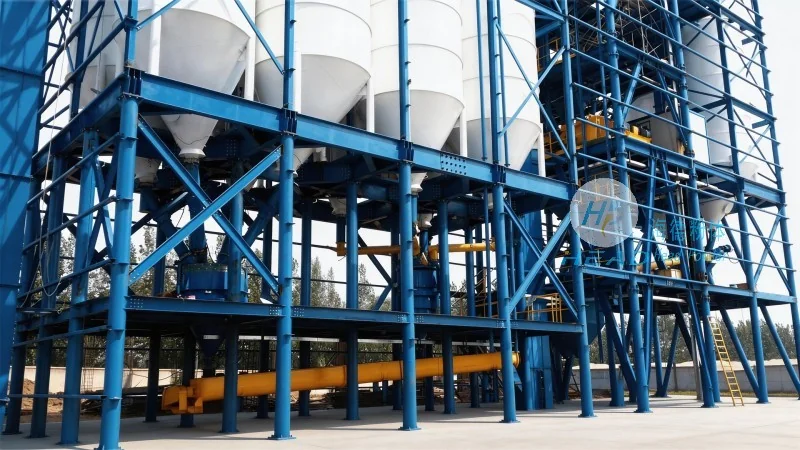
Shandong HeadPowder Engineering Co., Ltd. understands that industrial needs vary, and as such, offers customized solutions tailored to specific requirements. The company provides flexible design options, allowing clients to choose between pneumatic and mechanical systems based on their operational constraints. Additionally, the system can be integrated with existing equipment, such as crushers, screens, and storage silos, to create a comprehensive material handling solution. The engineering team at HeadPowder works closely with clients to assess their unique needs, ensuring that the final system meets all performance and safety standards. This approach results in a tailored solution that maximizes efficiency and minimizes downtime.
Conclusion and Company Information
The dry pebble powder conveying line is a robust and efficient solution for bulk material transport, offering significant advantages over traditional methods. By leveraging advanced technology and meticulous engineering, this system ensures reliable operation, material integrity, and operational safety. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and deliver high-quality conveying systems that meet the evolving demands of modern industry. With its headquarters in Shandong, China, the company remains committed to providing reliable and effective solutions for material handling challenges worldwide.