

Principle and Working Scene Characteristics of Maltose Powder Conveying System
HeadPowder, a leading provider in the field, specializes in advanced powder handling solutions tailored for industries dealing with maltose and other fine powders. This article explores the fundamental principles behind maltose powder conveying systems, alongside key working scene characteristics that define their application and effectiveness.
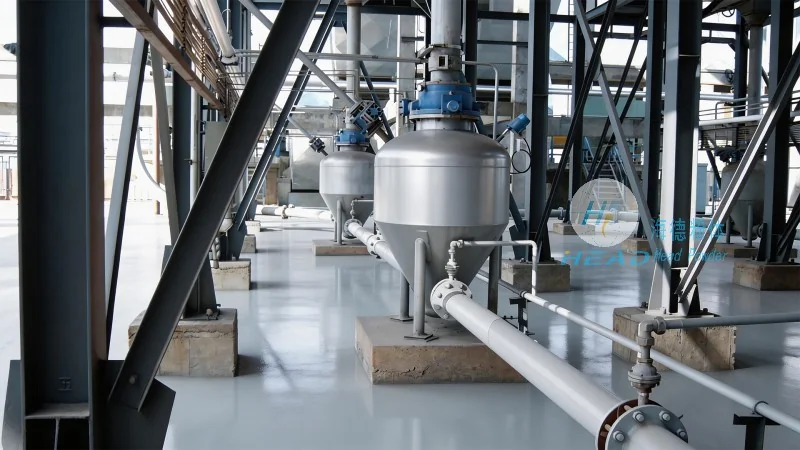
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating from Shandong, China, is dedicated to delivering innovative engineering solutions for powder processing. With a focus on precision and reliability, the company has established itself as a trusted partner for businesses requiring efficient maltose powder handling systems. The company’s commitment to quality and customer satisfaction drives its development of cutting-edge conveying technologies.
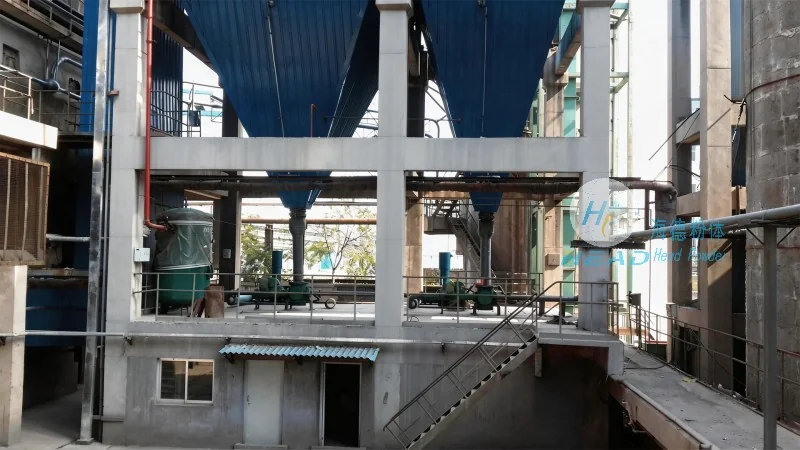
Principle of Maltose Powder Conveying Systems
The core principle of maltose powder conveying systems revolves around the efficient transfer of fine powders like maltose from one location to another. These systems typically employ mechanisms such as pneumatic conveying, screw conveyors, or bucket elevators, each designed to handle the unique properties of maltose—including its hygroscopic nature and fine particle size. The system’s design ensures minimal product degradation while maintaining high transfer efficiency. For instance, pneumatic conveying uses air to transport powder, reducing friction and preventing caking, which is crucial for maintaining maltose’s quality during handling.
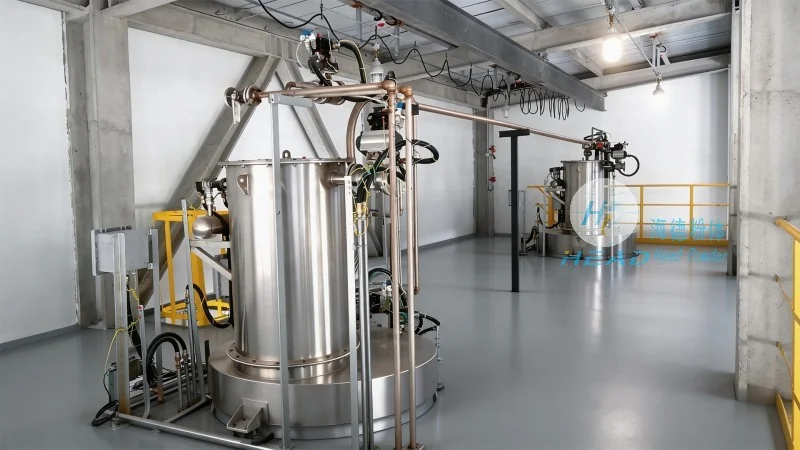
Working Scene Characteristics of Maltose Powder Conveying Systems
The working scene characteristics of maltose powder conveying systems are tailored to meet the specific demands of industrial applications. These systems are commonly used in food processing, pharmaceutical manufacturing, and chemical industries where maltose is a key ingredient. The key characteristics include:
- High Efficiency and Low Maintenance: Modern systems are engineered for continuous operation with minimal downtime, ensuring consistent production flow. This is achieved through robust components and advanced control systems that optimize the conveying process.
- Hygienic Design: Given maltose’s use in food and pharmaceutical sectors, the conveying systems are constructed with materials that meet strict hygiene standards. Stainless steel and food-grade components are commonly used to prevent contamination and ensure product safety.
- Customization for Diverse Applications: HeadPowder offers customized solutions to accommodate varying production scales and operational requirements. Whether for small-scale laboratory use or large-scale industrial production, the systems can be tailored to handle different maltose formulations and processing needs.
- Energy Efficiency: Advanced systems incorporate energy-saving features, such as variable speed drives and optimized air flow, reducing operational costs while maintaining performance. This is particularly important for industries focused on sustainability and cost management.
Key Features and Benefits
HeadPowder’s maltose powder conveying systems offer several key features that enhance operational performance and product quality. These include:
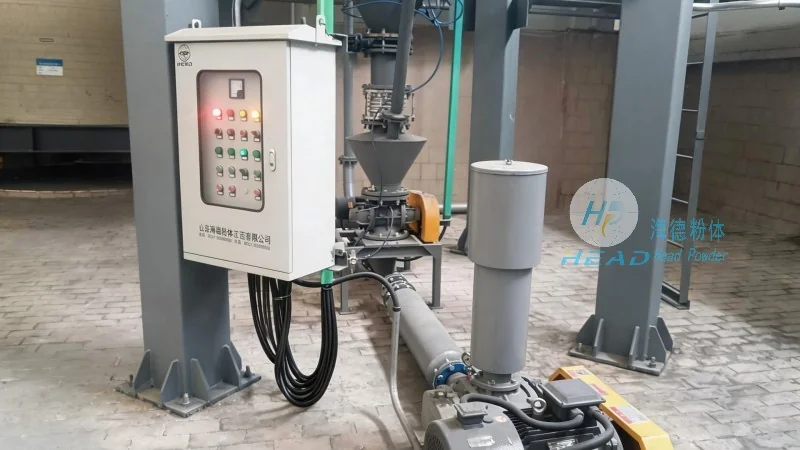
- Advanced Control Systems: Integrated control panels allow for real-time monitoring and adjustment of conveying parameters, ensuring optimal performance and preventing issues like overloading or clogging.
- Material Handling Flexibility: The systems are designed to handle a wide range of powder types, including maltose, with minimal adjustments. This flexibility makes them suitable for diverse applications and reduces the need for multiple specialized systems.
- Reduced Product Loss and Contamination: The enclosed design of the conveying systems minimizes product loss and exposure to contaminants, maintaining the purity and quality of maltose. This is critical for industries where product integrity is paramount.
- Easy Integration with Existing Facilities: The systems are engineered for seamless integration with existing production lines, minimizing installation time and disruption to operations. This allows businesses to upgrade their powder handling capabilities without major overhauls.
Conclusion
HeadPowder’s maltose powder conveying systems represent a reliable and efficient solution for industries requiring precise handling of maltose and similar fine powders. By leveraging advanced engineering principles and tailored design, these systems address the unique challenges of maltose processing while ensuring high performance, hygiene, and cost-effectiveness. For businesses seeking to enhance their powder handling capabilities, HeadPowder’s solutions provide a robust and adaptable option, supporting consistent production and product quality.