

Principle and Working Scene Characteristics of Limestone Powder Conveying Systems
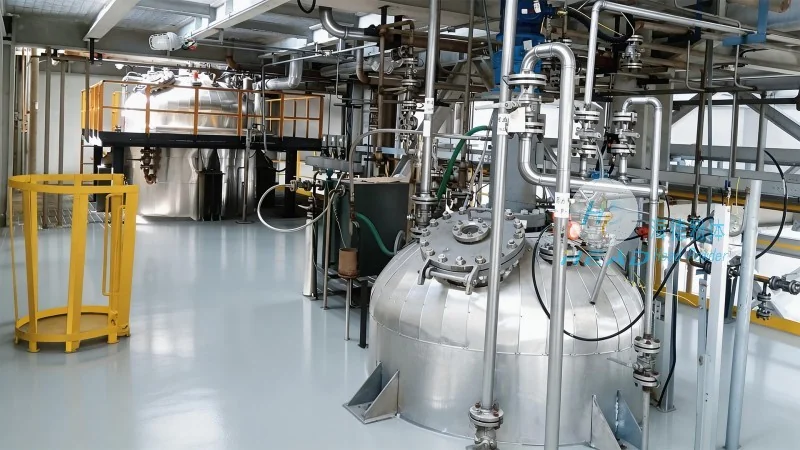
HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design and implementation of efficient limestone powder conveying systems. This article delves into the fundamental principles behind these systems and highlights the key characteristics of their operational environments.
Introduction to Limestone Powder Conveying Systems
Limestone powder, a crucial raw material in various industrial applications such as cement production, chemical processing, and environmental remediation, requires reliable and efficient transportation from storage to processing units. The limestone powder conveying system developed by Shandong HeadPowder Engineering Co., Ltd. addresses these needs through a combination of advanced engineering and robust technology. Based in China, the company leverages its local expertise and global standards to deliver tailored solutions that meet the specific demands of different industries.
Core Principles of the Conveying System
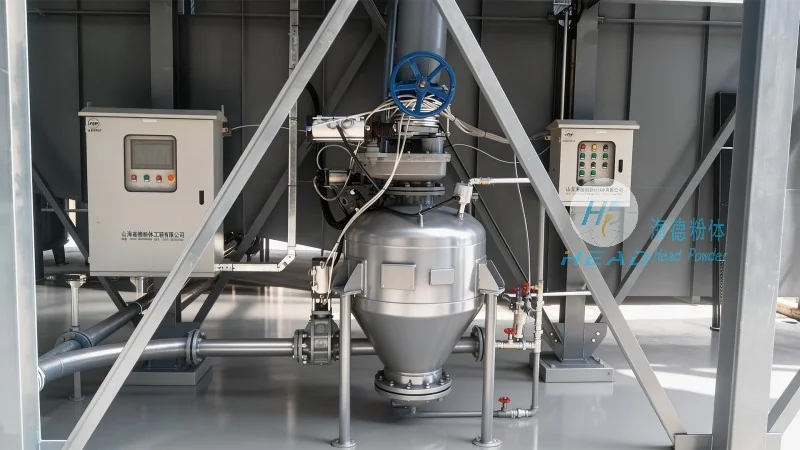
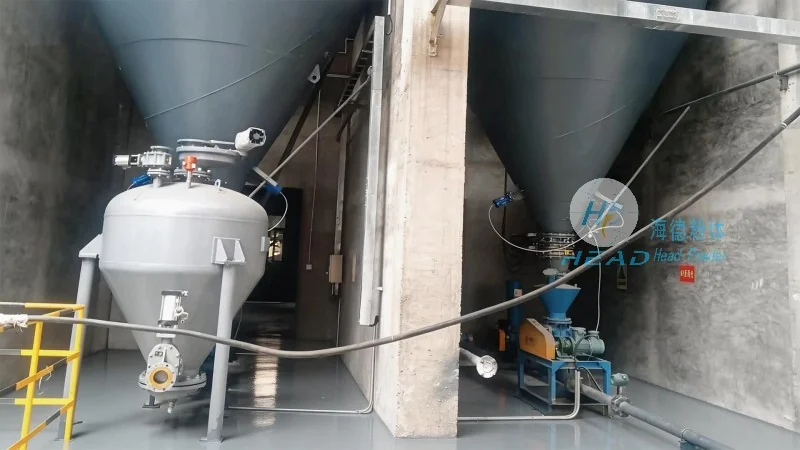
The limestone powder conveying system operates on the principle of pneumatic or mechanical transport, depending on the material characteristics and operational requirements. For limestone powder, which is typically fine and dry, pneumatic conveying is often preferred due to its ability to handle high volumes with minimal maintenance. The system comprises several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line (either flexible hose or rigid pipe), and a receiver for the material at the destination. The feeding mechanism ensures a consistent and controlled discharge of limestone powder, preventing blockages and ensuring smooth operation. The conveying line is designed to minimize material degradation and loss, with features like smooth inner surfaces and appropriate diameter to maintain the powder's integrity. The receiver is equipped with a dust collection system to comply with environmental regulations and ensure workplace safety.
Working Scene Characteristics and Applications
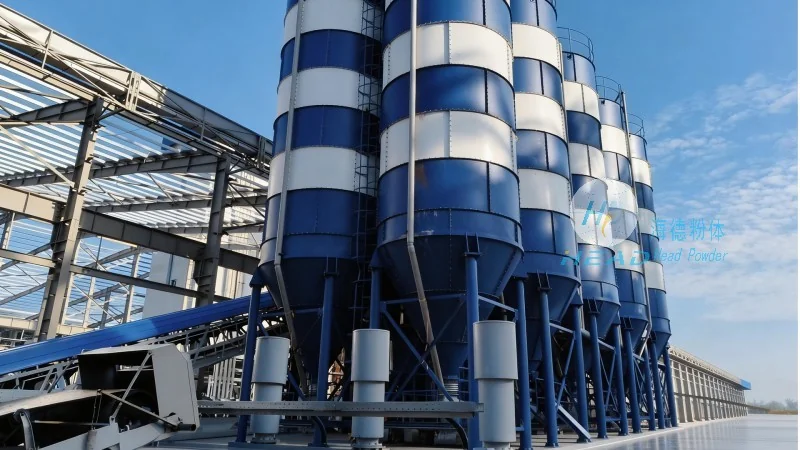
The operational environment of limestone powder conveying systems varies significantly based on the industry and application. In cement plants, for instance, the system must handle large quantities of limestone powder with high precision, often integrated with other raw material handling processes. The working scene is characterized by high throughput, continuous operation, and the need for integration with existing production lines. The system is designed to operate under varying ambient conditions, including temperature fluctuations and humidity, ensuring consistent performance. In chemical processing facilities, the limestone powder may be used as a neutralizing agent or in the production of calcium compounds, requiring the system to maintain strict material purity and avoid contamination. The working scene here emphasizes safety, as limestone powder can be a respiratory hazard if not handled properly, and the system incorporates dust suppression and filtration measures. Environmental remediation projects, such as flue gas desulfurization, also utilize limestone powder conveying systems, where the material is transported to reactors for sulfur removal. The working scene in these applications is often outdoors or in large industrial complexes, with the system designed for durability and resistance to corrosive elements.
Advantages and Key Features
Shandong HeadPowder Engineering Co., Ltd.'s limestone powder conveying systems offer several advantages that make them suitable for diverse industrial applications. The systems are designed for high efficiency, with low energy consumption and minimal material loss, which reduces operational costs and environmental impact. The modular design allows for easy installation and maintenance, with components that can be replaced or upgraded without disrupting the entire system. The company's expertise in material handling ensures that the systems are tailored to the specific properties of limestone powder, such as particle size distribution and moisture content, optimizing performance. Additionally, the systems are equipped with advanced control systems that provide real-time monitoring and feedback, enabling operators to adjust parameters for optimal performance. The working scene characteristics, including high throughput and continuous operation, are addressed through robust construction and reliable components, ensuring long-term durability and minimal downtime.
Conclusion
HeadPowder's limestone powder conveying systems exemplify the company's commitment to providing efficient, reliable, and sustainable solutions for industrial powder handling. By understanding the core principles of the system and the specific characteristics of the working environment, Shandong HeadPowder Engineering Co., Ltd. delivers tailored solutions that meet the needs of various industries. The systems are designed to enhance productivity, reduce costs, and ensure compliance with environmental regulations, making them a valuable asset for any industrial operation. With its headquarters in China, the company continues to innovate and provide cutting-edge solutions to meet the evolving demands of the market.