

What is a Fertilizer Powder Conveying System? What Are Its Design Principles?
Fertilizer powder conveying systems are critical components in the agricultural and industrial sectors, designed to transport bulk powder materials such as fertilizers, chemicals, and other granular substances efficiently and safely. These systems are essential for optimizing production processes, reducing labor costs, and ensuring consistent material flow in facilities ranging from small-scale farms to large-scale manufacturing plants. The core function of a fertilizer powder conveying system is to move powders from storage silos or production areas to processing units, packaging lines, or storage locations with minimal loss, contamination, and energy consumption.
Key Components of a Fertilizer Powder Conveying System
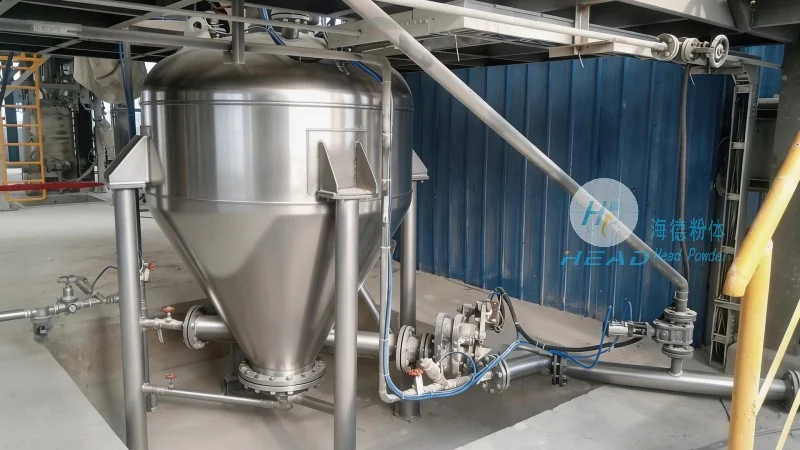
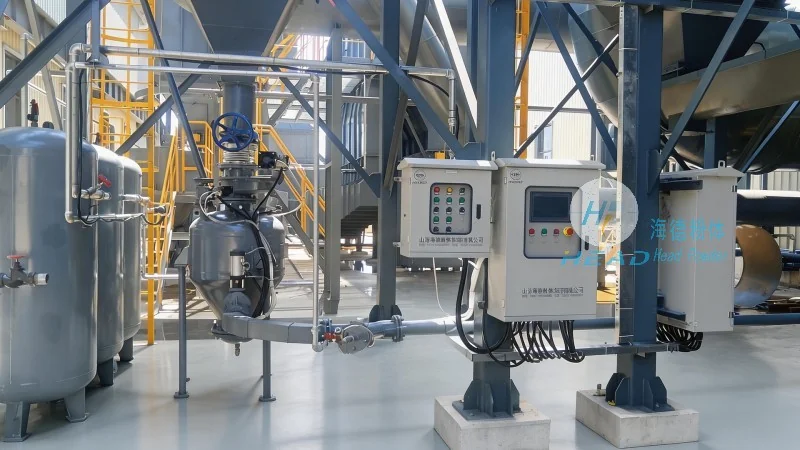
A typical fertilizer powder conveying system consists of several key components that work in tandem to achieve reliable material transport. The primary components include a hopper or silo for material storage, a feeder or metering device to control the flow rate of the powder, a conveying mechanism (such as a screw conveyor, pneumatic conveyor, or pneumatic duct system), and a control system to regulate the entire process. The hopper is designed to hold the bulk fertilizer and maintain a consistent head pressure, which helps in preventing material bridging or caking. The feeder, often a rotary valve or a screw feeder, ensures that the powder is discharged at a controlled rate, preventing overloading or underloading of the conveying system. The conveying mechanism is the heart of the system, responsible for moving the powder through the pipeline. For pneumatic systems, this involves using air pressure to create a flow of material, while mechanical systems rely on rotating screws or belts to push the powder forward. The control system, typically a PLC (Programmable Logic Controller), monitors and adjusts the flow rate, pressure, and other parameters to maintain optimal operation.
Design Principles for Efficient Powder Conveying
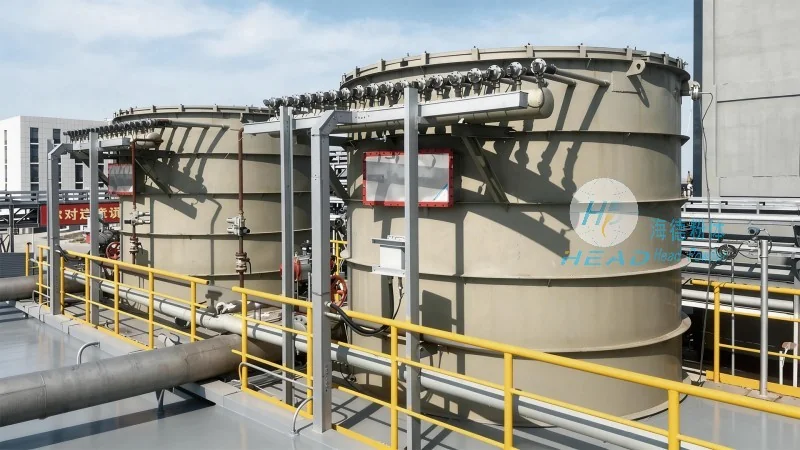
The design of a fertilizer powder conveying system is governed by several key principles aimed at maximizing efficiency, safety, and reliability. One of the most critical principles is the prevention of material degradation and contamination. This is achieved through proper sealing of the system, use of corrosion-resistant materials, and the incorporation of dust collection and filtration systems. The system must also be designed to handle the specific properties of the fertilizer, such as its moisture content, particle size distribution, and flowability. For example, cohesive or sticky fertilizers may require special hopper designs with agitators or vibrators to prevent caking. Another important design principle is energy efficiency. Modern systems often incorporate variable speed drives and optimized conveying paths to reduce energy consumption while maintaining the required flow rate. The system must also be designed for easy maintenance and cleaning, as fertilizers can be abrasive and may leave residue in the equipment. This includes features like easy-to-remove components, cleaning ports, and access panels.
Material Handling and Safety Considerations
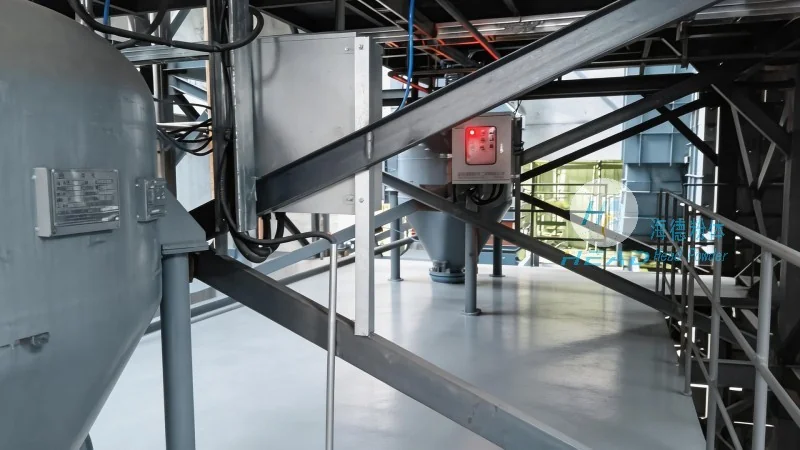
Material handling in fertilizer powder conveying systems involves several safety considerations to protect workers and the environment. The system must be designed to minimize dust emissions, as airborne particles can be hazardous to health and cause environmental pollution. This is typically achieved through the use of enclosed conveying lines, dust collection systems, and proper ventilation. The equipment must also be constructed from materials that are resistant to corrosion and wear, as fertilizers can be chemically aggressive. For example, stainless steel or coated steel components are commonly used in the construction of hoppers, conveyors, and valves. Additionally, the system must be equipped with safety features such as emergency stop buttons, pressure relief valves, and overload protection to prevent accidents and equipment damage. The design must also consider the potential for explosion hazards, especially with certain types of fertilizers that may be prone to dust explosions. This may involve incorporating explosion-proof components and using inert gases or other explosion suppression systems.
Applications and Industries Served by Fertilizer Powder Conveying Systems
Fertilizer powder conveying systems are used in a wide range of applications across various industries. In the agricultural sector, these systems are essential for moving bulk fertilizers from storage silos to farm fields or to processing facilities for blending and packaging. They are also used in the chemical industry for transporting raw materials and finished products, such as nitrogenous and phosphatic fertilizers. In the food and beverage industry, similar systems are used for handling powdered ingredients like sugar, flour, and vitamins. The versatility of fertilizer powder conveying systems makes them suitable for any application where bulk powder materials need to be transported efficiently and safely. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized fertilizer powder conveying systems tailored to the specific needs of each client. The company's expertise in material handling and engineering ensures that their systems are reliable, efficient, and compliant with industry standards.
Conclusion: The Importance of Proper Design and Implementation
In conclusion, fertilizer powder conveying systems are indispensable in modern industrial and agricultural operations. Their design and implementation must adhere to strict principles to ensure optimal performance, safety, and efficiency. By understanding the key components, design principles, and safety considerations, businesses can select and operate the most suitable system for their needs. Shandong HeadPowder Engineering Co., Ltd. offers comprehensive solutions for fertilizer powder conveying, combining advanced technology with expert engineering to meet the diverse requirements of the industry. Whether for small-scale farms or large-scale manufacturing plants, their systems provide reliable and efficient material transport, contributing to increased productivity and reduced operational costs.