

What is a Fertilizer Granule Pneumatic Conveying System Equipment? And What Are Its Design Principle
A fertilizer granule pneumatic conveying system is a specialized industrial equipment designed to transport granular fertilizer materials from one location to another using air as the conveying medium. This technology is widely used in the agricultural and chemical industries to efficiently move bulk fertilizer products with minimal human intervention and reduced risk of material degradation or contamination.
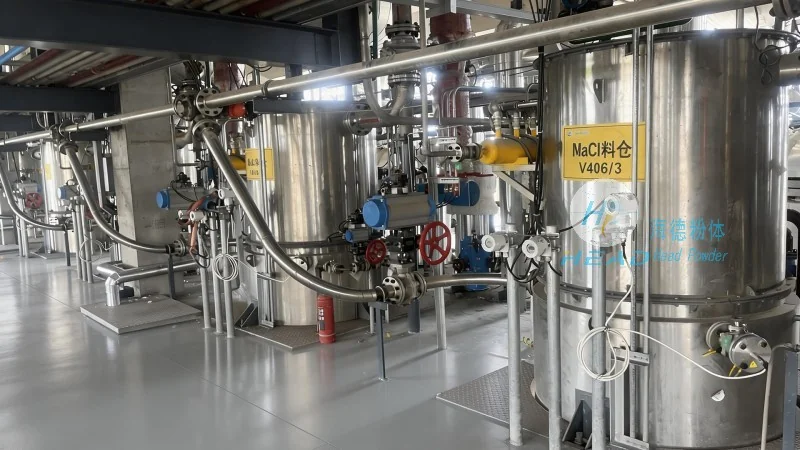
Key Components of the System
The system typically consists of several critical components that work in tandem to ensure smooth and efficient operation. These include a hopper or feeder to store and feed the fertilizer granules, a blower or compressor to generate the air pressure, a pipeline network to carry the material and air mixture, and a receiver or discharge hopper at the destination. Additionally, the system may incorporate features such as rotary valves, filters, and pressure regulators to maintain consistent flow and prevent blockages or air leaks.
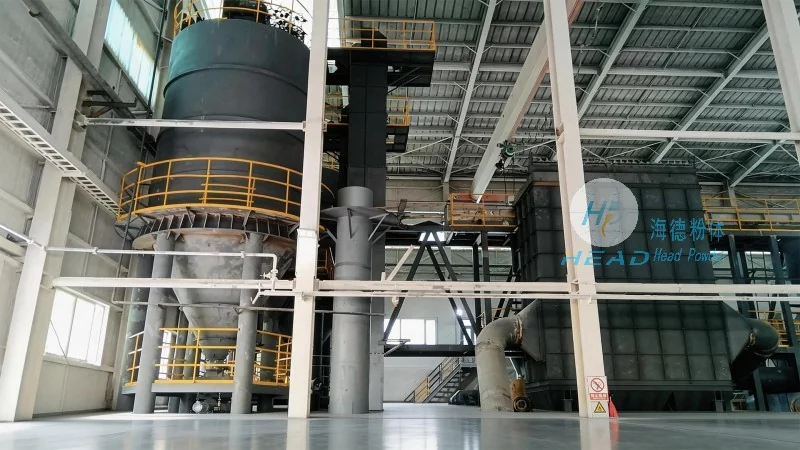
Design Principles and Operational Mechanisms
The design of a fertilizer granule pneumatic conveying system is based on fundamental principles of fluid dynamics and material handling. The primary mechanism involves creating a high-pressure air stream within the pipeline, which lifts and propels the fertilizer granules through the system. The velocity of the air and the size of the granules are carefully matched to ensure that the material is conveyed without excessive wear or breakage. The system may operate in either positive or negative pressure modes, depending on the specific application and the distance between the source and destination. Positive pressure systems are often used for short-distance conveying, while negative pressure systems are preferred for longer distances or when the material needs to be transported from a higher to a lower elevation.
Advantages of Using Pneumatic Conveying for Fertilizer Granules
Implementing a pneumatic conveying system for fertilizer granules offers several advantages over traditional methods like belt conveyors or bucket elevators. These benefits include reduced labor costs due to automated operation, improved material handling efficiency, and lower risk of product contamination or degradation. The system also allows for better control over the flow rate and pressure, enabling precise delivery of the fertilizer to storage or application areas. Furthermore, pneumatic conveying can handle a wide range of granule sizes and densities, making it versatile for various fertilizer products.
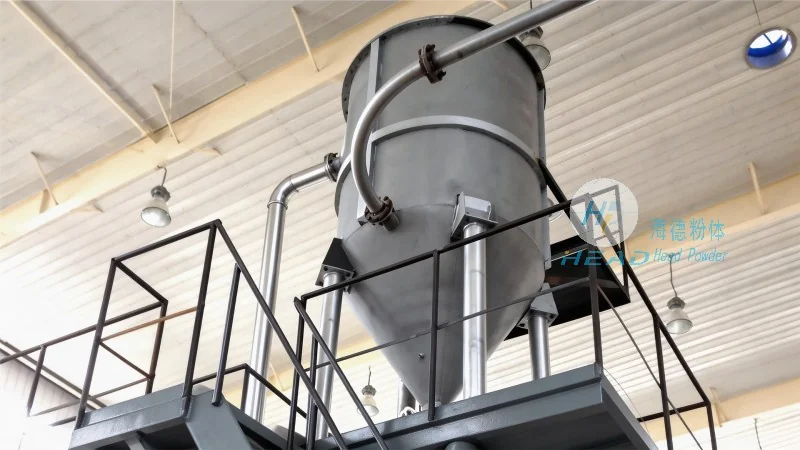
About HeadPowder: A Leading Provider of Conveying Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in China that specializes in the design, manufacturing, and installation of advanced material handling systems, including fertilizer granule pneumatic conveying equipment. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner in the agricultural and chemical industries, providing customized solutions tailored to the specific needs of their clients. The company's headquarters is located in Shandong, China, where they leverage their expertise and state-of-the-art facilities to deliver reliable and efficient conveying systems that meet the highest industry standards.