

Pneumatic Conveying Solutions for Soy Protein Powder
HeadPowder, a leading engineering firm based in Shandong, China, specializes in providing advanced pneumatic conveying solutions tailored for soy protein powder applications. This article outlines the key considerations and technical aspects of implementing efficient and reliable pneumatic conveying systems for handling soy protein powder, a critical component in various food and industrial processes.
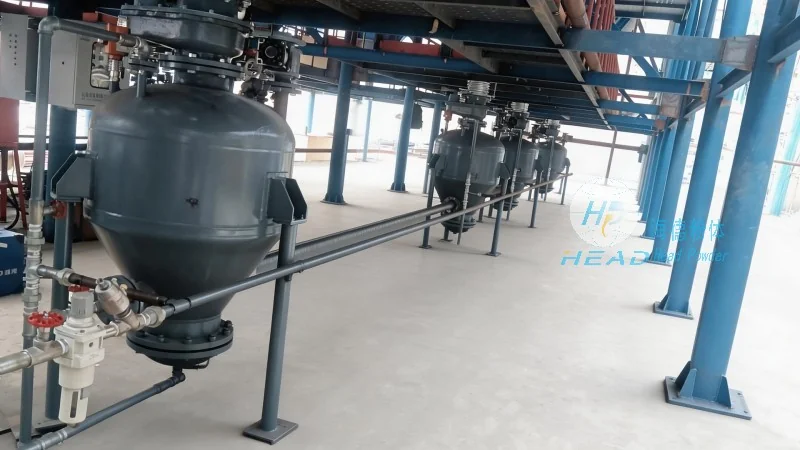
Understanding Pneumatic Conveying Technology
Pneumatic conveying is a method of transporting bulk materials, such as soy protein powder, through a pipeline using air or gas as the conveying medium. Unlike mechanical systems that rely on belts, screws, or buckets, pneumatic systems offer several advantages, including reduced product contamination, lower maintenance requirements, and the ability to handle materials with high moisture content or sensitive characteristics. For soy protein powder, which is often used in food products requiring strict quality control, these benefits are particularly valuable.
Key Factors in Designing a Soy Protein Powder Pneumatic Conveying System
When designing a pneumatic conveying system for soy protein powder, several critical factors must be considered to ensure optimal performance and product integrity. These include the material's flow properties, particle size distribution, moisture content, and the required conveying distance and capacity. The system design must also account for the need to minimize product degradation, prevent clogging, and maintain consistent air pressure and flow rates. HeadPowder engineers utilize advanced computational fluid dynamics (CFD) and material testing to analyze these factors and develop customized solutions that meet specific operational requirements.
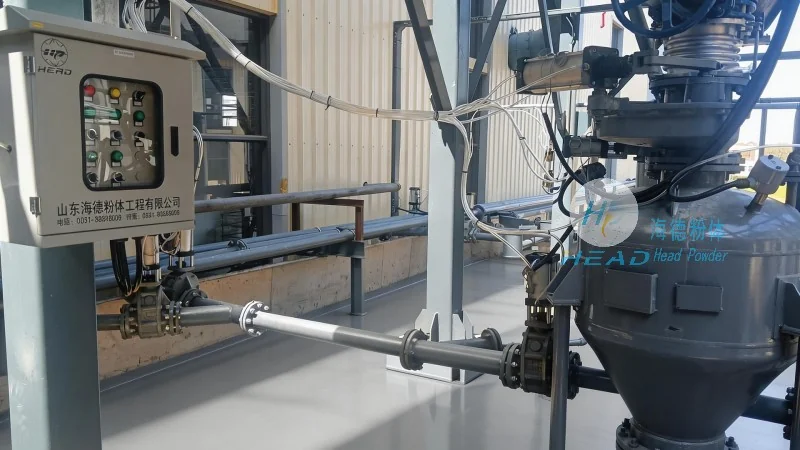
Components of a Typical Soy Protein Powder Pneumatic Conveying System
A standard pneumatic conveying system for soy protein powder typically consists of several key components. The primary elements include a hopper or storage silo to hold the powder, a rotary valve or feeder to control the material flow, a conveying pipeline, a venturi or airlock device to create the necessary pressure differential, and a receiver or discharge hopper at the destination. The air compressor or blower provides the motive force, generating the airflow that propels the powder through the system. Each component is selected based on the specific characteristics of the soy protein powder and the operational conditions, ensuring efficient and reliable transport.
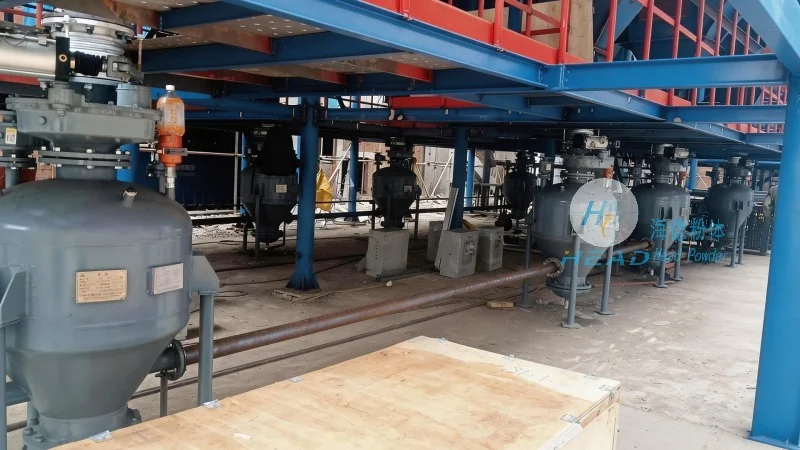
Advantages of Pneumatic Conveying for Soy Protein Powder
Implementing a pneumatic conveying system for soy protein powder offers numerous advantages over traditional mechanical conveying methods. One of the most significant benefits is the reduction in product contamination, as the system operates in a closed environment, preventing exposure to dust, moisture, or other contaminants. This is crucial for soy protein powder, which is often used in food applications where purity and quality are paramount. Additionally, pneumatic systems are more energy-efficient and require less space compared to mechanical conveyors, making them ideal for facilities with limited floor space or those seeking to optimize operational costs. The ability to handle varying material flow rates and distances also enhances flexibility, allowing for seamless integration into existing production lines.
Customization and Integration Services by HeadPowder
HeadPowder, with its headquarters in Shandong, China, offers comprehensive customization and integration services for pneumatic conveying systems tailored to soy protein powder applications. The company's team of experienced engineers works closely with clients to understand their specific needs, from initial system design and material testing to installation and commissioning. HeadPowder's solutions are designed to meet the highest standards of efficiency, reliability, and product integrity, ensuring that soy protein powder is transported safely and effectively. The company's commitment to quality and customer satisfaction has made it a trusted partner for businesses in the food and industrial sectors seeking advanced material handling solutions.