

Principle and Working Scene Characteristics of Coke Material Conveying Systems
HeadPowder Engineering, a leading provider of industrial material handling solutions, specializes in the design, manufacturing, and implementation of coke material conveying systems. Headquartered in Shandong, China, the company leverages its local expertise and advanced technology to deliver high-quality solutions tailored to the needs of industrial clients. These systems are crucial for the efficient transportation of coke, a vital raw material in steel production and other industrial applications. Understanding the principle and working scene characteristics of such systems is essential for optimizing industrial operations and ensuring safety and efficiency in material handling processes.
Principle of Coke Material Conveying Systems
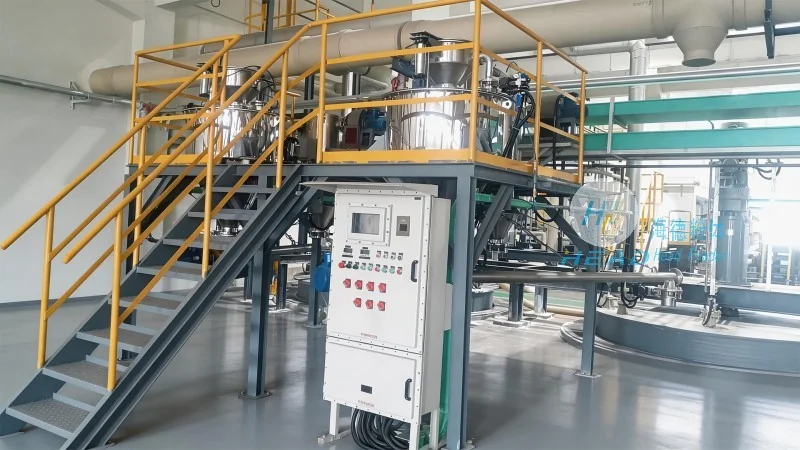
Coke material conveying systems operate on the fundamental principle of mechanical transport, utilizing various equipment to move coke from its source to its destination. The core components typically include feeders, conveyors (such as belt conveyors, screw conveyors, or pneumatic conveyors), and control systems. The system's design is tailored to the specific characteristics of coke, including its bulk density, particle size, and flowability. For instance, belt conveyors are commonly used for horizontal or slightly inclined transport due to their high load capacity and ability to handle large volumes of coke. Screw conveyors are suitable for vertical or inclined transport, providing a compact solution for space-constrained environments. Pneumatic conveyors, on the other hand, use air pressure to transport coke, which is ideal for applications requiring dust control and minimal maintenance.
Working Scene Characteristics of Coke Material Conveying Systems
The working scene characteristics of coke material conveying systems vary significantly based on the industrial environment and the specific application. In steel plants, for example, these systems are often integrated into larger production lines, handling large quantities of coke from storage silos to blast furnaces or other processing units. The systems must be capable of withstanding high temperatures and abrasive conditions, as coke is a hard, porous material that can cause wear on equipment components. Additionally, the systems need to ensure minimal material loss and dust generation to maintain environmental standards and operational safety.
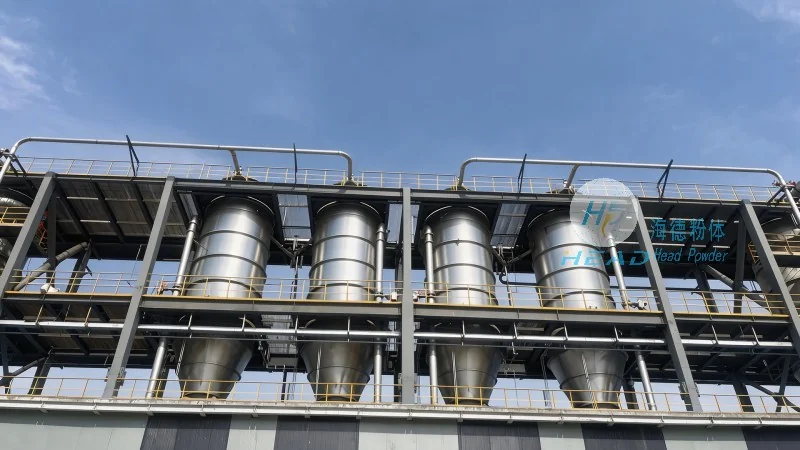
In other industrial settings, such as coke production facilities or recycling plants, the conveying systems may be used to transport coke from processing units to storage areas or for further treatment. The working scene may involve more complex material handling requirements, including the need for multiple conveyors in series or parallel configurations to achieve the desired transport efficiency. The systems must also be designed to accommodate variations in coke quality and moisture content, which can affect its flow characteristics and the overall performance of the conveying equipment.
Key Features and Advantages of HeadPowder's Coke Conveying Solutions
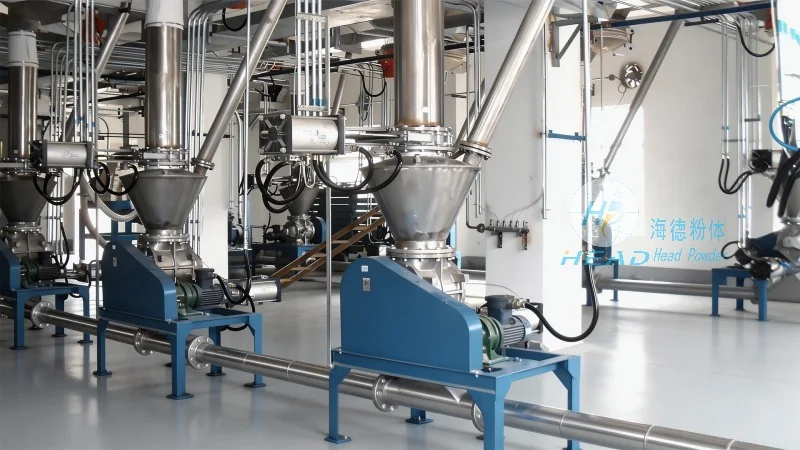
HeadPowder Engineering offers advanced coke material conveying systems that are engineered to meet the demanding requirements of modern industrial operations. The company's solutions are characterized by high reliability, low maintenance costs, and energy efficiency. For example, their belt conveyor systems utilize heavy-duty belts and robust frame structures to ensure long service life and minimal downtime. The screw conveyors are equipped with wear-resistant materials, such as stainless steel or special alloys, to withstand the abrasive nature of coke and reduce the frequency of component replacement. Pneumatic conveyors are designed with efficient air filtration systems to minimize dust emissions and comply with environmental regulations.
Another key advantage of HeadPowder's systems is their adaptability to different working environments. Whether it's a high-temperature steel plant or a cooler, ambient environment, the company's engineers can customize the system to suit specific operational needs. This includes adjusting the conveyor speed, capacity, and layout to optimize material flow and reduce bottlenecks. The control systems are also integrated with advanced monitoring and diagnostic tools, allowing operators to track system performance in real-time and identify potential issues before they lead to equipment failure.
Application Examples and Operational Efficiency
The effectiveness of coke material conveying systems is demonstrated through their application in various industrial scenarios. In a typical steel production facility, the system may start with a bulk storage silo, where coke is stored in large quantities. From there, a belt conveyor transports the coke to a transfer point, where it is then moved to a screw conveyor for vertical transport to the blast furnace. The system's efficiency is measured by its ability to maintain a consistent flow rate, minimize material spillage, and ensure that the coke reaches its destination without degradation. HeadPowder's systems have been proven to enhance operational efficiency by reducing the time required for material transport and minimizing the need for manual handling, which improves safety and reduces labor costs.
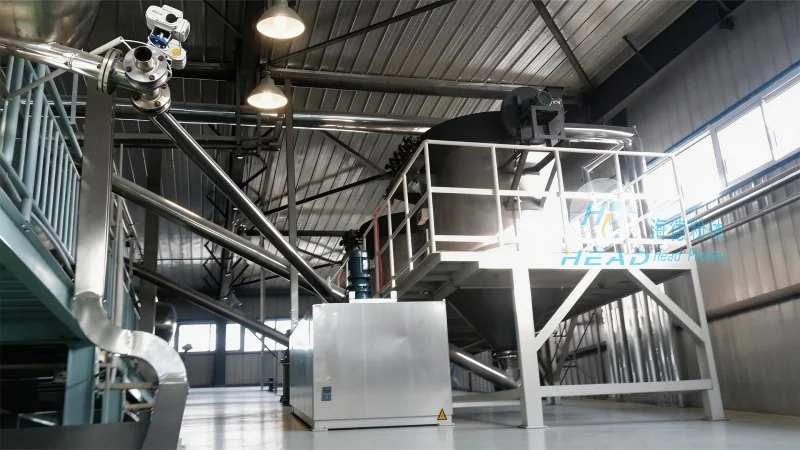
In recycling plants, the conveying systems may be used to transport coke from sorting and processing units to storage or for further treatment. The systems are designed to handle mixed materials and varying particle sizes, ensuring that the coke is separated and transported efficiently. The working scene in such environments may involve more frequent start-stop cycles and variable load conditions, which the systems are engineered to handle without compromising performance. The integration of HeadPowder's conveying systems with other processing equipment, such as crushers or screens, allows for a seamless material flow, enhancing overall plant productivity.
Conclusion and Future Trends
Coke material conveying systems are critical components of modern industrial operations, and their design and implementation require careful consideration of both the material characteristics and the operational environment. HeadPowder Engineering, with its expertise in industrial material handling, provides comprehensive solutions that address the unique challenges of coke transportation. By focusing on reliability, efficiency, and adaptability, the company's systems contribute to improved operational performance and reduced costs for its clients. As industrial demands continue to evolve, the future of coke conveying systems will likely involve more advanced technologies, such as automated control systems and predictive maintenance, to further enhance efficiency and sustainability in material handling processes.