

Principles and Working Scene Characteristics of Brown Sugar Material Handling Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling systems tailored for the brown sugar industry. This article delves into the core principles and operational characteristics of such systems, providing insights into their functionality and practical applications within the brown sugar production process.
Core Principles of Brown Sugar Material Handling Systems
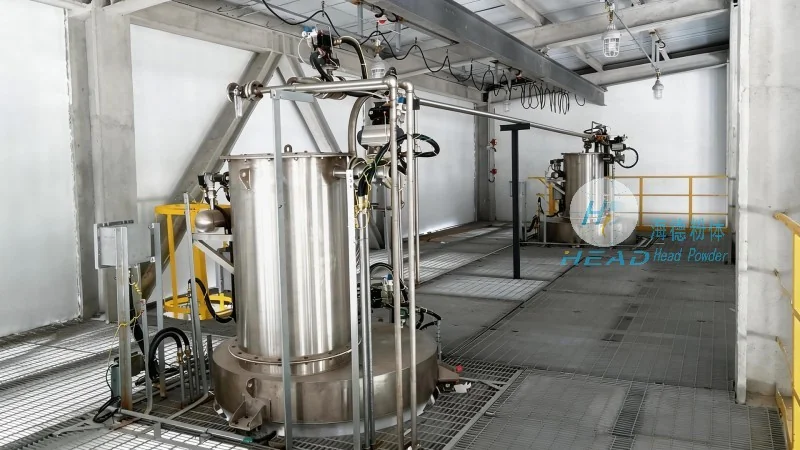
The fundamental principle of brown sugar material handling systems lies in the efficient and reliable transport of raw materials and finished products throughout the production line. These systems typically integrate mechanical components such as conveyor belts, bucket elevators, and pneumatic conveyors, which work in tandem to move bulk materials like sugar cane, molasses, or processed brown sugar. The design emphasizes durability, as the equipment must withstand the abrasive nature of sugar-related materials and the high operational demands of continuous production. Additionally, the systems are engineered for scalability, allowing manufacturers to adapt the infrastructure as production volumes increase or process requirements evolve.
Working Scene Characteristics and Application Scenarios
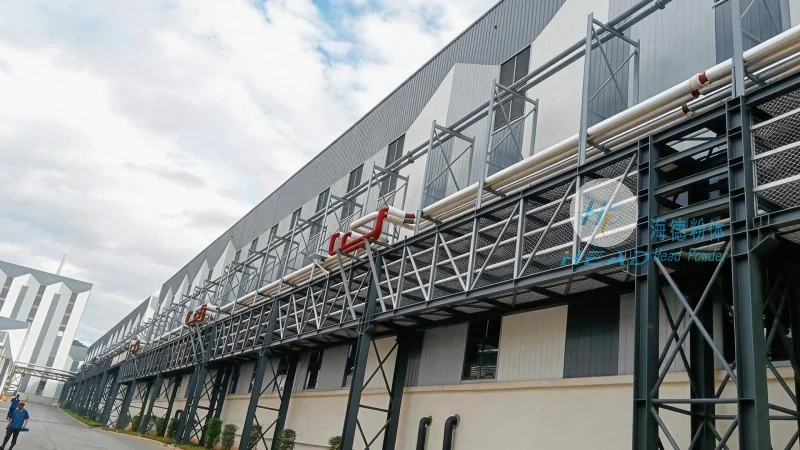
Brown sugar material handling systems are deployed across diverse operational stages within a sugar processing facility. In the initial stages, these systems facilitate the transport of raw sugar cane or harvested sugar beets from storage areas to processing units. This often involves heavy-duty belt conveyors capable of handling large volumes of bulk material, ensuring a smooth transition from raw input to processed state. As the production progresses to the refining and crystallization phases, specialized equipment like screw conveyors or pneumatic systems are employed to move molasses, crystals, and intermediate products between processing tanks and storage silos. The working environment in these scenes is characterized by high humidity, temperature fluctuations, and the presence of sticky or granular substances, which demands robust materials and precise engineering to maintain system efficiency and longevity.
Key Features and Operational Advantages
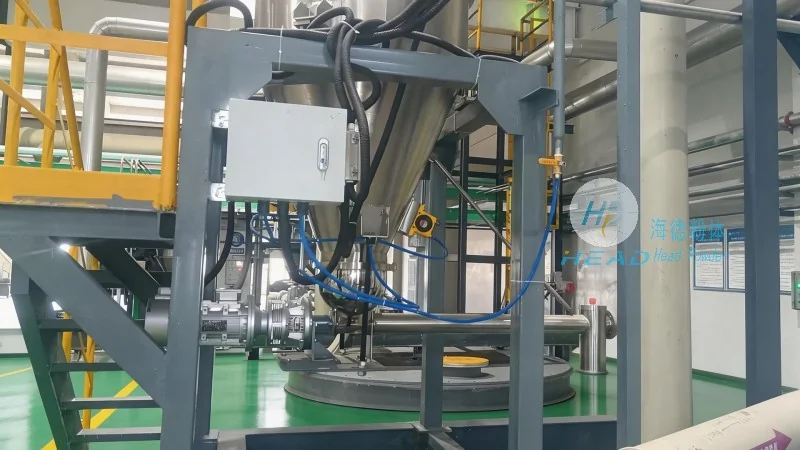
HeadPowder's brown sugar material handling systems are distinguished by several key features that enhance performance and reliability. For instance, the use of stainless steel or corrosion-resistant materials in conveyor components prevents contamination and extends service life in environments where moisture and sugar residues are prevalent. The systems also incorporate advanced control mechanisms, allowing for real-time monitoring of operational parameters such as speed, load, and temperature. This enables operators to optimize performance, reduce downtime, and ensure consistent product quality. Furthermore, the modular design of these systems allows for easy integration with existing production lines, minimizing installation time and disruption to ongoing operations.
Maintenance and Operational Considerations
Proper maintenance is crucial for the longevity and efficiency of brown sugar material handling systems. Regular inspections of conveyor belts, bucket elevators, and pneumatic components are essential to detect wear and tear early, preventing costly breakdowns. HeadPowder recommends routine cleaning of equipment to remove sugar residues, which can otherwise lead to clogging or reduced performance. Additionally, the systems are designed with accessible components, facilitating quick repairs and minimizing downtime. By adhering to these maintenance practices, manufacturers can ensure that their material handling infrastructure operates at peak efficiency, supporting consistent production output and maintaining product quality standards.
Conclusion
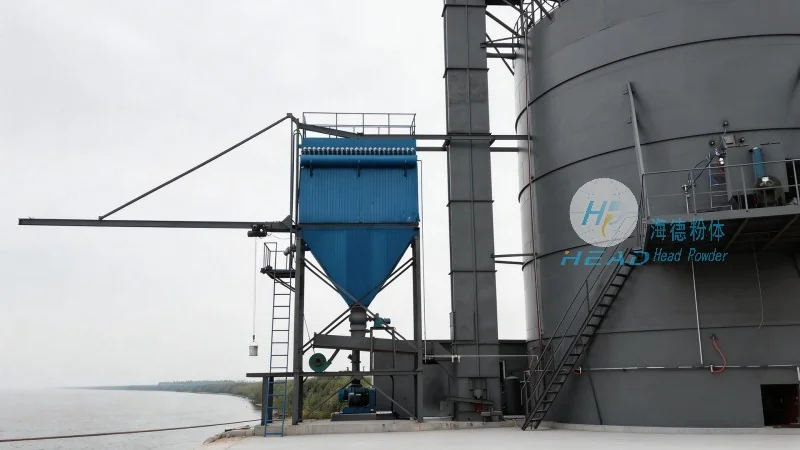
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides comprehensive solutions for brown sugar material handling systems, combining advanced engineering with practical application expertise. The principles and working scene characteristics outlined above highlight the importance of specialized equipment in optimizing the brown sugar production process. By investing in reliable material handling systems, sugar manufacturers can enhance operational efficiency, reduce costs, and ensure consistent product quality, ultimately contributing to their competitive advantage in the market.